Filter by:
Milling Cutters for Machining Hardened Steel
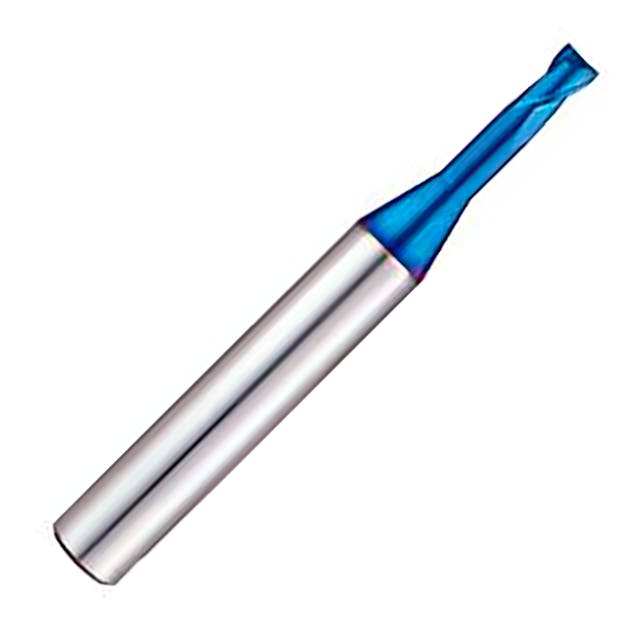
Pulsar Blue 2 Flute Rib Processing Slot Drill for Hardened Steel
Series: 100450
Pulsar Blue 2 Flute Rib Processing Slot Drill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
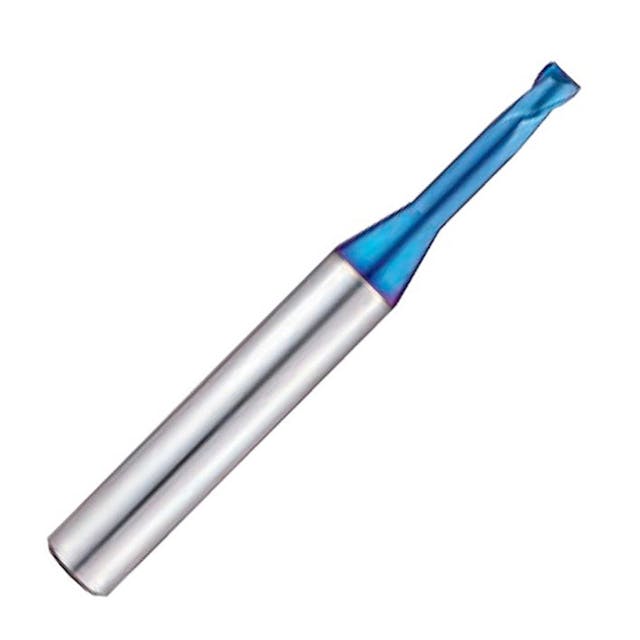
Pulsar Blue 2 Flute Corner Radius Rib Processing Slot Drill for Hardened Steel
Series: 101850
Pulsar Blue 2 Flute Rib Processing Corner Radius Slot Drill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Corner radius
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
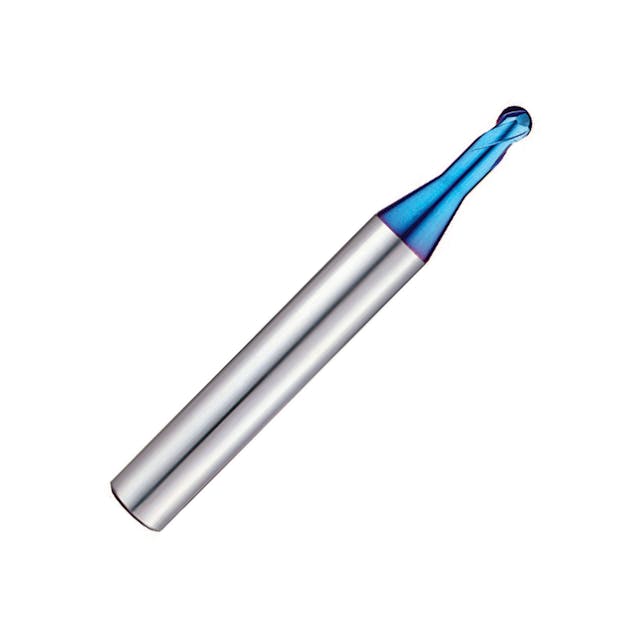
Pulsar Blue 2 Flute Rib Processing Ball Nose Micro End Mill for Hardened Steel
Series: 106350
Pulsar Blue 2 Flute Rib Processing Ball Nosed Slot Drill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
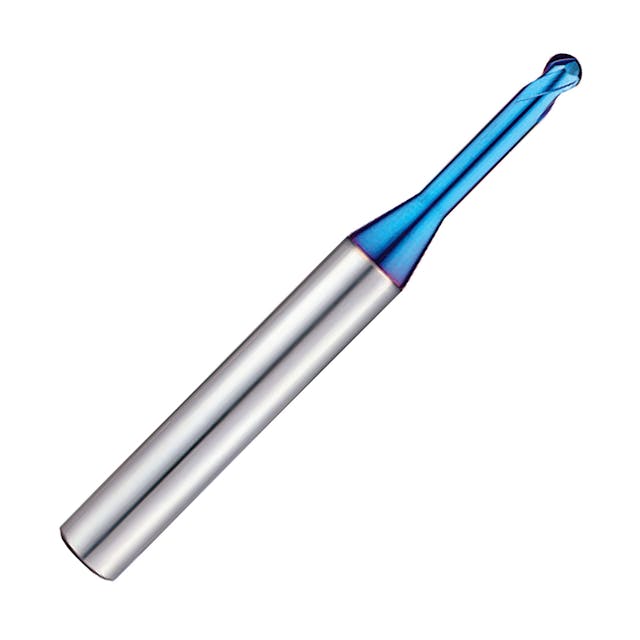
Pulsar Blue 2 Flute Rib Processing Ball Nose Slot Drill for Hardened Steel
Series: 109350
Pulsar Blue 2 Flute Rib Processing Ball Nose Slot Drill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
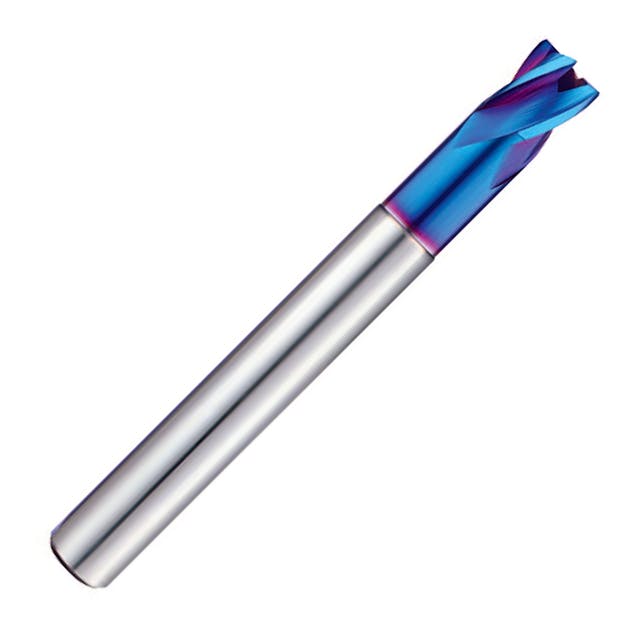
Pulsar Blue 4 Flute Extended Neck End Mill for Hardened Steel
Series: 101550
Pulsar Blue 4 Flute Extended Neck End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
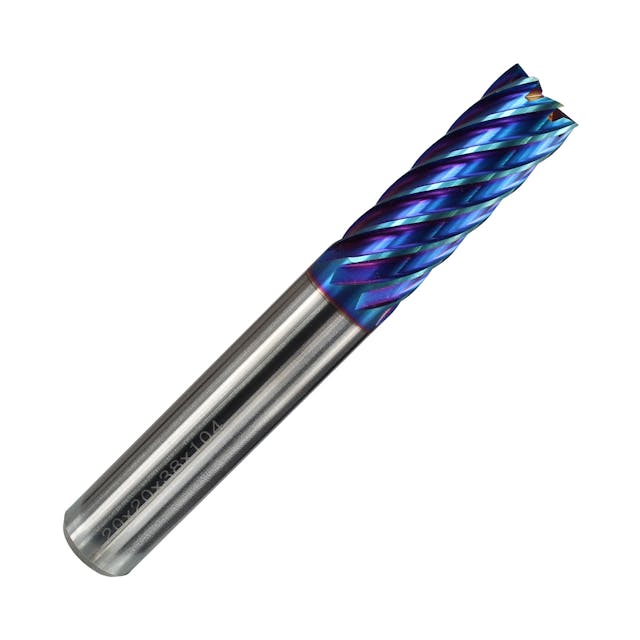
Pulsar Blue 6 & 8 Flute 45 Degree Helix Long Series End Mill for Hardened Steel
Series: 102950
Pulsar Blue 6 & 8 Flute Long End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 45 degree helix
- Excellent workpiece finish
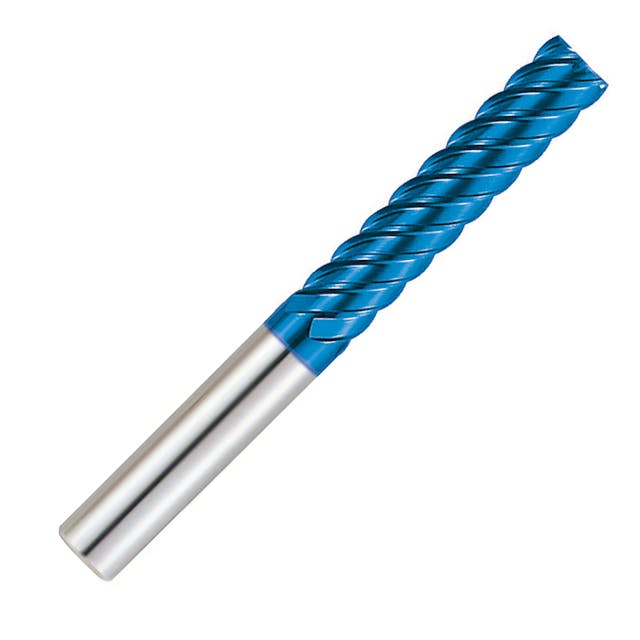
Pulsar Blue 6 & 8 Flute 45 Degree Helix Extra Long Series End Mill for Hardened Steel
Series: 103950
Pulsar Blue 6 & 8 Flute Extra Long End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 45 degree helix
- Excellent workpiece finish
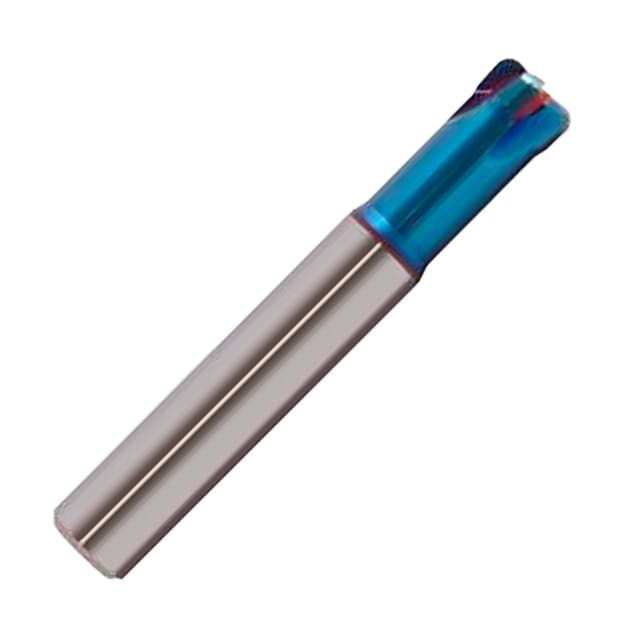
Pulsar Blue 4 Flute High Feed Corner Radius End Mill for Hardened Steel
Series: 110350
Pulsar Blue 4 Flute High Feed Corner Radius End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- Corner radius
- High speed cutting
- High feed geometry
- Short flute for maximum strength
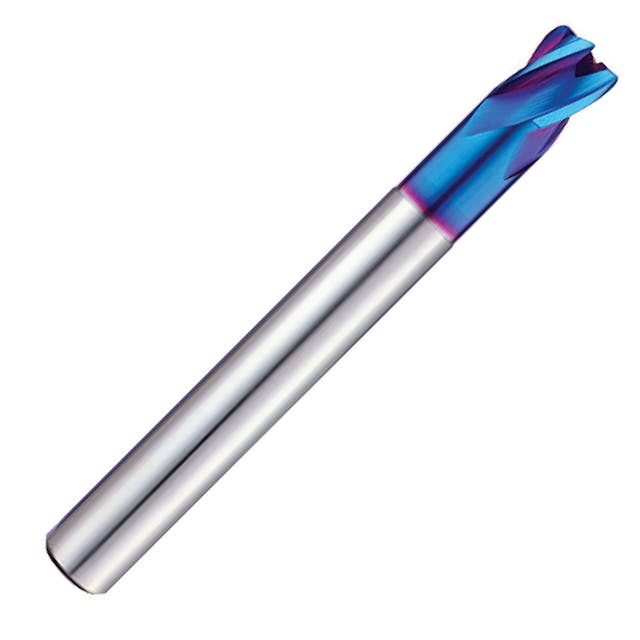
Pulsar Blue 4 Flute Extended Neck Corner Radius Stub Length End Mill for Hardened Steel
Series: 103350
Pulsar Blue 4 Flute Extended Neck Corner Radius Stub Length End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Corner radius
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
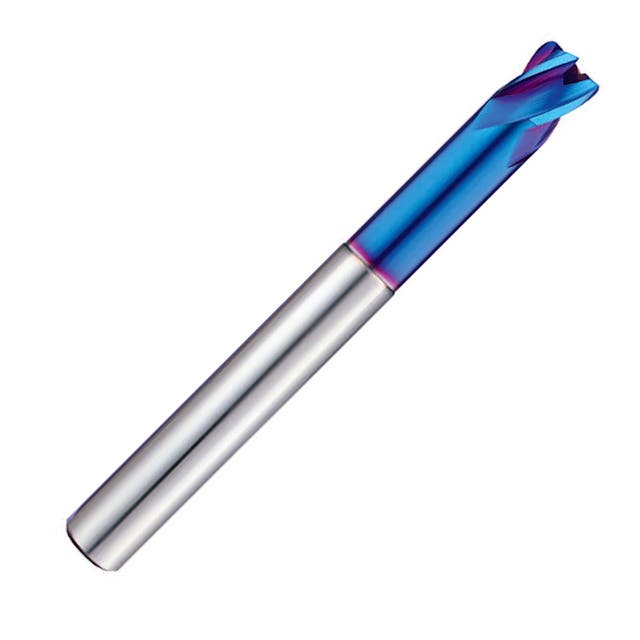
Pulsar Blue 4 Flute Extended Neck Corner Radius Long Length End Mill for Hardened Steel
Series: 101750
Pulsar Blue 4 Flute Extended Neck Corner Radius Long Length End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Corner radius
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
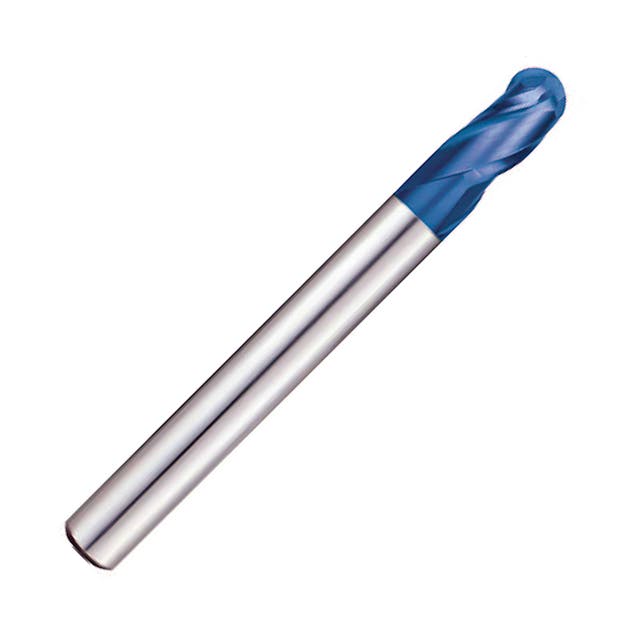
Pulsar Blue 3 Flute Ball Nose End Mill for Hardened Steel
Series: 107350
Pulsar Blue 3 Flute Ball Nose End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
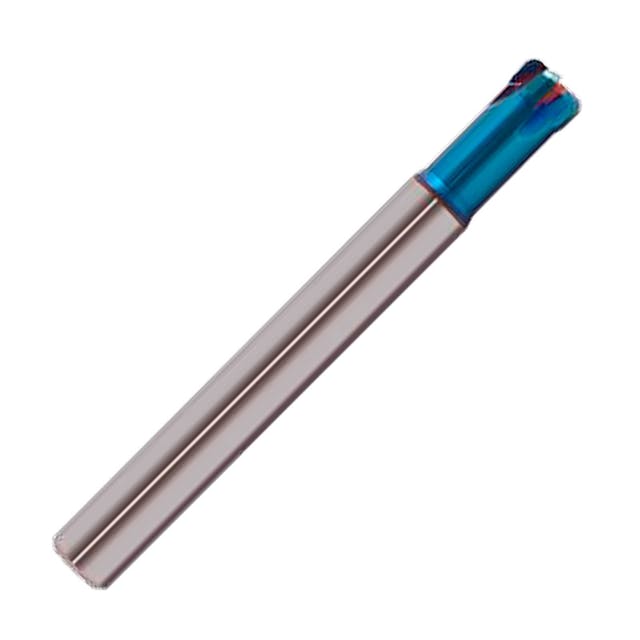
Pulsar Blue High Feed Long Length Corner Radius End Mill for Hardened Steel
Series: 111350
Pulsar Blue 4 Flute High Feed Long Length Corner Radius End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- Corner radius
- High speed cutting
- High feed geometry
- Short flute for maximum strength
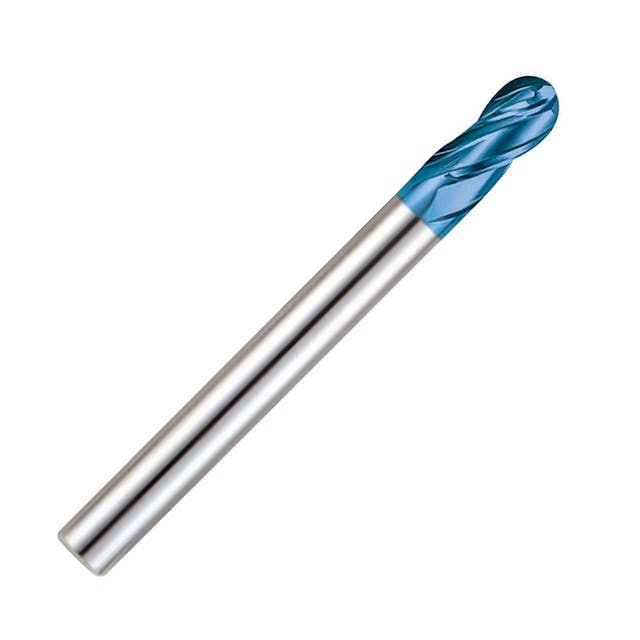
Pulsar Blue 4 Flute Ball Nose End Mill for Hardened Steel
Series: 101950
Pulsar Blue 4 Flute Ball Nose End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
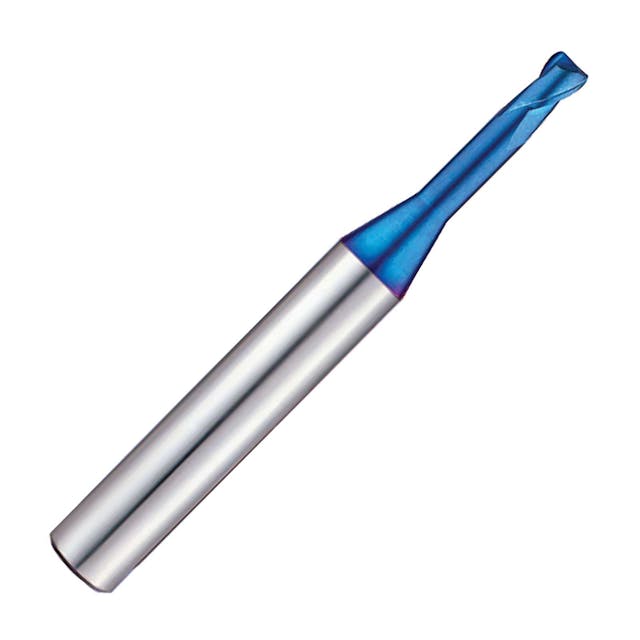
Pulsar Blue 2 Flute Corner Radius Rib Processing End Mill for Hardened Steel
Series: 102350
Pulsar Blue 2 Flute Rib Processing Corner Radius Slot Drill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Corner radius
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
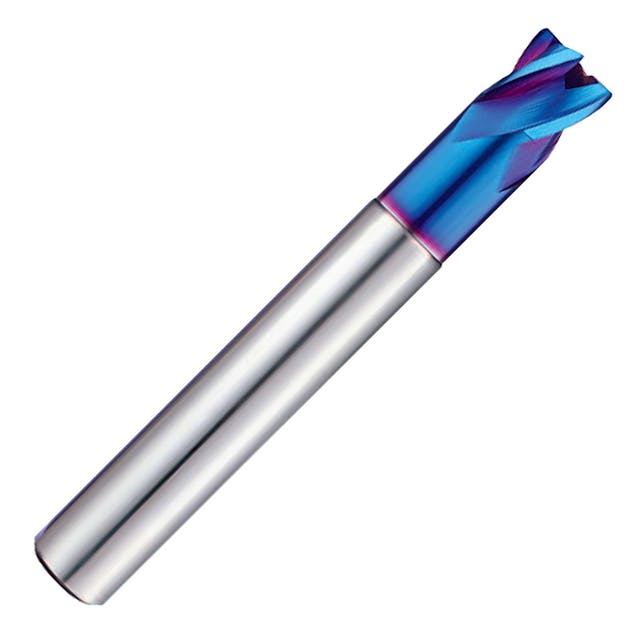
Pulsar Blue 4 Flute Corner Radius Extended Neck End Mill for Hardened Steel
Series: 101650
Pulsar Blue 4 Flute Extended Neck Corner Radius End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Corner radius
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
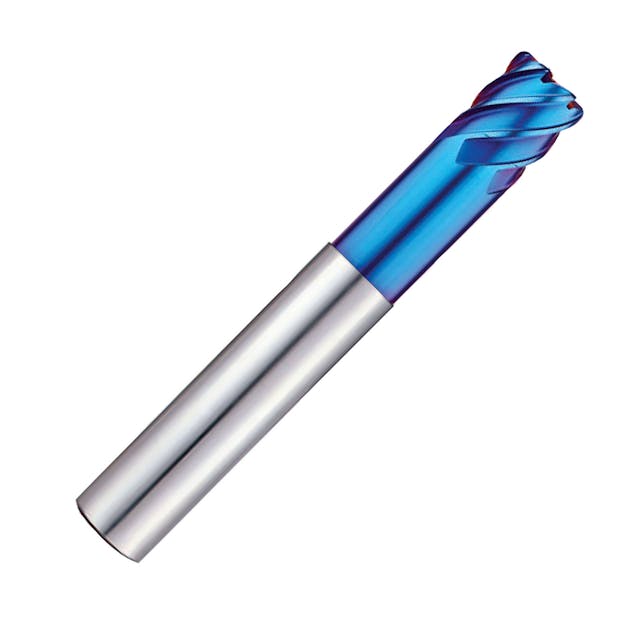
Pulsar Blue 6 Flute Helix Corner Radius End Mill for Hardened Steel
Series: 108350
Pulsar Blue 6 Flute Helix Corner Radius End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Corner radius
- Suitable for machining upto 70HRC
- High speed cutting
- 45 degree helix
- Excellent workpiece finish
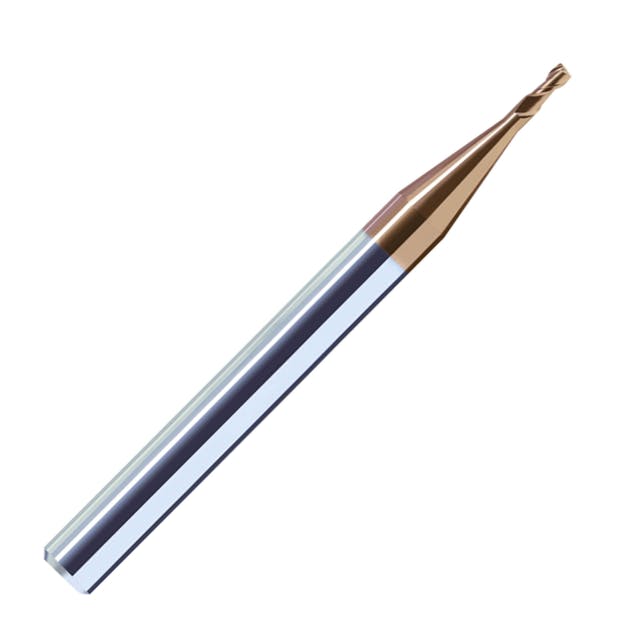
ZCC-CT HM-2E Series 2 Flute End Mill with Straight Shank for Hardened Steel Machining
Series: HM-2E
ZCC-CT HM-2E 2 Flute End Mill with Straight Shank
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
Starting From:
£17.49 excl. VAT
£20.99 incl. VAT
£17.49 excl. VAT
£20.99 incl. VAT
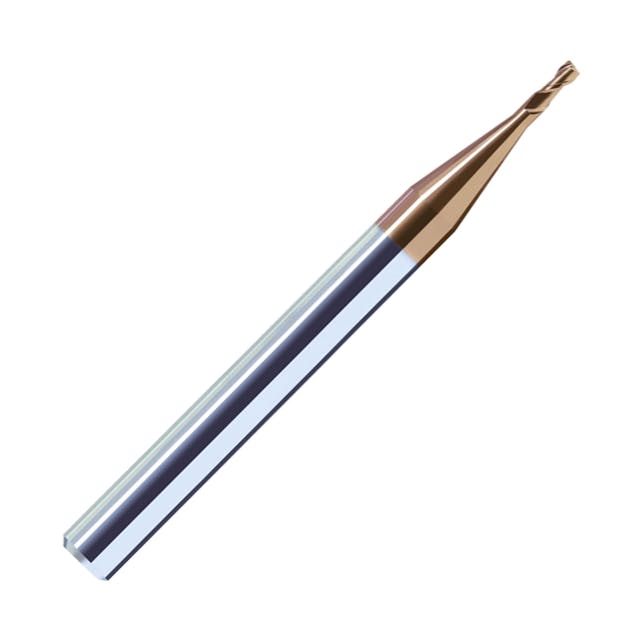
ZCC-CT HM-2ES Series 2 Flute Micro Diameter End Mill with Straight Shank for Hardened Steel Machining
Series: HM-2ES
ZCC-CT HM-2ES 2 Flute Micro Diameter End Mill with Straight Shank
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
- Starting at 0.3mm diameter
Starting From:
£12.31 excl. VAT
£14.77 incl. VAT
£12.31 excl. VAT
£14.77 incl. VAT
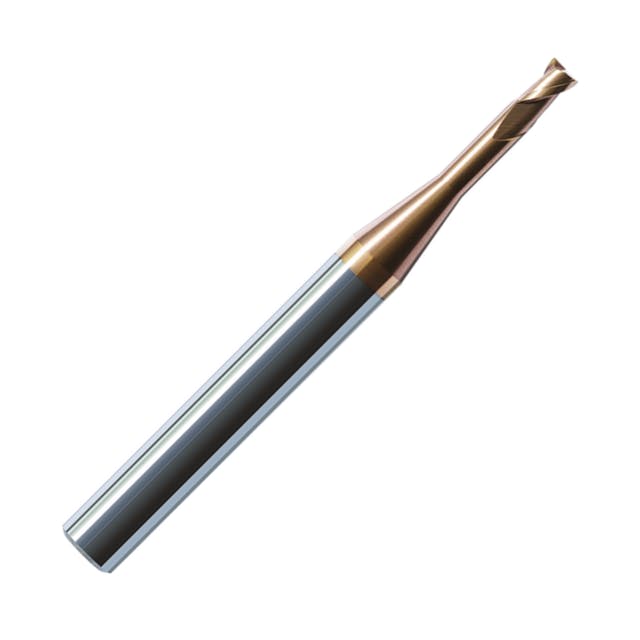
ZCC-CT HM-2EP 2 Flute Slot End Mill with Short Cutting Edge and Long Neck for Hardened Steel
Series: HM-2EP
ZCC-CT HM-2EP 2 Flute Slot End Mill with Short Cutting Edge and Long Neck
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
Starting From:
£19.74 excl. VAT
£23.69 incl. VAT
£19.74 excl. VAT
£23.69 incl. VAT
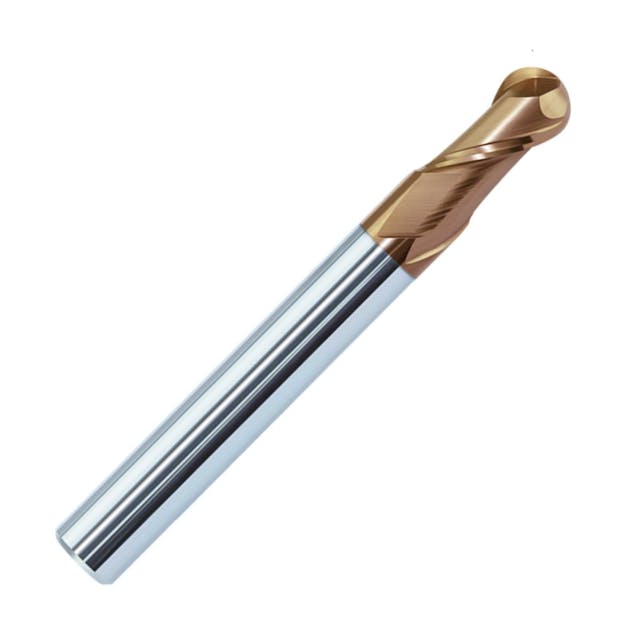
ZCC-CT HM-2B Series 2 Flute Ball Nose End Mill with Straight Shank for Hardened Steel Machining
Series: HM-2B
ZCC-CT HM-2B 2 Flute Ball Nose End Mill with Straight Shank
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
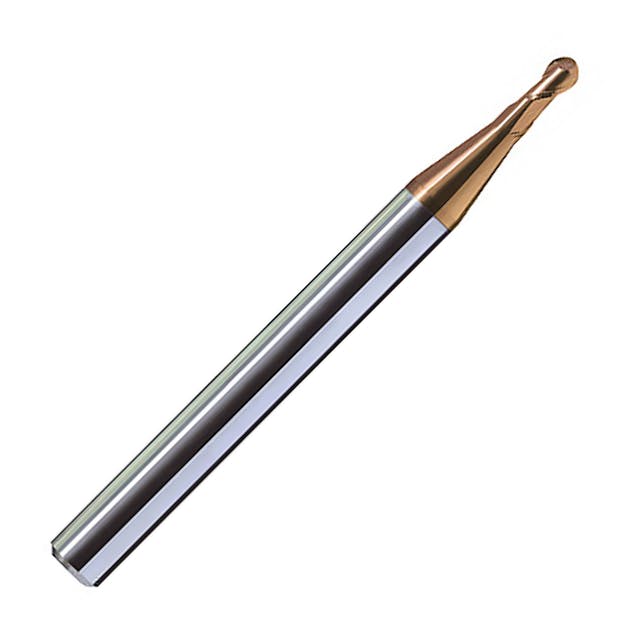
ZCC-CT HM Series 2 Flute Ball Nose Rib Processing Hardened Steel Milling Cutters
Series: HM-2BP
ZCC-CT HM-2BP 2 Flute Ball Nose Rib Processing Slot Drill
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
Starting From:
£21.79 excl. VAT
£26.15 incl. VAT
£21.79 excl. VAT
£26.15 incl. VAT
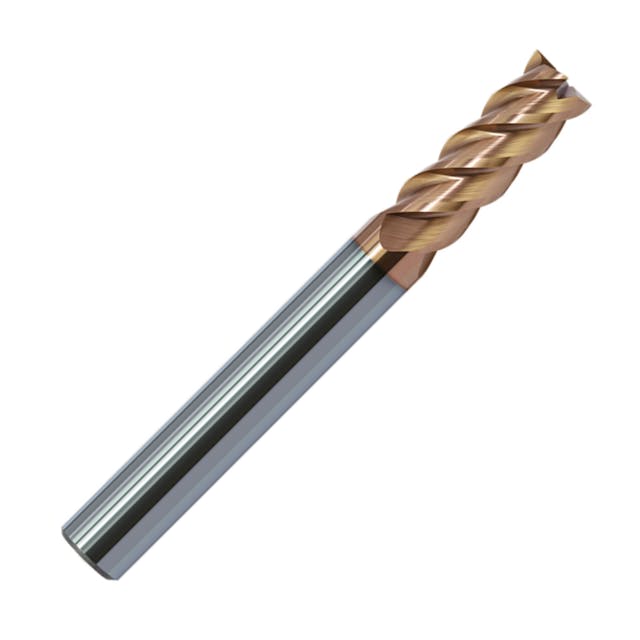
ZCC-CT HM-4E Series 4 Flute Hardened Steel Milling Cutters
Series: HM-4E
ZCC-CT HM-4E 4 Flute End Mill with Straight Shank For Hardened Steels
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
Starting From:
£14.53 excl. VAT
£17.44 incl. VAT
£14.53 excl. VAT
£17.44 incl. VAT
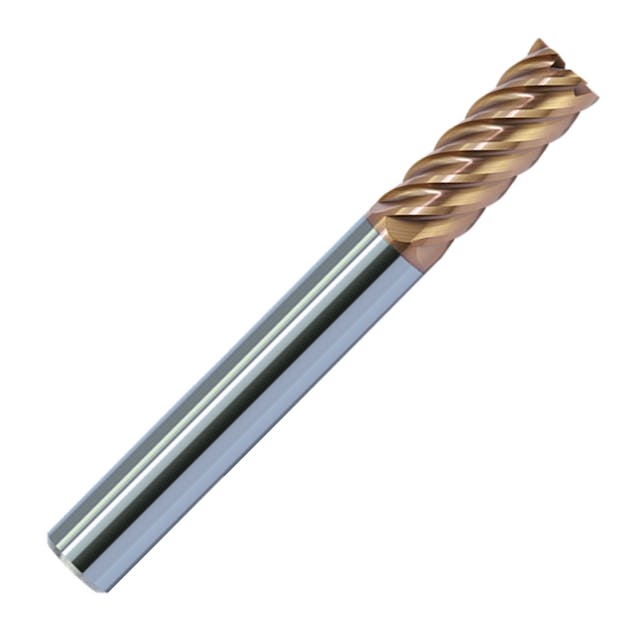
ZCC-CT HM-6E Series 6 Flute End Mill with Straight Shank for Hardened Steel Machining
Series: HM-6E
ZCC-CT HM-6E 6 Flute End Mill with Straight Shank
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
Starting From:
£26.10 excl. VAT
£31.32 incl. VAT
£26.10 excl. VAT
£31.32 incl. VAT
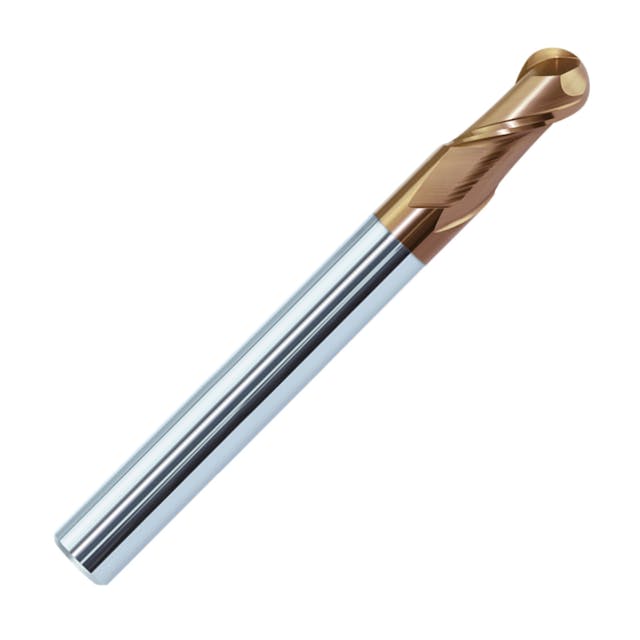
ZCC-CT HM-2BL Series 2 Flute Long Length Ball Nose Slot Drill for Hardened Steel Machining
Series: HM-2BL
ZCC-CT 2 Flute Long Length Ball Nose Slot Drill
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
Starting From:
£38.11 excl. VAT
£45.73 incl. VAT
£38.11 excl. VAT
£45.73 incl. VAT
Frequently Asked Questions
A hardened steel milling cutter is a solid carbide end mill specifically designed to machine steels that have been heat-treated to high hardness, typically above 45 HRC (Hardness Rockwell C) and up to 70 HRC. Standard milling cutters are designed for steels up to approximately 45 HRC; beyond that hardness, the cutting forces and temperatures exceed what general-purpose carbide and coatings can withstand, causing rapid edge wear, chipping and tool failure.
Hardened steel milling is used in tool and die making, mould making and precision component manufacturing where the workpiece is heat-treated to its final hardness before machining. This "hard machining" approach has replaced the older practice of machining soft (annealed) steel and then heat-treating the finished part, hard machining avoids the distortion that occurs during heat treatment, producing more accurate components. Typical hardened steel workpieces include stamping dies, injection moulds, forging dies, hardened shafts, gears, bearings and tool components made from tool steels such as D2, A2, O1, H13, S7 and M2 hardened to 50-65 HRC.
Our range contains over 2,000 products rated for hardened steel machining, all solid carbide, from three brands: ZCC-CT, Europa Tool and Nano-Mill.
Hardened steel cutters from the above brands are organised into sub-ranges:
HM Series (ZCC-CT, rated to 68 HRC)
Pulsar Blue (Europa Tool, rated to 70 HRC)
Max-Mill (Nano-Mill, rated to 55 HRC for lighter hard-machining applications).
The range covers three hardness tiers, each matching a different class of cutter:
Up to 55 HRC / Nano-Mill Max-Mill range: The entry tier cutter option for hard machining. TiAlN-coated micrograin carbide rated for steels up to 55 HRC. This covers medium-hardened steels through to hardened alloy steels, case-hardened components and tool steels tempered to moderate hardness. The Max-Mill range is suitable for steels, stainless steels, inconel and titanium and can be used wet or dry. At 55 HRC, the cutting forces are manageable with standard TiAlN coating and micrograin carbide and this tier is suitable for job shops that occasionally machine moderately hardened parts but do not specialise in hard machining.
Up to 68 HRC / ZCC-CT HM Series: The production hard-machining tier. KMG555 Nano-ALTiN coating on ultra-fine grain carbide, rated for steels up to 68 HRC. This covers fully hardened tool steels (D2 at 60–62 HRC, A2 at 57–59 HRC, H13 at 50-54 HRC, M2 at 62-65 HRC) and hardened bearing steels. The HM Series is the standard choice for mould and die making where the workpiece is hardened to its final operating hardness. The KMG555 coating is specifically formulated for "hard machining at high temperatures" and the nano-structured AlTiN coating provides the oxidation resistance and hot hardness needed to cut steel at 60+ HRC where cutting temperatures exceed 800°C.
Up to 70 HRC / Europa Tool Pulsar Blue: The premium tier for extreme hard machining. Premium nanograin carbide rated for steels up to 70 HRC. This covers the hardest tool steels and through-hardened components at the top of the hardness range — including D2 at maximum hardness (62 HRC), M2 at maximum hardness (65 HRC) and specialised wear-resistant steels. The Pulsar Blue range features "high speed cutting" capability and a 45° helix angle for efficient chip evacuation. The nanograin carbide substrate has a finer grain structure than micrograin carbide, providing higher hardness and edge sharpness for cutting the hardest steels. The range is "suitable for dry cutting", meaning that the coating and substrate can withstand the cutting temperatures of hard machining without coolant.
Our selection guidance:
For steels up to 55 HRC go for Max-Mill (TiAlN, most economical)
For steels 55-68 HRC use the HM Series (KMG555, production hard machining)
For steels up to 70 HRC it's Pulsar Blue (nanograin carbide, maximum hardness capability).
Always select a cutter rated above the workpiece hardness — a cutter rated to 55 HRC will fail rapidly on 60 HRC steel.
The two sub-ranges represent different approaches to hard machining, from different manufacturers:
HM Series (ZCC-CT): ZCC-CT is a Chinese carbide tooling manufacturer (part of the Zhuzhou Cemented Carbide Group). The HM Series uses "ultra fine grain carbide" with a KMG555 "Nano-ALTiN" coating. Key design features include: "Excellent tool design covers large chip pocket, good stability and machining efficiency" and "Optimised cutting geometry (Rake angle) assures edge stability and sharpness." The HM Series is rated to 68 HRC and is designed for production hard machining where tool life and consistency are critical. The series includes 17 sub-series (HM-2E, HM-2EP, HM-2FP, HM-4E, HM-4EL, HM-4EP, HM-4RP, HM-4RF, HM-4R, HM-6E, HM-6EL, HM-2B, HM-20P, HM-20S, HM-4B, HM-2BL, HM-4BL) covering 2-flute, 4-flute and 6-flute configurations in square, ball nose and corner radius profiles. The HM Series uses standard shank designations (HA = standard shank) and is available in diameters from 0.3mm to 20mm.
Pulsar Blue (Europa Tool): Europa Tool is a European precision tooling manufacturer. The Pulsar Blue range uses "premium nanograin carbide" which is a finer carbide grain structure than the HM Series ultra-fine grain, providing higher hardness and edge sharpness. Rated to 70 HRC (2 HRC higher than HM Series), the Pulsar Blue is designed for the hardest machining applications. Key features: "Suitable for dry cutting," "High speed cutting," and a 45° helix angle. The Pulsar Blue range covers 2, 3, 4, 6, and 8 flutes (more flute options than HM Series, which offers 2, 4, and 6) and includes square, ball nose and corner radius profiles. The Pulsar Blue is available in diameters from 0.1mm to 25mm and includes short, standard, and long length configurations. The additional 3-flute and 8-flute options provide specialised configurations for specific hard-machining applications.
Key differences: HM Series (68 HRC, ultra-fine grain carbide, KMG555 coating, 2/4/6 flutes, 0.3–20mm). Pulsar Blue (70 HRC, nanograin carbide, 2/3/4/6/8 flutes, 0.1–25mm, 45° helix, dry cutting, high-speed capable).
The Pulsar Blue has higher hardness capability, more flute options, a wider diameter range and is designed for dry high-speed cutting. The HM Series is the production workhorse for 55-68 HRC hard machining; the Pulsar Blue is the premium choice for 65-70 HRC and high-speed hard machining.
The range offers five flute configurations, each suited to different hard-machining operations:
2 Flute: Two cutting flutes provide the largest chip pocket space so the gullet between flutes is the largest of any configuration. This makes 2-flute cutters ideal for deep slotting and plunging operations where chip evacuation is critical. In hard machining, chips are hard and abrasive (if they are not evacuated quickly, they pack in the flute and destroy the cutting edge). The large chip pocket of a 2-flute cutter ensures chips clear the cutting zone. However, 2-flute cutters have only two cutting edges engaged, so the feed rate per tooth must be higher to achieve a given feed rate and the tool is less rigid than multi-flute cutters. The 2-flute is the most common configuration in our range, reflecting that slotting and plunging are common hard-machining operations. Available in all three sub-ranges.
3 Flute: A compromise between 2-flute chip space and 4-flute rigidity. The 3-flute configuration provides better surface finish than 2-flute (more cutting edges per revolution) while maintaining adequate chip space. Available exclusively in the Pulsar Blue range. The 3-flute is used for profiling and finishing operations in hard steel where surface finish matters and chip evacuation is manageable.
4 Flute: The standard general-purpose configuration for hard machining. Four flutes provide more cutting edges (higher feed rate capability, better surface finish) and greater tool rigidity than 2-flute. The 4-flute is used for profiling, facing and shoulder milling where chip evacuation is less critical than in slotting. The 4-flute is the standard choice for finishing passes on hardened steel where surface finish and dimensional accuracy are critical. Available in all three of our listed sub-ranges. The HM-4E, HM-4EL, HM-4EP, HM-4RP, HM-4RF series are 4-flute configurations.
6 Flute: Six flutes provide maximum rigidity and the highest number of cutting edges. The 6-flute is used for high-feed finishing operations where small chip loads per tooth are distributed across many edges, reducing the load on each edge and extending tool life in abrasive hardened steel. The 6-flute is particularly effective for profiling and finishing hardened steel at high cutting speeds. The HM-6E and HM-6EL series are 6-flute configurations. The 6-flute has smaller chip pockets than 4-flute, so it is not suitable for deep slotting, rather it is a profiling and finishing tool.
8 Flute: Eight flutes, this is the maximum in the range, available exclusively in the Pulsar Blue range. The 8-flute provides the highest edge count and maximum rigidity for high-speed finishing of hardened steel. Used for precision finishing operations where surface finish (low Ra) and dimensional accuracy are critical, such as mould and die finishing, precision component finishing. The 8-flute distributes the cutting load across many edges, allowing high feed rates while maintaining a small chip per tooth. Not suitable for roughing or slotting due to very small chip pockets.
Our selection guidance:
Slotting/plunging → 2-flute (maximum chip space)
General profiling → 4-flute (balance of chip space and edge count)
High-feed finishing → 6-flute (more edges, higher rigidity)
Precision finishing → 8-flute (maximum edges, best surface finish)
Compromise profiling/finishing → 3-flute.
The range offers three end mill profiles, each suited to different feature geometries:
Square: A flat-bottomed end mill with a 90° corner where the cutting face meets the cylindrical periphery. The square profile produces flat bottoms and sharp internal corners (90°). Used for slotting, facing, shoulder milling and pocketing where sharp internal corners are required. The square corner is the weakest point of the cutting edge and in hard machining, the sharp 90° corner is prone to chipping under high cutting forces. For this reason, square end mills in hardened steel are typically used with light cuts and are not recommended for heavy roughing. The square profile is available in 2, 4, 6 and 8-flute configurations across all three sub-ranges. The HM-2E, HM-4E, HM-6E series are square profile.
Ball Nose: A hemispherical tip, meaning that the end of the cutter is a full ball radius equal to half the cutter diameter. The ball nose is used for 3D contouring, profiling and sculpting complex surfaces (the defining application in mould and die making). The ball geometry allows the cutter to machine curved surfaces, draft angles and freeform shapes without leaving scallops or steps. In hard machining, the ball nose is critical for finishing hardened mould and die cavities to surface finishes as low as Ra 0.2-0.4 µm. The ball nose distributes cutting forces across the spherical surface, reducing the point-loading that causes corner chipping on square tools. The ball nose is available in 2, 3, 4 and 6-flute configurations. The HM-2B, HM-20P, HM-20S, HM-4B, HM-2BL, HM-4BL series are ball nose profiles.
Corner Radius: A flat-bottomed end mill with a radiused corner instead of a sharp 90° corner where the corner radius (typically 0.5mm to 3mm) blends the cutting face and periphery with a smooth arc. The corner radius eliminates the weak sharp corner of the square profile, significantly increasing edge strength and resistance to chipping in hard machining. The corner radius produces a fillet at the bottom of pockets and slots, which is actually desirable (a fillet reduces stress concentration in the workpiece, improving fatigue strength). The corner radius is the preferred profile for roughing and semi-finishing hardened steel where the cutting forces are high and corner chipping is a risk. The HM-4R, HM-4RP, HM-4RF series are corner radius profiles. The product code includes the radius value, e.g. HM4RPD80R05KMG555 has R=0.5 (0.5mm corner radius on an 8mm diameter cutter).
Our selection guidance:
3D contouring and mould/die finishing → ball nose
Slotting and sharp-corner pockets → square
Roughing, semi-finishing, and high-force operations → corner radius (stronger edge, no chipping).
For hardened steel, the corner radius is often preferred over square for general-purpose use because the radiused corner resists chipping.
The KMG555 coating is ZCC-CT's proprietary nano-structured AlTiN (Aluminium Titanium Nitride) coating which is specifically formulated for the HM Series of hardened steel milling cutters. In ZCC-CT's own words: "KMG555 Nano-ALTiN coating base for hard machining at high temperatures."
Coating Composition: AlTiN is a PVD (Physical Vapour Deposition) coating with a higher aluminium-to-titanium ratio than standard TiAlN. The high aluminium content is the key to its performance in hard machining (at cutting temperatures above 700°C, the aluminium in the coating oxidises to form a thin, stable layer of aluminium oxide (Al₂O₃) on the coating surface). This oxide layer acts as a thermal barrier preventing heat from transferring into the carbide substrate and maintaining the cutting edge hardness at elevated temperatures. Standard TiAlN coatings begin to oxidise and degrade above 800°C but the AlTiN formulation in KMG555 extends oxidation resistance to approximately 900-1000°C.
"Nano" Structure: The "Nano-ALTiN" designation indicates a nano-structured coating (the coating is deposited in a multilayer or nanocomposite structure where individual layers are measured in nanometres). This nanostructure produces a coating with higher hardness (typically 3300-3500 HV) and better toughness than conventional monolithic coatings. The nanostructure also reduces residual stress in the coating, preventing cracking and delamination under the cyclic thermal and mechanical loading of hard machining.
Why KMG555 Matters for Hard Machining: When machining hardened steel at 60+ HRC the cutting temperature at the edge can exceed 800°C. Without a coating that can withstand these temperatures the carbide substrate softens and the edge deforms and fails. The KMG555 coating maintains its hardness and protective oxide layer at these temperatures, allowing the cutter to operate at productive cutting speeds (55-125 m/min for 55-60 HRC steel, per the ZCC-CT cutting data) rather than the very low speeds that would be needed with an uncoated or inadequately coated tool.
The Pulsar Blue Alternative: The Europa Tool Pulsar Blue range uses a different coating system on its "premium nanograin carbide" substrate. While the specific coating designation is not published, the Pulsar Blue is rated to 70 HRC (2 HRC higher than the KMG555-coated HM Series) and is "suitable for dry cutting" which indicates a coating with even higher temperature resistance. The nanograin carbide substrate (finer grain than ultra-fine grain) also contributes to the higher hardness capability.
The range covers an exceptionally wide diameter range from 0.1mm to 25mm, making it suitable for everything from micro-machining to large mould and die work:
Micro Diameters (0.1mm-0.9mm): The Pulsar Blue range includes cutters from 0.1mm diameter, these are micro-machining tools used for engraving, fine detail work and micro-mould features. At 0.1mm (100 microns) the cutter is thinner than a human hair and requires extremely high spindle speeds (often 40,000+ RPM) and minimal depth of cut. The range includes: 0.1mm (16 products), 0.2mm (24), 0.3mm (32), 0.4mm (40), 0.5mm (56), 0.6mm (68), 0.8mm (60). The HM Series starts at 0.3mm. Micro-diameter cutters are predominantly 2-flute (for chip space) and ball nose (for 3D micro-contouring).
Small Diameters (1mm-3mm): Used for fine detail machining in moulds and dies such as engraving, small features, ribs and fine 3D contours. The range includes: 1mm, 1.2mm, 1.5mm, 2mm, 2.5mm & 3mm. These diameters are commonly used with 4-flute ball nose configurations for finishing small mould features.
Medium Diameters (3.5mm-8mm): The most commonly used range for general hard machining tasks such as profiling, slotting and finishing of hardened steel components. The range includes: 4mm, 5mm, 6mm & 8mm. These diameters are used with 4-flute and 6-flute configurations for profiling and finishing. The HM4RPD80R05KMG555 (8mm, 4-flute, corner radius) is a typical medium-diameter production tool.
Large Diameters (9mm-12mm): Used for heavier profiling and facing operations on larger hardened components. The range includes: 10mm, 12mm. These diameters are used with 4-flute and 6-flute configurations. The HM6ED100KMG555 (10mm, 6-flute) is a typical large-diameter tool.
Extra-large Diameters (14mm-25mm): Used for large mould and die work such as facing large hardened surfaces and profiling large cavities. The range includes: 14mm, 16mm, 18mm, 20mm, 25mm. These diameters are predominantly 6-flute and 8-flute (for rigidity and edge count on large cuts). The 25mm diameter is available only in the Pulsar Blue range.
Shank Diameter: Most cutters have a shank diameter equal to the cutting diameter ("necked" or "reduced neck" designs have a shank smaller than the cutting diameter). The range includes shank diameters from 3mm to 25mm. The most common shank sizes are 4mm, 6mm, 8mm, 10mm & 12mm, which match standard collet sizes.
Our range offers three length configurations, affecting the reach and rigidity of the cutter:
Standard Length: The default configuration where the flute length (cutting length) and overall length are standardised for each diameter, providing a balance of reach and rigidity. Standard length cutters are the most common because they provide adequate reach for most operations while maintaining maximum rigidity. The cutting length is typically 2-3x the diameter for standard-length tools. For example, the JB0154 has dimensions "1.5x4x3x50" — 1.5mm diameter, 4mm shank, 3mm cutting length, 50mm overall length. The JB1002 (10mm diameter) has "10×10×20×75" — 10mm diameter, 10mm shank, 20mm cutting length, 75mm overall length.
Long Length: Extended flute length and overall length for deep pocketing, deep slotting, and reaching into deep mould cavities. Long-length cutters provide greater reach but are less rigid — the longer the cutting section, the more it can deflect under cutting forces, causing chatter, poor surface finish, and potential tool breakage. Long-length cutters require reduced depths of cut and lower feed rates to manage deflection. In hard machining, deflection is particularly dangerous — a deflecting cutter in hardened steel will chip or break rapidly. Long-length cutters are used when the geometry of the workpiece demands reach (deep cavities, tall walls) and are operated with conservative parameters. The HM-4EL and HM-6EL series are long-length configurations.
Short Length: Reduced flute length and overall length for maximum rigidity. Short-length cutters are used for shallow operations where maximum rigidity is needed — light finishing passes, engraving, and operations where chatter is a problem. The short cutting section minimises deflection, allowing higher feed rates and better surface finish. Short-length cutters are the least common (36 products) because most hard-machining operations require at least standard reach. The Pulsar Blue range includes 48 short-length configurations.
Selection guidance: General profiling and finishing → standard length. Deep cavities and pockets → long length (with conservative parameters). Shallow finishing and chatter-sensitive operations → short length. The length choice should be the minimum that provides adequate reach — never use a long-length cutter when a standard will reach, as the extra length sacrifices rigidity.
The HM-4RP series is a "4 Flute Reduced Neck Corner Radius End Mill", a specialised geometry where the neck (the section between the cutting flutes and the shank) is reduced to a diameter smaller than both the cutting diameter and the shank diameter. This product example: HM4RPD80R05KMG555 has an 8mm cutting diameter, a standard (HA) shank & a reduced neck diameter that is smaller than 8mm.
Purpose of The Reduced Neck: The reduced neck provides clearance for deep profiling and shoulder milling operations where the cutter must reach past an obstacle (a wall, shoulder or clamp) to machine a surface below. Without a reduced neck the shank (same diameter as the cutter) would rub against the obstacle, preventing the cutter from reaching the machining surface. The reduced neck allows the cutter to pass beside the obstacle while the cutting flutes reach the surface below.
Reduced Neck vs Long Length: A reduced neck cutter is different from a long-length cutter. A long-length cutter has extended flutes (more cutting length) on a standard shank so it reaches deeper but the shank is full diameter. A reduced neck cutter has standard (or extended) flutes but a necked-down section behind the flutes so it reaches past obstacles. The reduced neck is used for "knuckle" or "undercut" geometries where the cutter must machine under a shoulder or overhang.
Trade Offs: The reduced neck is weaker than a full-diameter shank, the necked section has less cross-sectional area and is more prone to deflection and breakage. Reduced neck cutters require conservative depths of cut and feed rates. The corner radius on the HM-4RP (R0.5 on the 8mm example) provides edge strength at the cutting corner, partially compensating for the reduced neck rigidity.
When to Use a Reduced Neck:
When machining deep walls or shoulders where the shank would interfere with the workpiece
When plunge-finishing deep cavities in moulds and dies
When profiling past a clamp or fixture
When the workpiece geometry has undercuts or overhangs that a standard shank cannot clear.
For standard profiling without obstacles, a standard shank cutter is preferred for its greater rigidity.
The ZCC-CT HM Series cutting data (available as downloadable PDFs on each product page) provides recommended cutting speeds for hardened steel machining.
The data is organised by material hardness and HM Series sub-type:
Cutting speed (vc) for hardened steel: HM-4E and HM-4EP series (4-flute, shoulder milling, 0–20mm diameter, 0.05xD depth of cut):
For hardened steel at 55 HRC (machining group 37): The recommended cutting speed range is 55-100-125 m/min. The three values represent the starting, median and upper range. The starting value (55 m/min) is the conservative recommendation for initial setup while 125 m/min is the upper limit for optimal conditions (rigid setup, good coolant, fresh tool). At 55 HRC the HM-4E can operate at productive speeds.
For hardened steel at 60 HRC (machining group 38): The recommended cutting speed range is 55-95-120 m/min. The speeds are slightly reduced compared to 55 HRC, reflecting the increased cutting forces and temperatures at higher hardness. The starting value remains 55 m/min, but the upper limit drops to 120 m/min.
For hardened cast iron at 55 HRC (machining group 40): The recommended cutting speed range is 55-100-125 m/min (the same as hardened steel at 55 HRC) as cast iron machines more freely.
For hardened cast iron at 60 HRC (machining group 39): 70-125-160 m/min. Cast iron at 60 HRC can be cut faster than steel at the same hardness because cast iron produces shorter chips and lower cutting forces.
Feed Rate (fz) Per Tooth: The cutting data specifies feed groups that correspond to feed-per-tooth values based on the diameter and the ae/D (radial depth of cut to diameter ratio). The feed recommendations are on a separate page (referenced as "Feed rate recommendations on page B444" in the cutting data PDF). For hard machining, feed per tooth is typically 0.02-0.08mm for finishing and 0.05-0.15mm for roughing, depending on diameter and flute count.
Key Principles for Hard Machining Parameters:
Reduce cutting speed as hardness increases: The data shows vc dropping from 125 m/min (55 HRC) to 120 m/min (60 HRC). For 65-70 HRC (Pulsar Blue territory), speeds may drop further to 80-100 m/min
Use light depths of cut: The cutting data specifies ae = 0.05xD (radial depth = 5% of diameter) for the listed speeds. Hard machining uses shallow passes (typically 0.05–0.1×D radially and 0.1–0.5×D axially)
Dry cutting for Pulsar Blue: The Pulsar Blue is "suitable for dry cutting" (in hard machining, thermal shock from coolant can crack the carbide edge). Dry cutting with the AlTiN/nanograin coating allows the heat to stay in the chip and be evacuated. The HM Series can be used wet or dry
Climb milling: Hard machining should use climb (down) milling, not conventional (up) milling. Climb milling produces thinner chips at the exit, reducing edge stress and chipping.
The product descriptions include shank designations, for example, the HM4RPD80R05KMG555 is described as "Shaft HA" (HA shank).
Shank designations indicate the shank type and tolerance:
HA (Shank HA): The standard shank designation in the ZCC-CT HM Series. "HA" indicates a plain cylindrical shank with a standard tolerance (typically h6) (the shank diameter is ground to a precise tolerance for collet or shrink-fit holding). The HA shank is the most common type, suitable for collet chucks (ER collets), side-lock holders and shrink-fit holders. The HA shank on the HM4RPD80R05KMG555 is 8mm diameter (matching the cutting diameter for this non-reduced-neck example, though this is a reduced-neck tool so the shank may be larger than the neck).
Shank vs Cutting Diameter: For standard end mills, the shank diameter equals the cutting diameter. For reduced-neck tools (HM-4RP), the shank diameter equals the cutting diameter but the neck between the flutes and shank is reduced. For necked tools the shank may be larger than the cutting diameter (a "necked" tool where a smaller cutting section is mounted on a larger shank for rigidity).
Holder Compatibility:
The shank diameter must match the tool holder:
4mm shank (687 products): Fits ER11 collets (or larger). Common for small-diameter cutters
6mm shank (717 products): Fits ER16 collets (or larger). The most common shank size, covering 2–6mm cutting diameters
8mm shank (120 products): Fits ER20 collets
10mm shank (135 products): Fits ER20 or ER25 collets
12mm shank (132 products): Fits ER25 collets
16mm–25mm shank: Fits ER32 or ER40 collets or shrink-fit holders.
Shrink-fit Holding: For hard machining at high speeds, shrink-fit holders provide the best runout accuracy and gripping force. The HA shank tolerance (h6) is suitable for shrink-fit because the holder is heated, the tool inserted and the holder contracts on cooling to grip the shank with high force and concentricity. Shrink-fit is recommended for hard machining where runout must be minimised (runout causes uneven chip load and edge chipping in hardened steel).
Selecting the correct cutter requires matching seven parameters:
1. Workpiece Hardness: Determine the HRC of the hardened steel.
For up to 55 HRC → Nano-Mill Max-Mill (TiAlN, economical)
For 55–68 HRC → ZCC-CT HM Series (KMG555, production)
For 65–70 HRC → Europa Tool Pulsar Blue (nanograin carbide, maximum hardness).
2. Operation Type:
Slotting/plunging → 2-flute (chip space)
General profiling → 4-flute (balance)
High-feed finishing → 6-flute (edge count)
Precision finishing → 8-flute (surface finish)
3D contouring → ball nose
Roughing → corner radius (edge strength)
Sharp corners → square.
3. Feature Geometry:
Flat bottoms and sharp corners → square
3D curves and mould cavities → ball nose
Flat bottoms with filleted corners → corner radius
Deep walls past obstacles → reduced neck (HM-4RP)
Deep pockets → long length.
4. Diameter: Match to feature size, small features need small diameters.
For general profiling, 6–12mm is typical
For mould cavities, 3–10mm ball nose
For micro-detail, 0.1–2mm.
Ensure the shank diameter matches your holder!
5. Length: Use the minimum length that reaches the machining depth.
Standard for general work
Long for deep cavities (with conservative parameters)
Short for maximum rigidity on shallow features.
6. Coating & Substrate:
KMG555 (HM Series) for 55-68 HRC
Nanograin carbide (Pulsar Blue) for 65-70 HRC
TiAlN (Max-Mill) for up to 55 HRC.
7. Rigidity & Setup: Hard machining requires a rigid setup: rigid machine, short tool projection, shrink-fit or high-precision collet holding and minimal runout. A cutter that is correct in all other parameters will fail if the setup is not rigid enough to prevent deflection and chatter.