


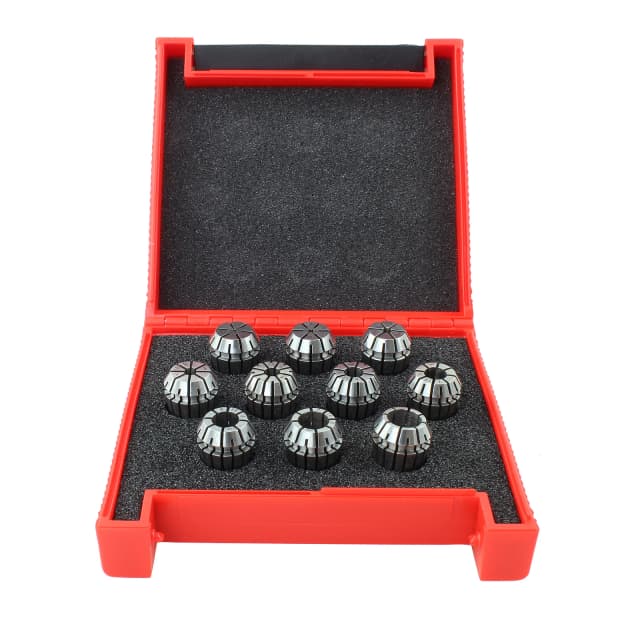
ER16 standard type collet set with max 15 micron runout - 10 piece standard precision ER collets : 1mm - 10mm in 1mm increments.
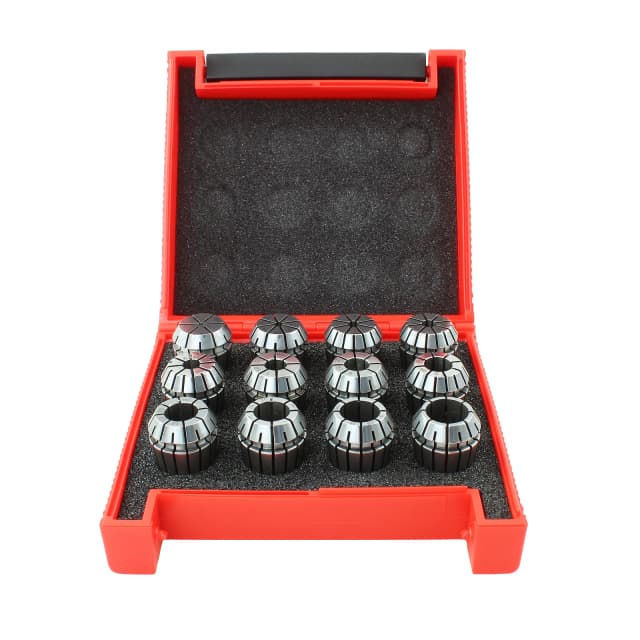
ER20 standard type collet set with max 15 micron runout - 12 piece standard precision ER collets : 2mm - 13mm in 1mm increments.
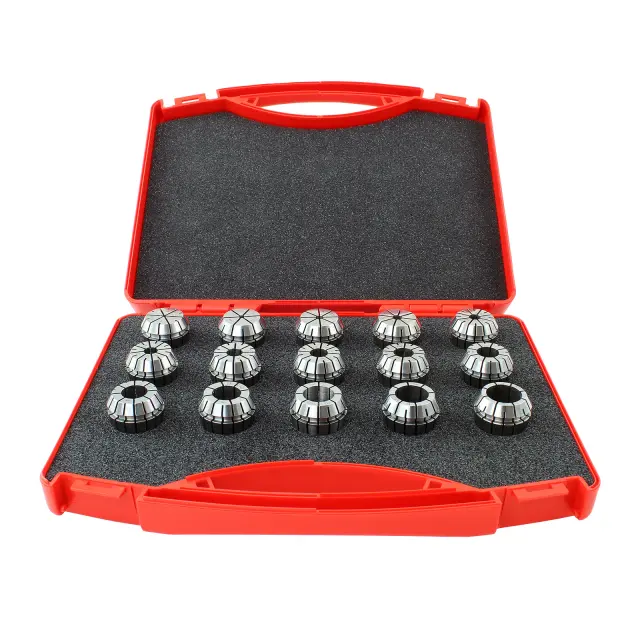
ER25 standard type collet set with max 15 micron runout - 15 piece standard precision ER collets : 2mm - 16mm in 1mm increments.
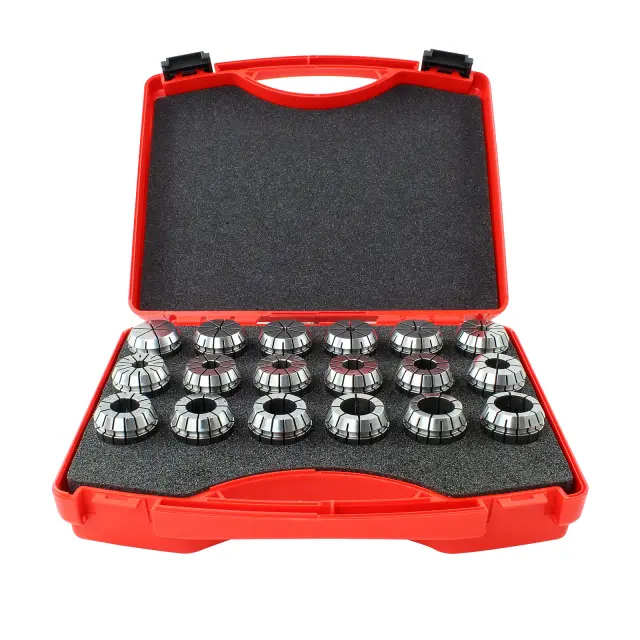
ER32 standard type collet set with max 15 micron runout - 18 piece standard precision ER collets : 3mm - 20mm in 1mm increments.
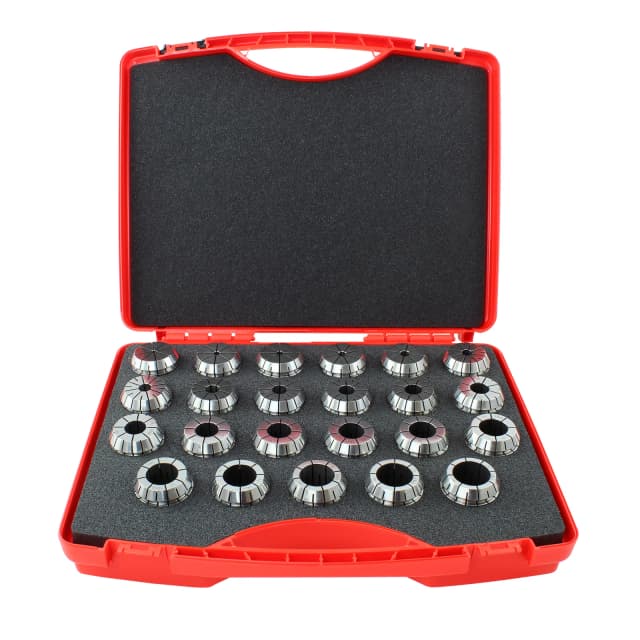
ER40 standard type collet set with max 15 micron runout - 23 piece standard precision ER collets : 4mm - 26mm in 1mm increments.
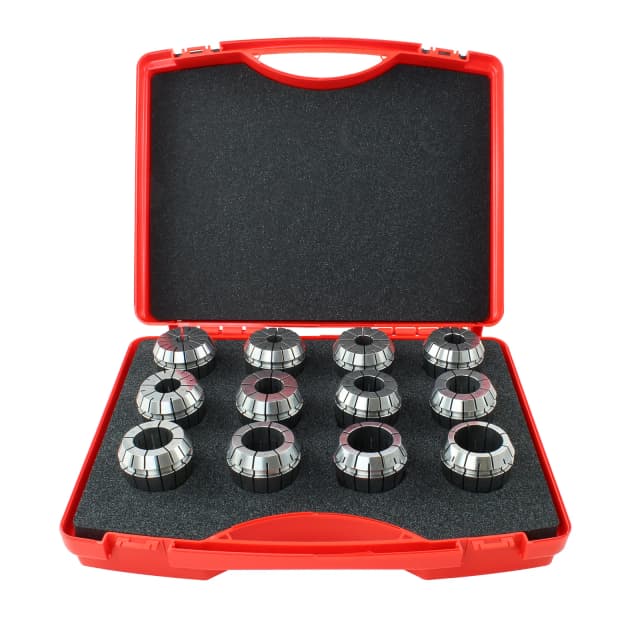
ER50 standard type collet set with max 15 micron runout - 12 piece standard precision ER collets : 12mm - 34mm in 2mm increments.
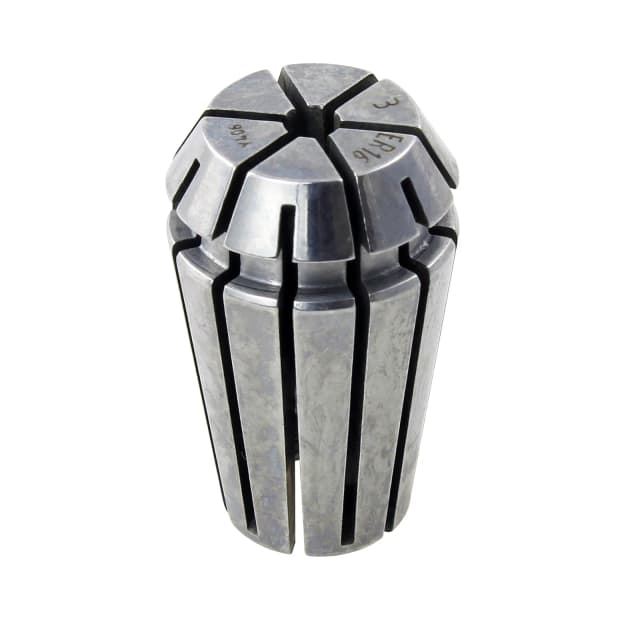
ER16 standard type 15 micron runout collets, available in diameters from 1mm to 12.5mm. The standard type, standard accuracy variants of ER collets - the world's most widely used clamping system, used for a wide array of standard precision machining applications.
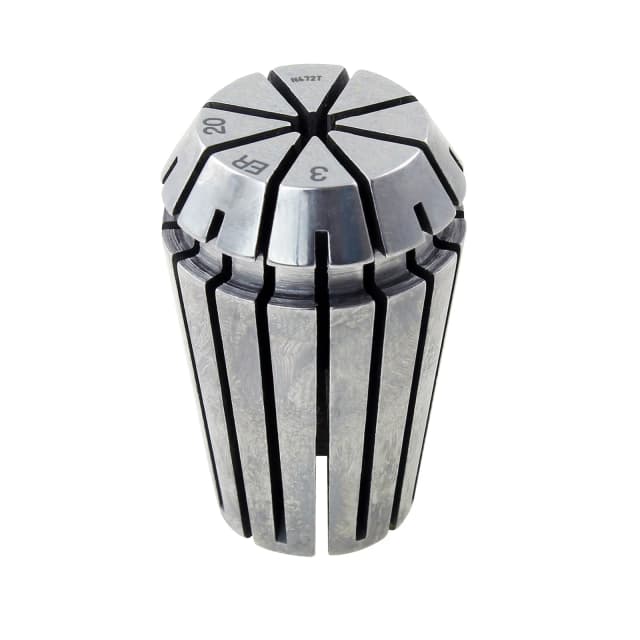
ER20 standard <15 micron runout collets, available in diameters from 1.00mm - 13.00mm. Standard type, standard accuracy ER collets
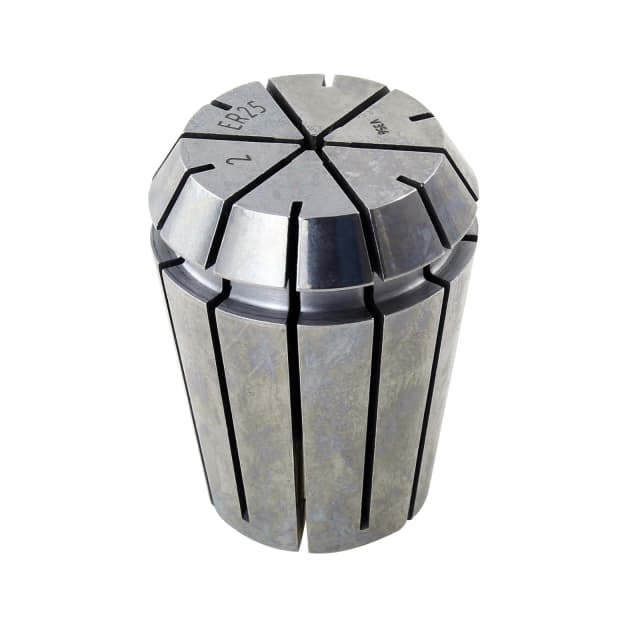
ER25 standard type 15 micron runout collets, available in diameters from 1mm to 20mm. The standard type, standard accuracy variants of ER collets - the world's most widely used clamping system, used for a wide array of standard precision machining applications.
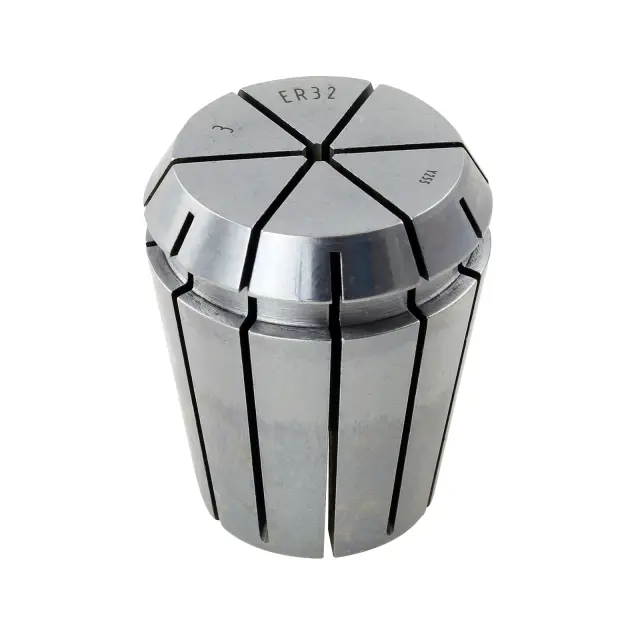
ER32 standard type 15 micron runout collets, available in diameters from 1mm to 25mm. The standard type, standard accuracy variants of ER collets - the world's most widely used clamping system, used for a wide array of standard precision machining applications.
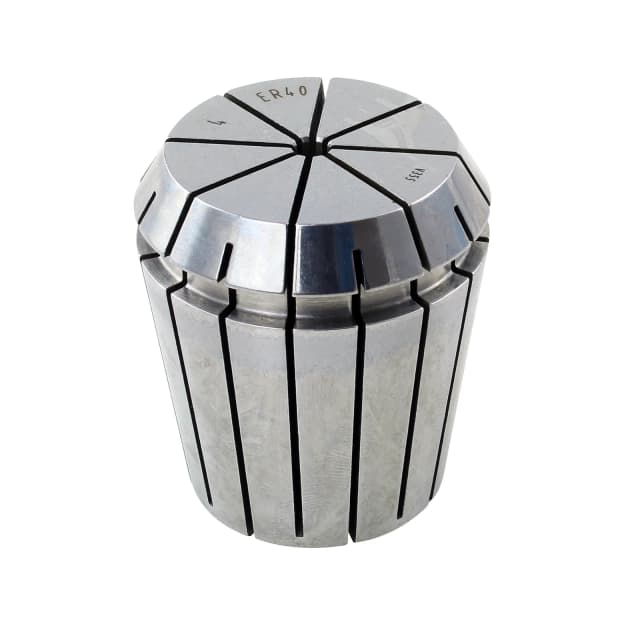
ER40 standard type <15 micron runout collets, available in diameters from 1mm to 32mm. The standard type, standard accuracy variants of ER collets - the world's most widely used clamping system, used for a wide array of standard precision machining applications.
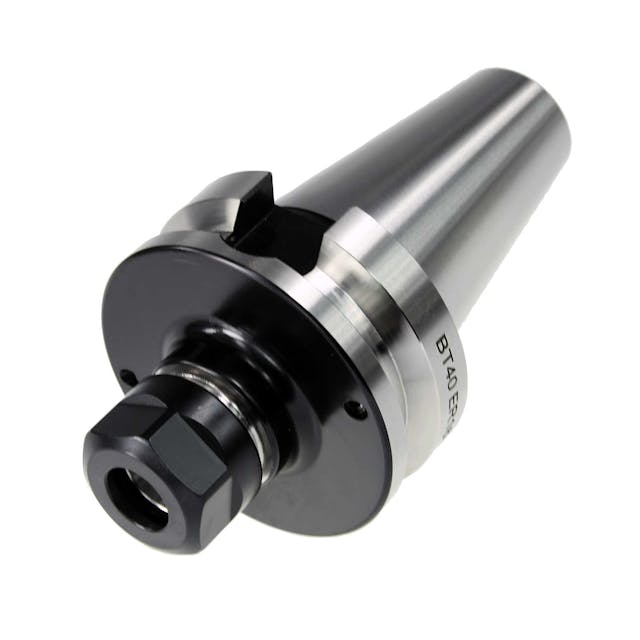
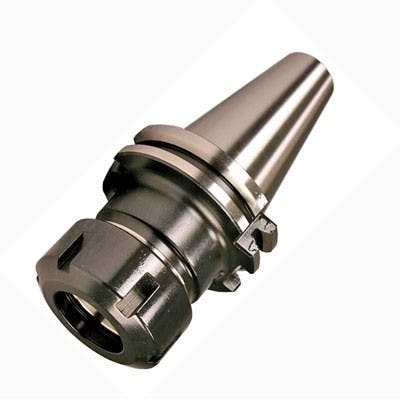
BT40 ER Collet Chucks
BT40 taper (BT MAS)
Balanced at 12,000 rpm G2.5
Buy 5 for £99 - Mix & Match - This offer is only available by phone
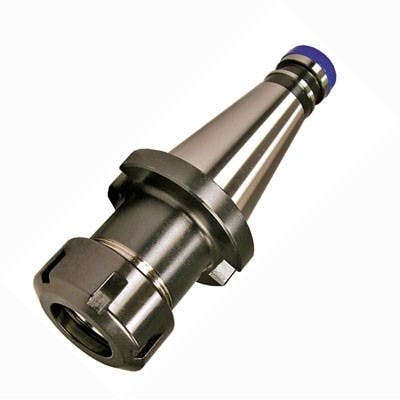
SK40 ER collet chucks
SK40 taper (DIN69871)
Balanced at 12,000 rpm G2.5
Buy 5 for £99 - Mix & Match - This offer is only available by phone
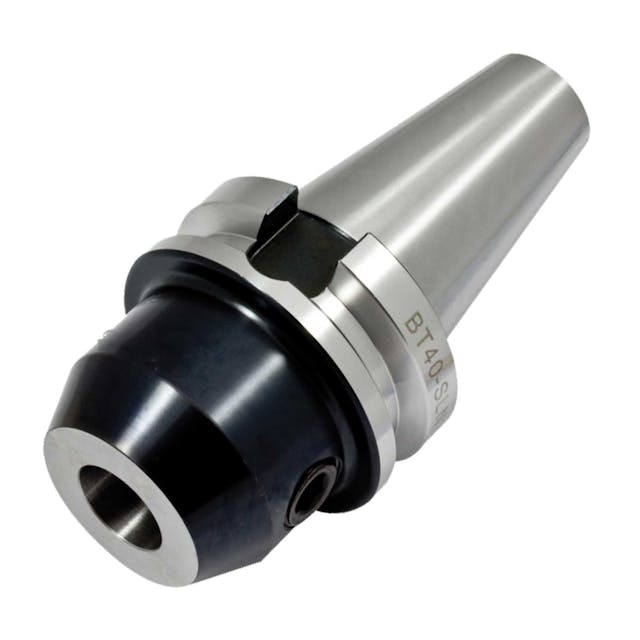
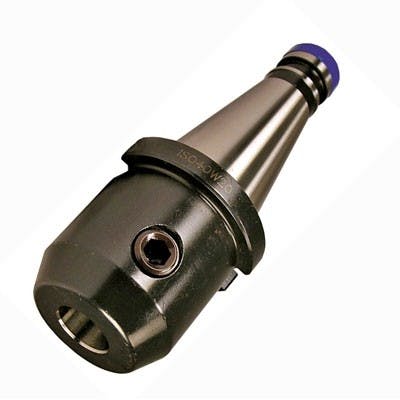
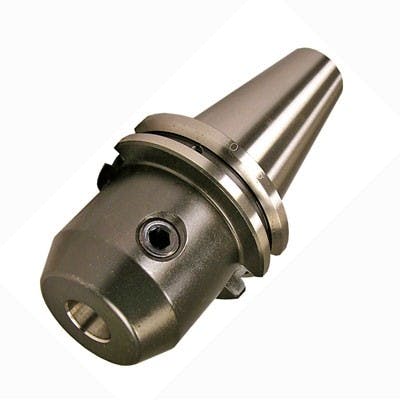
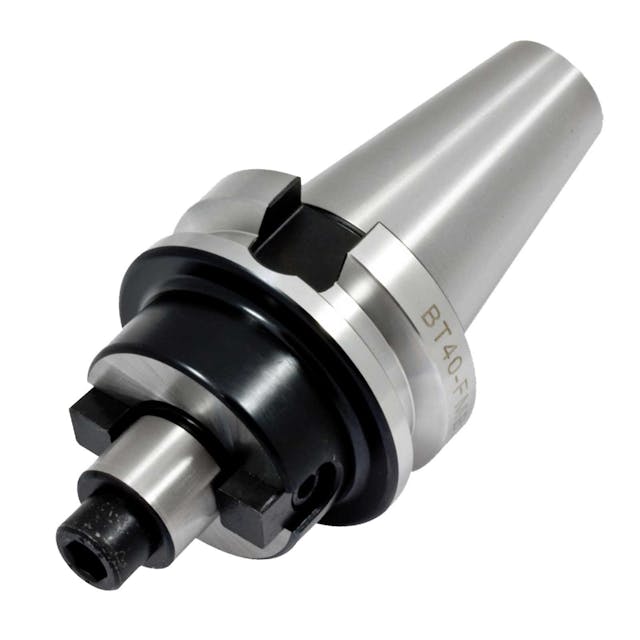
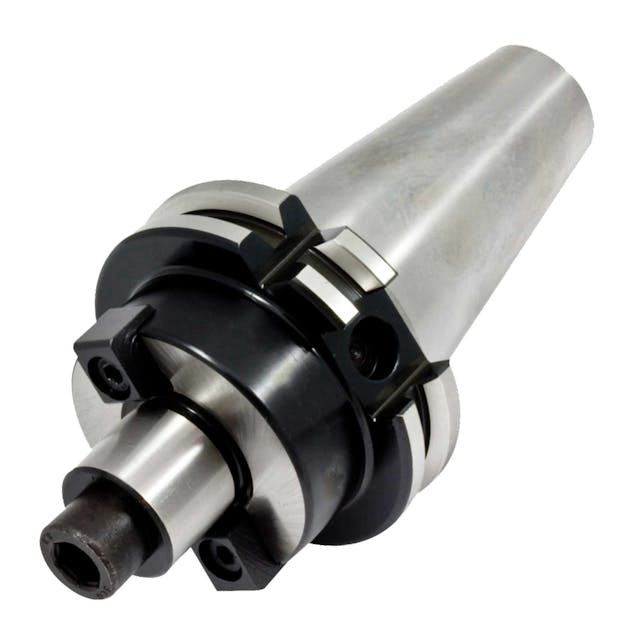
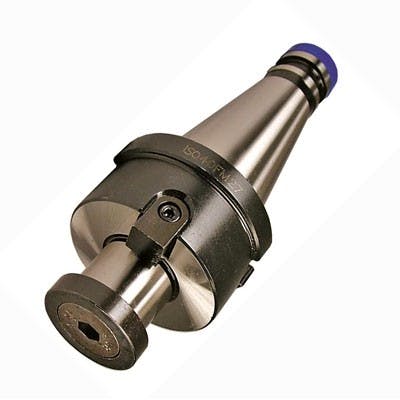
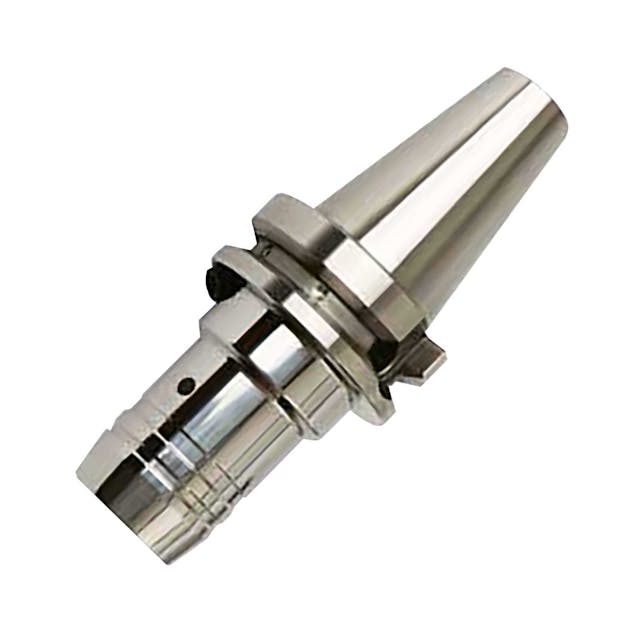
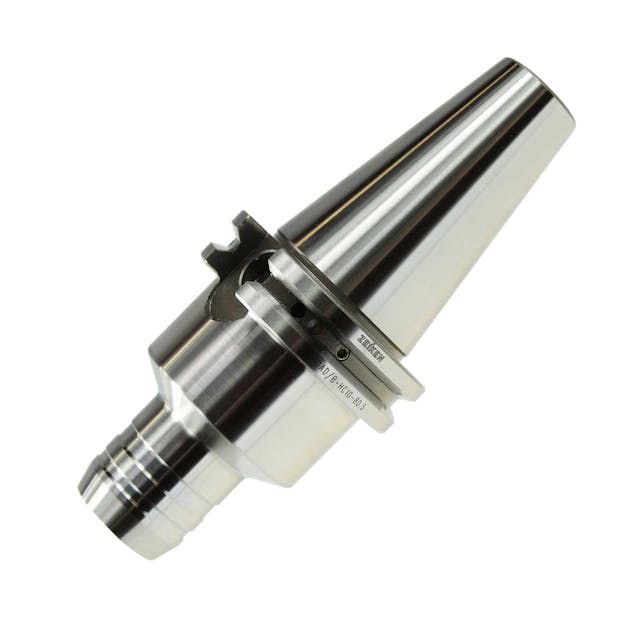
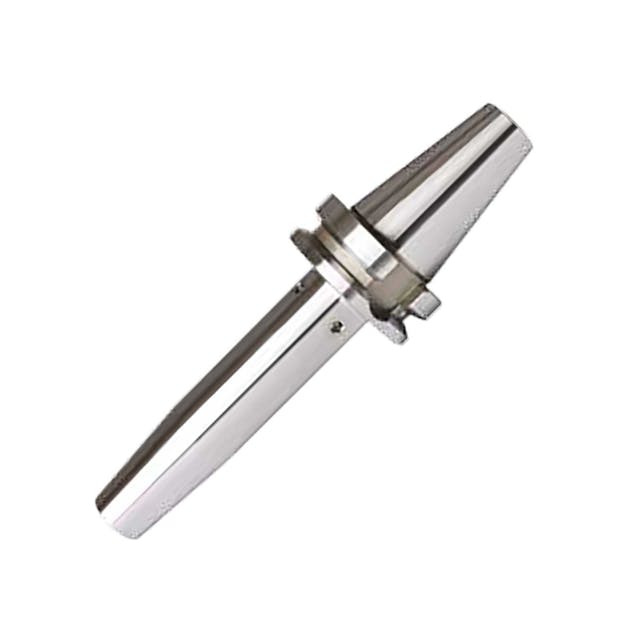
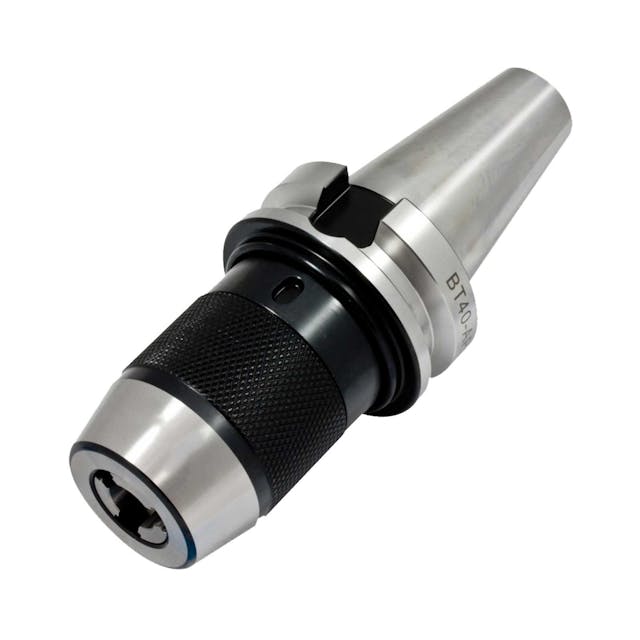
Our Tool Holding section is divided into four areas covering both milling and turning machine applications:
Toolholders that fit into the machining centre or milling machine spindle which includes ER collet chucks, end mill holders, face mill arbors, hydraulic chucks, shrink fit chucks, drill chucks, morse taper adaptors and screwed shank arbors.
Collets, nuts, pull studs/retention knobs, collet spanners and other accessories to complete the toolholding assembly.
Quick Change Toolposts & Tool Holders
Bison-brand quick change toolpost systems for manual and CNC lathes that allow rapid, repeatable tool changeover without resetting centre height.
CNC lathe turret toolholders, VDI static holders, BMT-mount static & driven holders and angle heads for live tooling operations.
An end mill holder (also called a side lock arbor or Weldon shank holder) clamps the tool using a grub screw that bears against a flat ground into the tool shank (the Weldon flat). The grub screw is tightened through a hole in the side of the holder body.
When to use end mill holders:
Heavy-duty roughing where maximum torque transmission is required and pull-out risk is a concern
Tools with Weldon flats: some manufacturers grind Weldon flats specifically to be used with side lock holders
Large diameter face mills and shell mills where the side lock is the standard mounting method
Limitations:
Not suitable for tools without a Weldon flat as the grub screw will damage a plain round shank
Inherently poor runout where the grub screw bears against one side only, pushing the tool slightly off-centre - typical runout 5–20µm depending on the holder quality
Not suitable for finishing operations or small-diameter tools where runout matters
Each holder is sized for one specific shank diameter
For end mills below 20mm diameter where both roughing and finishing will be performed with the same tool an ER collet chuck is generally preferable to a side lock holder as it provides adequate torque for most operations with better runout.
Three principal mount types are found across the lathe tool holder range:
VDI (Verband Deutscher Ingenieure)
Cylindrical shank with anti-rotation flat and bolt pattern
The most common European CNC turret standard
Snap-in / bolt-in fitment; good repeatability
Sizes: VDI 30, 40, 50 (and 60 for large machines)
Face-mount interface where the holder bolts directly to a flat face on the turret disc using a bolt circle
Very common on Korean-built CNC lathes (Doosan, Hyundai-WIA etc) and increasingly on Mazak and other brands
Superior rigidity for driven (live) toolholders compared to VDI the face contact transmits cutting forces more directly into the turret disc
Sizes stocked include: BMT 45, BMT 55, BMT 65, BMT 75, BMT 85 (and EM variants — with extended mounting dimensions)
Cylindrical Shank
Simple cylindrical shank clamped in a bore in the turret and typically used on older or smaller turrets
To identify which mount your lathe uses check the machine manual or measure the turret interface. If unsure, contact us with the make, model and year of manufacture.