

Corner Radius Milling Cutters
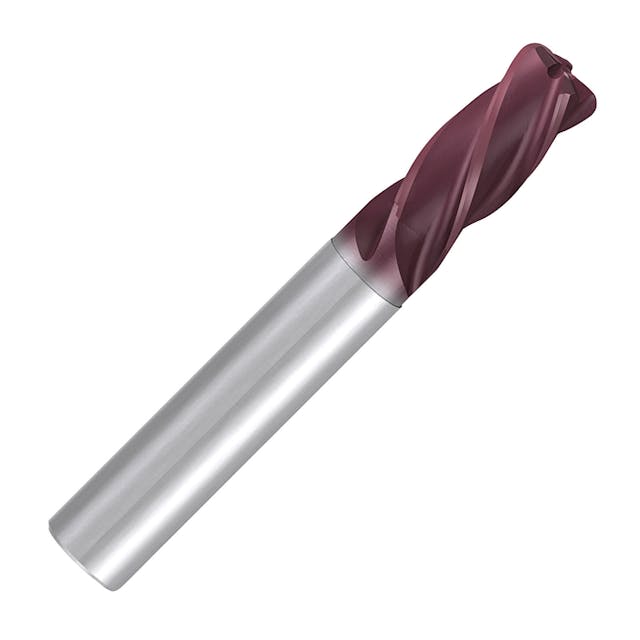
FRANKEN 4 Flute Solid Carbide Corner Radius End Mill
FRANKEN Top-Cut 4 Flute Corner Radius High Performance End Mill
- Solid micrograin carbide
- TiALN coated
- Centre cutting
- Variable helix geometry
- Rough and finish with 1 tool
- Corner radius
- Several coerner radii per cutting diameter
- Suitable for steel, stainless steel, cast iron, titanium and HRSA
£29.60 excl. VAT
£35.52 incl. VAT
£25.83excl. VAT
£31.00incl. VAT
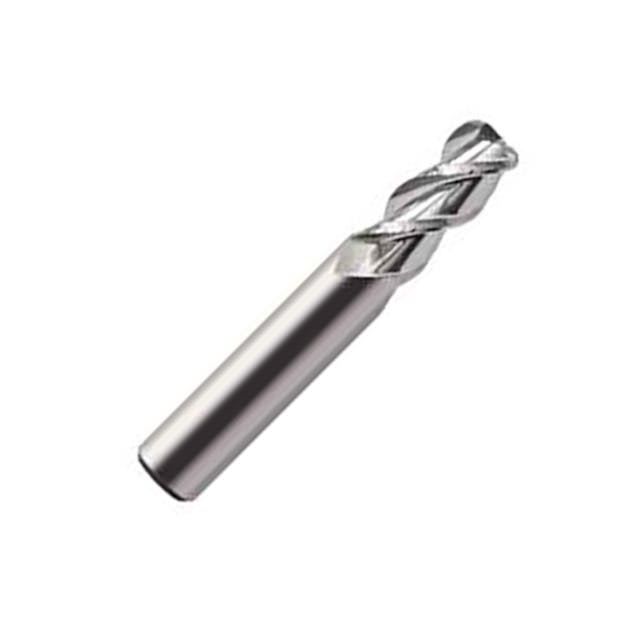
Alu-XP 142303 Series 3 Flute Carbide Corner Radius End Mill for Aluminium & Non-Ferrous Machining
Alu-XP tools with Òmirror polishedÓ flutes allow for smooth chip evacuation, giving better surface finish and wear resistance. Cutting edges are optimised to minimise vibration, and 3-flute tools have a tight diameter tolerance giving excellent process reliability.
£16.06 excl. VAT
£19.27 incl. VAT
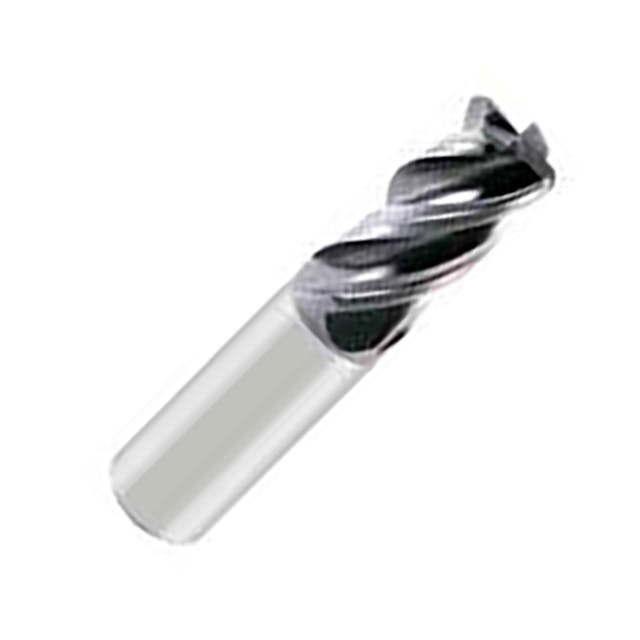
MasterMill VX Series 4 Flute Corner Radius High Performance End Mill
- Corner radius
- Solid micrograin carbide
- Chamfered for corner protection
- Minimized tool deflection
- Reduced tool vibration
- Multi layer VX coating
- Variable helix geometry
- Suitable for high perfromance machining of Steel, Stainless steel, Titanium and nickel alloy
ZCC-CT HM-4R 4 Flute Corner Radius End Mill for Hardened Steel
ZCC-CT HM-4R 4 Flute Corner Radius End Mill With Straight Shank
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
£25.50 excl. VAT
£30.60 incl. VAT
Pulsar Blue 4 Flute High Feed Corner Radius End Mill for Hardened Steel
Pulsar Blue 4 Flute High Feed Corner Radius End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- Corner radius
- High speed cutting
- High feed geometry
- Short flute for maximum strength
Alu-XP 156303 Series 2 Flute Carbide Corner Radius Reduced Neck End Mill for Aluminium & Non-Ferrous Machining
Alu-XP tools with Òmirror polishedÓ flutes allow for smooth chip evacuation, giving better surface finish and wear resistance. Cutting edges are optimised to minimise vibration, and 3-flute tools have a tight diameter tolerance giving excellent process reliability.
Pulsar Blue 4 Flute Extended Neck Corner Radius Stub Length End Mill for Hardened Steel
Pulsar Blue 4 Flute Extended Neck Corner Radius Stub Length End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Corner radius
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
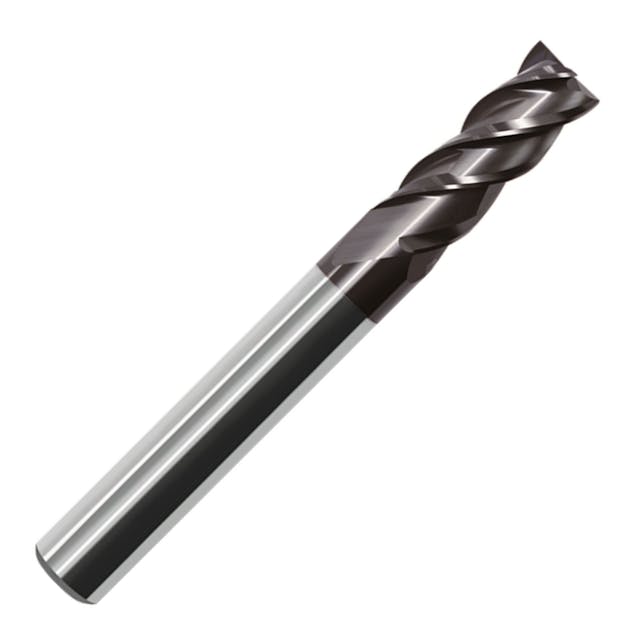
ZCC-CT UM-4R 4 Flute Corner Radius Variable Helix End Mill
ZCC-CT UM-4R Series 4 Flute Standard Length Corner Radius AlCrN Coated High Performance Variable Helix Solid Carbide End Mill
- Optimised geometry with unequal 38 degree and 41 degree helix angles and unequal pitch.
- Working processes: Square shoulder milling, groove milling, face milling, counter sinking, circular milling and centre cutting.
- End mills and torus Mills.
- HSC/HPC machining.
- AlCrN (Aluminium Chromium Nitride) coated solid carbide for exceptional tool life.
£22.26 excl. VAT
£26.71 incl. VAT
£18.92excl. VAT
£22.70incl. VAT
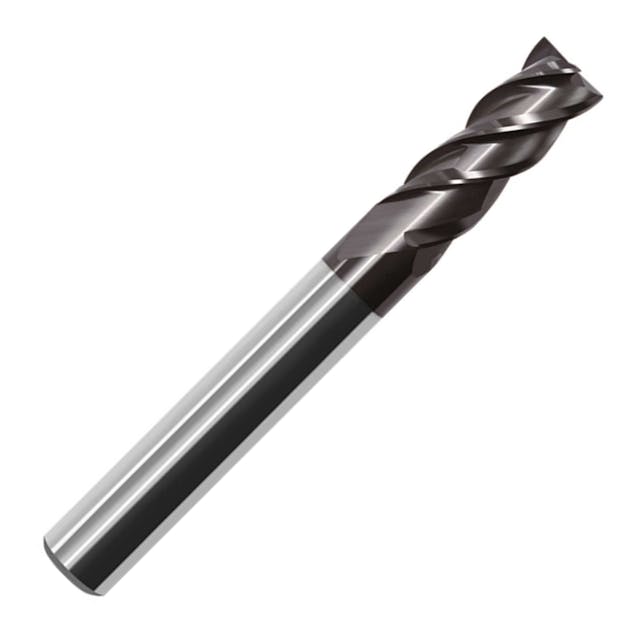
ZCC-CT UM-4RL 4 Flute Long Length Corner Radius Variable Helix End Mill
ZCC-CT UM-4RL Series 4 Flute Long Length Corner Radius AlCrN Coated High Performance Variable Helix Solid Carbide End Mill
- Optimised geometry with unequal 38 degree and 41 degree helix angles and unequal pitch.
- Working processes: Square shoulder milling, groove milling, face milling, counter sinking, circular milling and centre cutting.
- End mills and torus Mills.
- HSC/HPC machining.
- AlCrN (Aluminium Chromium Nitride) coated solid carbide for exceptional tool life.
£25.03 excl. VAT
£30.04 incl. VAT
£21.28excl. VAT
£25.54incl. VAT
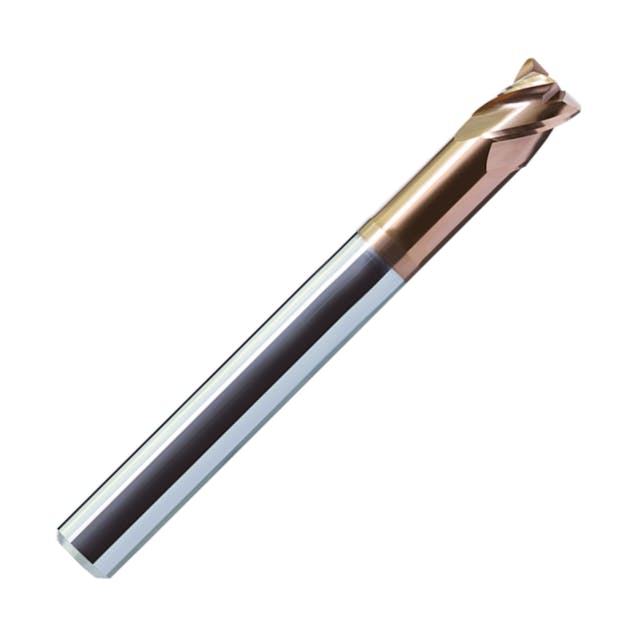
ZCC-CT HM-4RP 4 Flute Reduced Neck Corner Radius End Mill for Hardened Steel
ZCC-CT 4 Flute Reduced Neck Corner Radius End Mill
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
£26.25 excl. VAT
£31.50 incl. VAT
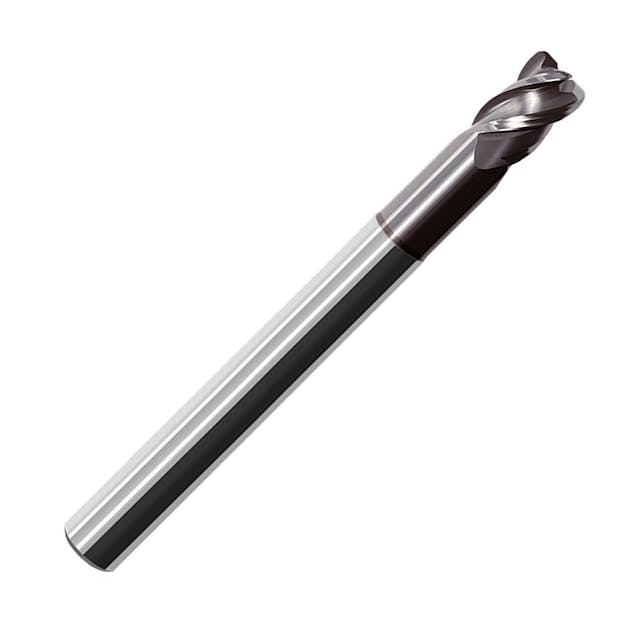
ZCC-CT UM-4RFP 4 Flute Short Cutting Edge Corner Radius Variable Helix End Mill
ZCC-CT UM-4RFP Series 4 Flute Short Cutting Edge Corner Radius AlCrN Coated High Performance Variable Helix Solid Carbide End Mill
- Optimised geometry with unequal 38 degree and 41 degree helix angles and unequal pitch.
- Working processes: Square shoulder milling, groove milling, face milling, counter sinking, circular milling and centre cutting.
- End mills and torus Mills.
- HSC/HPC machining.
- AlCrN (Aluminium Chromium Nitride) coated solid carbide for exceptional tool life.
£25.03 excl. VAT
£30.04 incl. VAT
£21.28excl. VAT
£25.54incl. VAT
Pulsar Blue 4 Flute Extended Neck Corner Radius Long Length End Mill for Hardened Steel
Pulsar Blue 4 Flute Extended Neck Corner Radius Long Length End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Corner radius
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
Pulsar Blue High Feed Long Length Corner Radius End Mill for Hardened Steel
Pulsar Blue 4 Flute High Feed Long Length Corner Radius End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- Corner radius
- High speed cutting
- High feed geometry
- Short flute for maximum strength
2 Flute Corner Radius Long Length End Mill for Aluminium
2 Flute Corner Radius Long Length End Mill for Aluminium
- Newly developed geometry
- New KMD401 diamond like coating for significantly improved tool life
- Wide range of radii available on larger diameters
£45.15 excl. VAT
£54.18 incl. VAT
FRANKEN 3 Flute Long Length Corner Radius For Aluminium
Franken Alu-Cut solid carbide 3 flute long length end mills for high performance machining of aluminium, wrought aluminium alloys and aluminium alloys with a silicon content of up to 7%.
Features:
- High performance tool.
- Special geometry for the machining of aluminium
- Centre cutting
- 3 Flute Ripper
- Several corner radii per cutting diameter
- Suitable for z-axis milling
- Suitable for roughing and finishing
- Low-vibration machining
£44.30 excl. VAT
£53.16 incl. VAT
£38.70excl. VAT
£46.44incl. VAT
Mastermill VX5 Series 5 Flute High Performance Corner Radius Ripper
MasterMill VX5 175323 Series 5 Flute High Performance Corner Radius Ripper
- Solid micrograin carbide
- Fine pitch roughing end mill
- Corner radius
- Multi layer VX coated
- Variable helix geometry
- Suitable for high perfromance machining of Steel, Stainless steel, Titanium and nickel alloy
- Exceptional performance in Titanium, Inconel and other HRSA materials
- High rigidity of flute for heavy profiling and high speed machining
- Reinforced cutting edge
AL-2R 2 Flute Corner Radius End Mill for Aluminium
AL-2R 2 Flute Corner Radius End Mill for Aluminium
- Newly developed geometry
- New KMD401 diamond like coating for significantly improved tool life
- Wide range of radii available on larger diameters
£40.16 excl. VAT
£48.19 incl. VAT
ZCC-CT TM-4R Series 4 Flute KMS405 Coated Carbide Corner Radius End Mill for Titanium & Heat-Resistant Alloy Machining
ZCC-CTÕs new TM range of high performance milling cutters for heat resistant super-alloys feature a revolutionary proprietary KMS405 coating for exceptional thermal stability and wear resistance.
£27.02 excl. VAT
£32.42 incl. VAT
£22.97excl. VAT
£27.56incl. VAT
ZCC-CT TM-4RP Series 4 Flute KMS405 Coated Carbide Corner Radius Reduced Neck End Mill for Titanium & Heat-Resistant Alloy Machining
ZCC-CTÕs new TM range of high performance milling cutters for heat resistant super-alloys feature a revolutionary proprietary KMS405 coating for exceptional thermal stability and wear resistance.
£45.35 excl. VAT
£54.42 incl. VAT
£38.55excl. VAT
£46.26incl. VAT
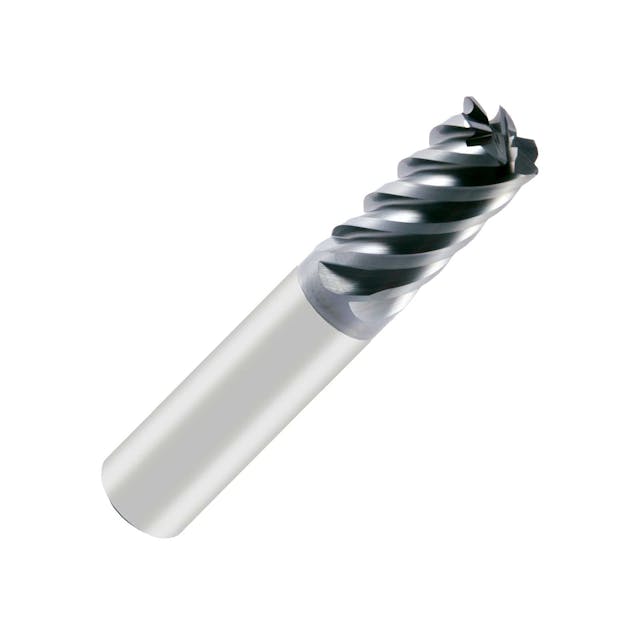
MasterMill VX6 Series 6 Flute High Performance Corner Radius End Mill
MasterMill VX6 176329 Series 6 Flute High Performance Corner Radius End Mill
- Solid micrograin carbide
- Optimised for high speed and trochoidal milling
- Corner radius
- Multi layer VX coated
- Variable helix geometry
- Suitable for high perfromance machining of Steel, Stainless steel, Titanium and nickel alloy
- Exceptional performance in Titanium, Inconel and other HRSA materials
MasterMill VX Series 4 Flute Long Length Necked Corner radius High Performance End Mill
- Solid micrograin carbide
- Long series
- Necked design
- Corner radius
- Minimized tool deflection
- Reduced tool vibration
- Multi layer VX coating
- Variable helix geometry
- Suitable for high perfromance machining of Steel, Stainless steel, Titanium and nickel alloy
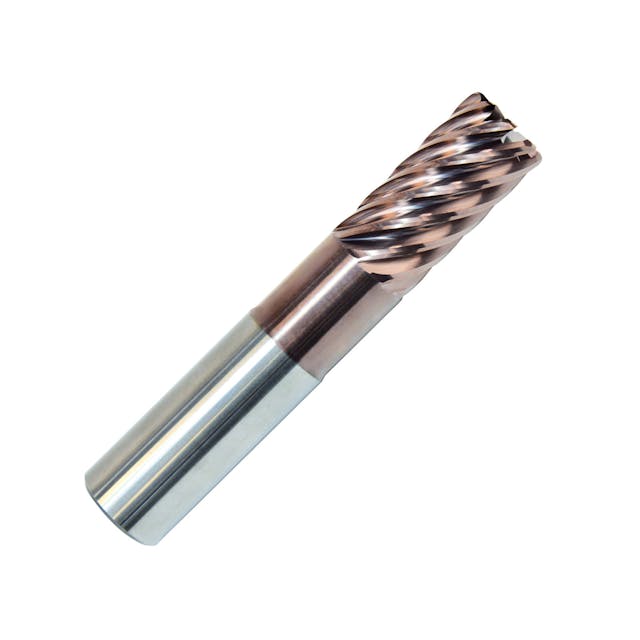
ZCC-CT TM-9RP Series 9 Flute KMS405 Coated Carbide Corner Radius Reduced Neck End Mill for Titanium & Heat-Resistant Alloy Machining
ZCC-CTÕs new TM range of high performance milling cutters for heat resistant super-alloys feature a revolutionary proprietary KMS405 coating for exceptional thermal stability and wear resistance.
£693.67 excl. VAT
£832.40 incl. VAT
£589.62excl. VAT
£707.54incl. VAT
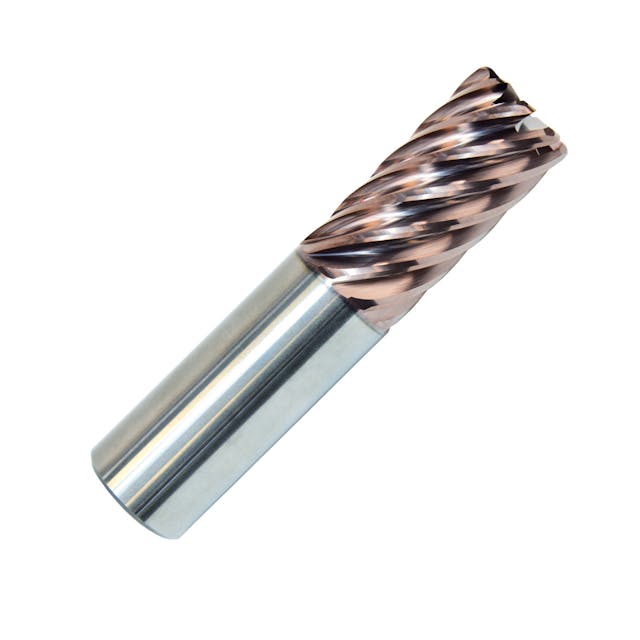
ZCC-CT TM-9R Series 9 Flute KMS405 Coated Carbide Corner Radius End Mill for Titanium & Heat-Resistant Alloy Machining
ZCC-CTÕs new TM range of high performance milling cutters for heat resistant super-alloys feature a revolutionary proprietary KMS405 coating for exceptional thermal stability and wear resistance.
£519.17 excl. VAT
£623.00 incl. VAT
£441.29excl. VAT
£529.55incl. VAT
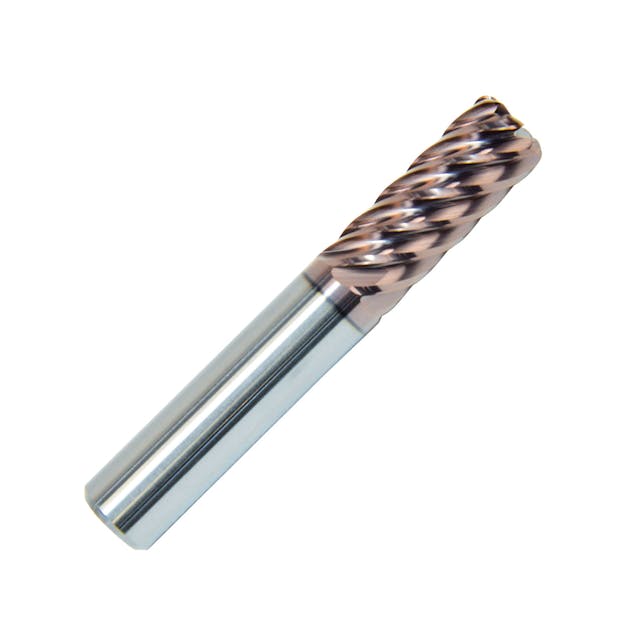
ZCC-CT TM-7R Series 7 Flute KMS405 Coated Carbide Corner Radius End Mill for Titanium & Heat-Resistant Alloy Machining
ZCC-CTÕs new TM range of high performance milling cutters for heat resistant super-alloys feature a revolutionary proprietary KMS405 coating for exceptional thermal stability and wear resistance.
£93.89 excl. VAT
£112.67 incl. VAT
£79.81excl. VAT
£95.77incl. VAT
Frequently Asked Questions
A corner radius cutter (sometimes called a bull-nose end mill) is a solid end mill with a radiused corner blended between the periphery and the flat bottom. Where a square-end mill has a sharp 90° corner, a corner radius cutter has a fixed radius at that corner and where a ball-nose is fully radiused across the whole tip, a corner radius cutter keeps a flat bottom with only the corner radiused. The geometry sits between the two: most of the cutting is done on the periphery and the flat bottom, with the radius just blending the corner.
The result is a cutter that cuts a flat floor with a fillet at the wall rather than the sharp internal corner a square-end mill leaves or the full spherical floor a ball-nose produces.
The radius strengthens the weakest point of an end mill (the sharp corner is the first thing to chip) so a corner radius cutter holds its edge longer and takes heavier cuts than the equivalent square-end mill. For pocketing, profiling & shoulder milling where a sharp internal corner is not required, the corner radius cutter is the everyday choice.
Two reasons dominate this choice: tool life and part integrity.
The sharp corner of a square-end mill is the most stress-concentrated point on the tool, and it is the first thing to chip under a heavy cut, an interrupted entry or a hard spot in the material.
A radiused corner spreads that stress over a larger area, so the edge holds up to heavier cuts, interrupted cuts and harder materials where a sharp corner would fail in minutes.
On the part side, an internal corner cut with a square-end mill is a sharp 90° that becomes a stress-raiser in the finished component; a crack initiator in service, especially in harder or fatigue-critical parts.
A corner radius leaves a fillet, which is why most engineering drawings specify a radius at the root of a pocket or shoulder. Choosing a corner radius cutter gives both the longer tool life and the fillet the drawing asks for, which is why it is the default choice for production milling in this category.
The corner radius is chosen for the part first and the tool second. The drawing specifies a maximum fillet radius at the root of a pocket or shoulder and the cutter radius must be equal to or smaller than that because a cutter larger than the drawing radius will leave a fillet that violates the part. Within that limit, choose the largest radius you can, because a larger radius strengthens the corner more and gives longer tool life.
Where the drawing calls for a sharp internal corner (no fillet) a corner radius cutter cannot be used; you need a square-end mill for that feature or a corner-radius rough-out followed by a square-end finish.
For the common case where the drawing allows a fillet, pick the largest radius that fits, match it to the pocket corner and keep a small stock of the common radii (0.5, 1, 2, 3 mm) so the right cutter is to hand.
The radius is specified on the cutter as a dimension, not a code, so it is straightforward to select.
On a corner radius cutter the shank is the plain cylindrical portion held in the collet or holder and the cutting diameter is the diameter of the fluted cutting portion.
On many cutters the shank and the cutting diameter are the same (a 10 mm cutter with a 10 mm shank) which gives the most rigid set-up and the best reach for a given diameter. On others the shank is larger or smaller than the cutting diameter: a necked cutter has a shank smaller than the cutting diameter to reach into a pocket, a reduced-shank cutter has a shank larger than the cutting diameter for rigidity in a shallow cut.
It matters because the shank determines what collet or holder the cutter fits and how deep the cutter can reach before the shank fouls the work.
A 6 mm cutter on a 6 mm shank reaches a pocket of 6 mm or wider; the same 6 mm cutter on a 3 mm necked shank reaches a narrower feature but is less rigid.
Match the shank to your holder (ER collets are the common choice) and choose a necked shank only where the geometry of the part demands the extra reach.
Flute count is chosen for the material and the cut.
A 2-flute cutter has the most flute space, so it clears chips freely in the softer, gummier materials (aluminium, brass, copper) where the chip is long and tends to pack.
A 3-flute is the middle ground, a good all-rounder for the softer steels and stainless.
A 4-flute has less chip space but more cutting edges, so it gives a better finish and a higher feed rate per revolution in the harder, free-cutting materials (steels, cast iron).
A 6-flute is for the harder steels and high-temperature alloys, where the chip is small and the extra edges share the cutting load.
The trade-off here is chip space against edge count.
Too few flutes in a hard material and each edge takes too heavy a chip load and chatters; too many flutes in a soft material and the chips pack the flutes and the cutter seizes.
Our rule of thumb is 2-flute for aluminium and non-ferrous, 3- or 4-flute for general steels, 4- or 6-flute for the harder steels & high-temp alloys and a 4-flute for a finishing pass in steel where the finish matters.
The helix angle is the angle of the flute to the cutter axis.
A low helix (around 30°) gives a stronger cutting edge and lifts the chip less aggressively so it suits the harder, brittle materials and the shallower cuts.
A high helix (45° and above) shears the material more aggressively, lifts the chip faster and gives a better finish in the softer, gummier materials (it suits aluminium and the long-chipping steels). A variable helix (flutes with differing helix angles) breaks up the harmonic that causes chatter, so a variable-helix cutter runs smoother in difficult cuts.
For the bulk of general work a medium helix around 35–40° is the all-rounder. Choose a high helix for aluminium and the long-chipping materials, a low helix for the harder and more brittle materials, and a variable helix where chatter is a known problem on a particular set-up.
The helix is a parameter on the cutter, so it is selected with the material in mind and the right helix makes a real difference to both finish and tool life.
The coatings on corner radius cutters are thin PVD layers applied over the carbide to raise the surface hardness, reduce friction and resist the heat of the cut. The common ones are TiAlN (titanium aluminium nitride) and AlTiN (aluminium titanium nitride) (the general-purpose high-temperature coatings that suit steels, stainless and cast iron). There are specialist coatings for hardened steel, for high-temperature alloys and the polished or uncoated cutters for aluminium and non-ferrous (where a coating can build up an edge and a polished bare carbide cuts cleaner).
Match the coating to the material.
A TiAlN or AlTiN is the right general choice for steels and stainless and gives a meaningful speed and life advantage over uncoated. A specialist coating is worth it for the harder or more demanding work such as hardened steel, the HRSA alloys. An uncoated, polished cutter is right for aluminium, brass and copper, where the coating would cause build-up and the polished flute evacuates the soft chip.
The wrong coating in the wrong material will not damage the part but will give poor tool life, so pick the coating for the workpiece.
A corner radius cutter can plunge, but less freely than a centre-cutting end mill. The flat bottom of a corner radius cutter has a centre region that may or may not cut (the geometry depends on the cutter) so plunging straight down is not always possible and is never the preferred entry. Where the cutter is centre-cutting a small plunge is acceptable, but the chips have to escape past the flutes and a deep plunge will pack them; where it is not centre-cutting the cutter will rub and burn the bottom and damage the edge.
For entering a pocket, prefer a ramped or helical entry so the cutter moves down into the pocket in a helical or ramped path, cutting on the periphery and the bottom together, which keeps the chips clearing and the edge cutting.
A pre-drilled entry hole is the other option so it drill a hole larger than the cutter, then drop the cutter into the hole and begin profiling. Plunging a corner radius cutter straight down is the last resort and only at a light feed and only if the cutter is rated for it.
A pocket is roughed out by ramping or helical entry to depth, then profiling the wall and finishing the floor. The cutter enters with a helical ramp (a circular path descending into the work) to the first depth, then takes a series of passes around the pocket perimeter, stepping down in Z and stepping over in X-Y, until the full depth is reached. The floor is then finished with a finishing pass that leaves the specified corner radius at the wall.
The corner radius must be matched to the pocket: the cutter radius equals the fillet radius the drawing calls for, or is smaller and a second pass with a larger cutter leaves the fillet.
The stepover for roughing is typically 50–70% of the cutter diameter, the stepdown is set by the cutter’s rigidity and the material, and the finish pass takes a light cut on the wall and the floor to clean up.
Through-coolant or flood coolant flushes the chips from the pocket and the chip clearing is the thing that limits the depth (a packed pocket will destroy the cutter in a single pass).