

Ball Nose End Mills
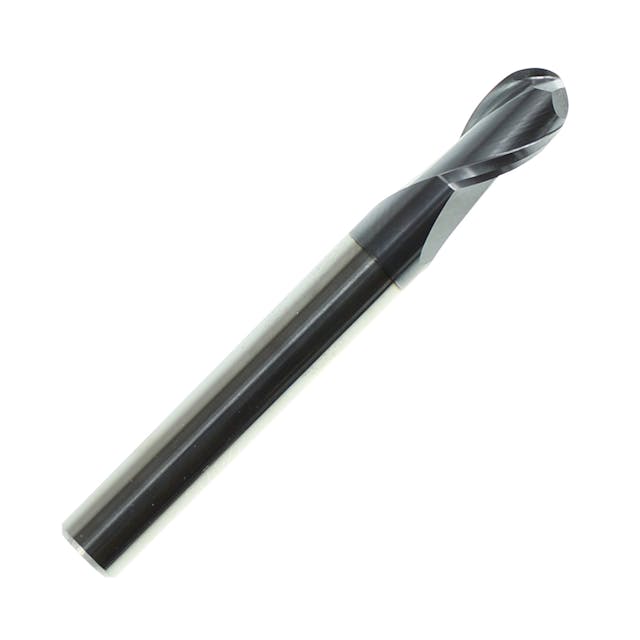
Eco-Mill 2 Flute Coated Carbide Ball Nose Slot Drills
ECO-MILL coated carbide 2 flute ball nosed slot drill from STÄRKE, a TiALN coated general purpose cutter.
- Suitable for cutting steel, stainless steel, cast iron and non-ferrous materials including aluminium alloys and copper.
- Cut up to 45 HRC
- Can be used wet or dry to increase tool life.
- Micrograin carbide
- Available diameter sizes between 1mm and 20mm


£7.78 excl. VAT
£9.34 incl. VAT
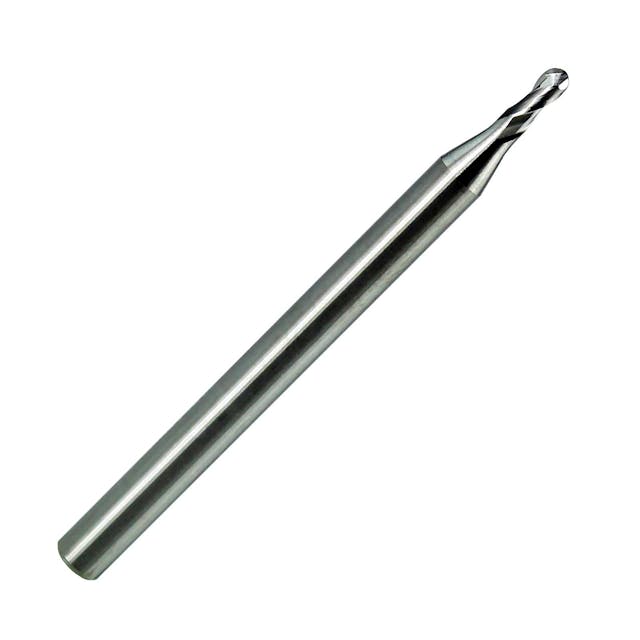
Ali-Mill 2 Flute Ball Nosed Solid Carbide for Aluminium
- Solid micrograin carbide
- 38 degree helix geometry enable better chip removal
- Polished flutes for superior surface finish
- 2 flutes
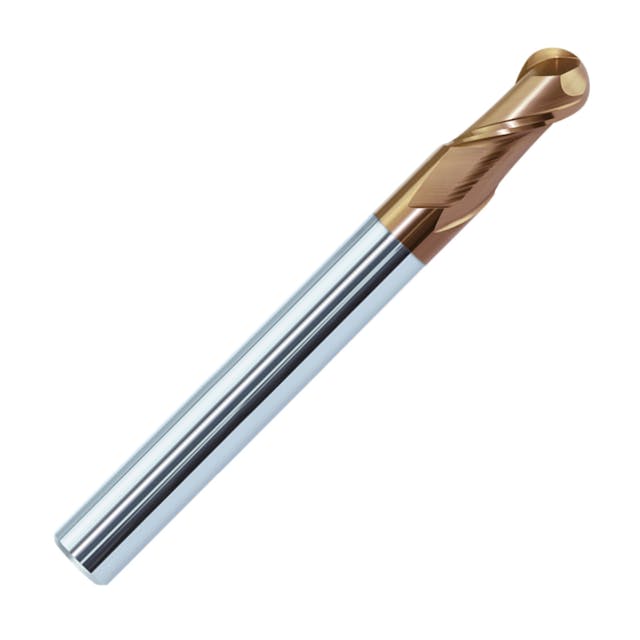
ZCC-CT HM-2BL Series 2 Flute Long Length Ball Nose Slot Drill for Hardened Steel Machining
ZCC-CT 2 Flute Long Length Ball Nose Slot Drill
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
£38.11 excl. VAT
£45.73 incl. VAT

FRANKEN Top-Cut Extra Long Length High Performance Ball Nosed End Mill
FRANKEN Top-Cut Extra Long Length High Performance Ball Nosed End Mill
- Solid micrograin carbide
- TiALN coated
- Extra long
- Centre cutting
- Variable helix geometry
- Rough and finish with 1 tool
- Suitable for steel, stainless steel, cast iron, titanium and HRSA
£48.60 excl. VAT
£58.32 incl. VAT
£41.66excl. VAT
£49.99incl. VAT
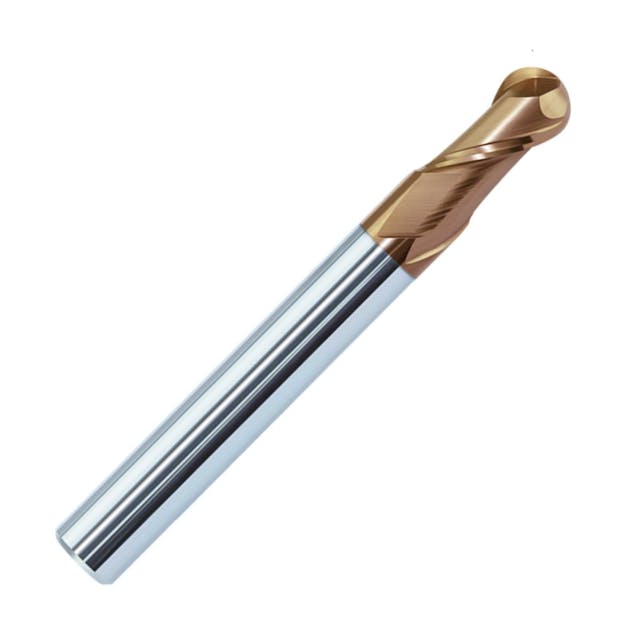
ZCC-CT HM-2B Series 2 Flute Ball Nose End Mill with Straight Shank for Hardened Steel Machining
ZCC-CT HM-2B 2 Flute Ball Nose End Mill with Straight Shank
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
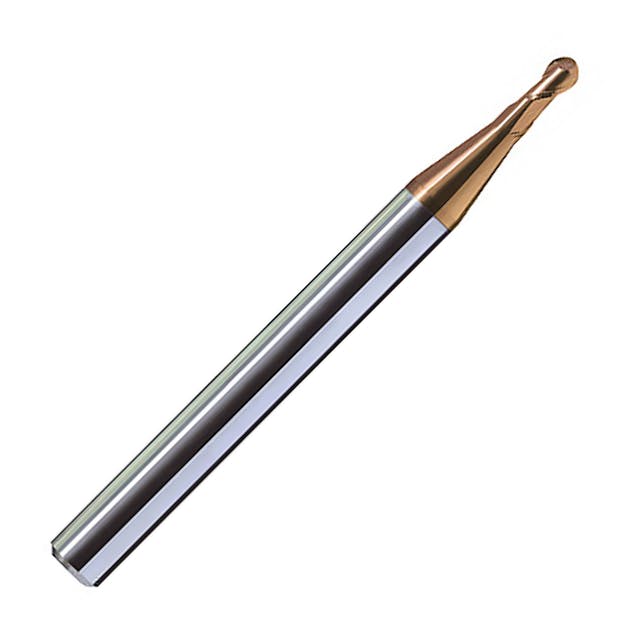
ZCC-CT HM Series 2 Flute Ball Nose Rib Processing Hardened Steel Milling Cutters
ZCC-CT HM-2BP 2 Flute Ball Nose Rib Processing Slot Drill
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
£21.79 excl. VAT
£26.15 incl. VAT
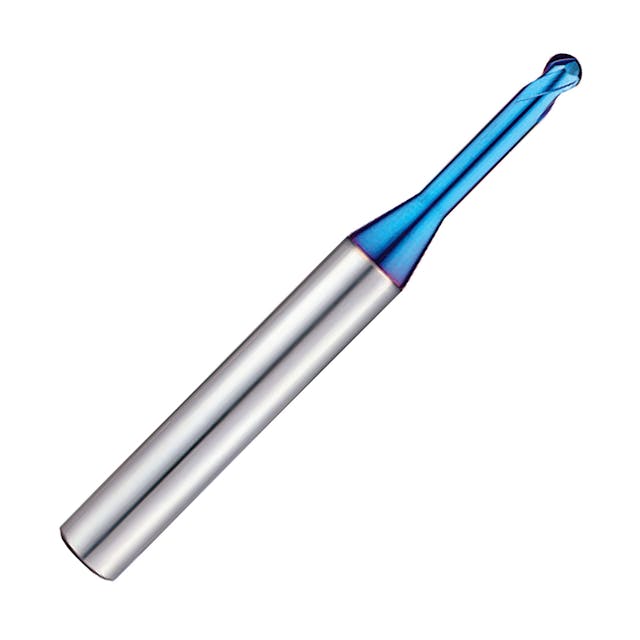
Pulsar Blue 2 Flute Rib Processing Ball Nose Slot Drill for Hardened Steel
Pulsar Blue 2 Flute Rib Processing Ball Nose Slot Drill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish

MasterMill VX Series 4 Flute High Performance Ball Nosed End Mill
MasterMill VX 170329 Series 4 Flute High Performance Ball Nosed End Mill
- Solid micrograin carbide
- Minimized tool deflection
- Reduced tool vibration
- Multi layer VX coated
- Variable helix geometry
- Suitable for high perfromance machining of Steel, Stainless steel, Titanium and nickel alloy

FRANKEN Top-Cut High Performance Ball Nosed End Mill
FRANKEN Top-Cut High Performance Ball Nosed End Mill
- Solid micrograin carbide
- TiALN coated
- Centre cutting
- Variable helix geometry
- Rough and finish with 1 tool
- Suitable for steel, stainless steel, cast iron, titanium and HRSA
£34.10 excl. VAT
£40.92 incl. VAT
£29.16excl. VAT
£34.99incl. VAT

ZCC-CT HM-4BL 4 Flute Ball Nose Long Shank for Hardened Steel
ZCC-CT HM-4BL 4 Flute Ball Nose End Mill with Long Straight Shank
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
£38.11 excl. VAT
£45.73 incl. VAT

ZCC-CT HM-4B 4 Flute Ball Nose End Mill for Hardened Steel
ZCC-CT HM-4B 4 Flute Ball Nose End Mill with Straight Shank
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
£32.54 excl. VAT
£39.05 incl. VAT
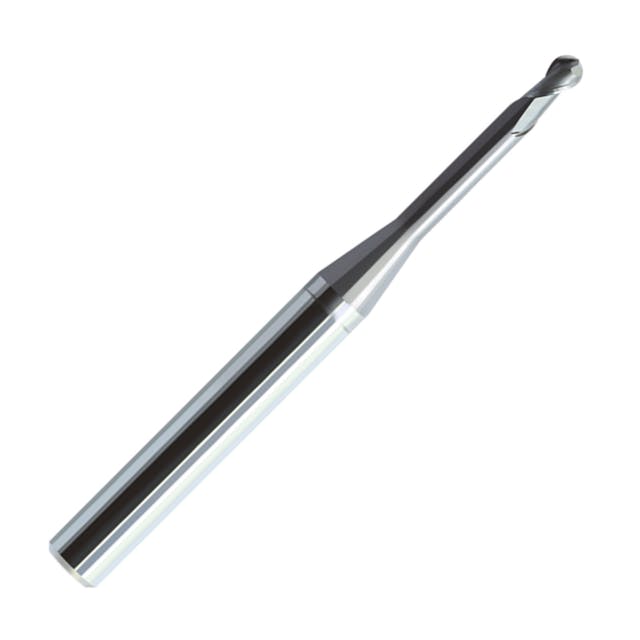
2 Flute CrN Coated Aluminium Ball Nose Rib Processing Micro Slot Drill
2 Flute CrN Coated Aluminium Ball Nose Rib Processing Micro Slot Drill
- For machining of Aluminiums, Copper, Brass and Bronze
- Excellent sharpness of cutting edge for very good surface quality
- CrN coating for improved tool life
- Sizes from 0.5mm-5mm
£20.11 excl. VAT
£24.13 incl. VAT
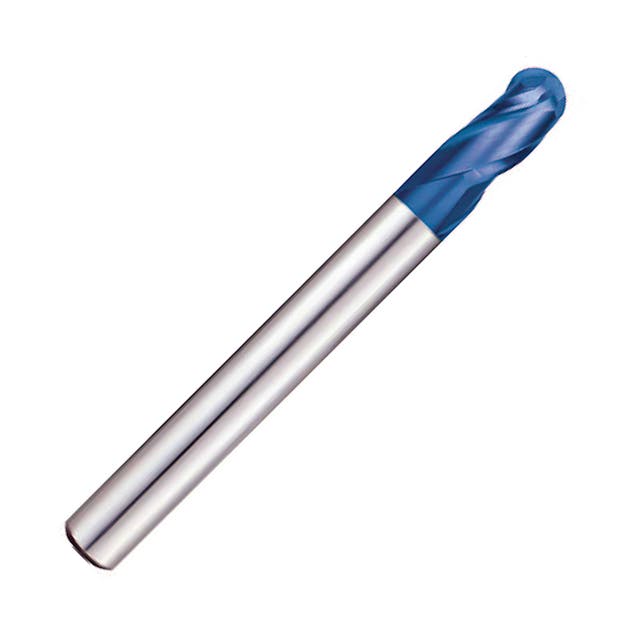
Pulsar Blue 3 Flute Ball Nose End Mill for Hardened Steel
Pulsar Blue 3 Flute Ball Nose End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
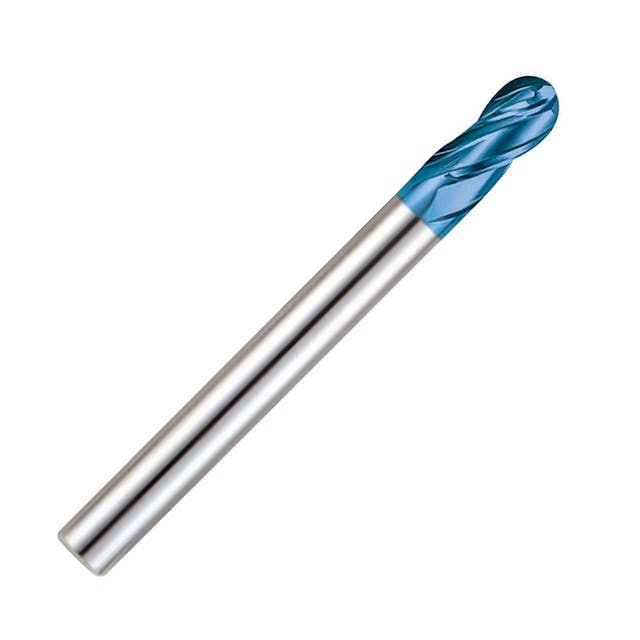
Pulsar Blue 4 Flute Ball Nose End Mill for Hardened Steel
Pulsar Blue 4 Flute Ball Nose End Mill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish

ZCC-CT TM-4BP Series 4 Flute KMS405 Coated Carbide Ball Nose Reduced Neck End Mill for Titanium & Heat-Resistant Alloy Machining
ZCC-CTÕs new TM range of high performance milling cutters for heat resistant super-alloys feature a revolutionary proprietary KMS405 coating for exceptional thermal stability and wear resistance.
£31.71 excl. VAT
£38.05 incl. VAT
£26.95excl. VAT
£32.34incl. VAT

ZCC-CT TM-4B Series 4 Flute KMS405 Coated Carbide Ball Nose End Mill for Titanium & Heat-Resistant Alloy Machining
ZCC-CTÕs new TM range of high performance milling cutters for heat resistant super-alloys feature a revolutionary proprietary KMS405 coating for exceptional thermal stability and wear resistance.
£27.02 excl. VAT
£32.42 incl. VAT
£22.97excl. VAT
£27.56incl. VAT

ZCC-CT TM-4BL Series 4 Flute KMS405 Coated Carbide Ball Nose Long Length End Mill for Titanium & Heat-Resistant Alloy Machining
ZCC-CTÕs new TM range of high performance milling cutters for heat resistant super-alloys feature a revolutionary proprietary KMS405 coating for exceptional thermal stability and wear resistance.
£28.52 excl. VAT
£34.22 incl. VAT
£24.24excl. VAT
£29.09incl. VAT

Clarkson 2 Flute HSS Co8 Weldon Shank Long Length Slot Drill
Clarkson 2 Flute HSS Co8 Weldon Shank Long Length Slot Drill
- HSS 8% cobalt
- Uncoated
- Weldon (flatted) shank
- Suitable for a wide range of materials

CLARKSON TiALN HSS Co8 2 Flute Long Length Ball Nose Slot Drill
CLARKSON TiALN HSS Co8 2 Flute Long Length Ball Nose Slot Drill
- HSS 8% cobalt
- TiALN coated
- Weldon (flatted) shank
- Suitable for a wide range of materials

ALU-XP 113202 2 Flute Extended Neck 50 Degree Helix Ball Nose Milling Cutter for Aluminium
ALU-XP 113202 2 Flute Extended Neck High Helix Ball Nose Milling Cutter for Aluminium
Suitable for high speed machining of aluminium and other non-ferrous materials.
Excellent surface finishes
Superior chip removal.
Neck relief.
Mirror polished flutes.

CLARKSON HSS Co8 4 Flute Ball Nose End Mill
CLARKSON HSS Co8 4 Flute Ball Nose End Mill
- HSS 8% cobalt
- Uncoated
- Weldon (flatted) shank
- Suitable for a wide range of materials
£23.88 excl. VAT
£28.66 incl. VAT
£35.56excl. VAT
£42.67incl. VAT

ZCC-CT TM-5B Series 5 Flute KMS405 Coated Carbide Ball Nose End Mill for Titanium & Heat-Resistant Alloy Machining
ZCC-CTÕs new TM range of high performance milling cutters for heat resistant super-alloys feature a revolutionary proprietary KMS405 coating for exceptional thermal stability and wear resistance.
£28.88 excl. VAT
£34.66 incl. VAT
£24.55excl. VAT
£29.46incl. VAT

ZCC-CT TM-5BL Series 5 Flute KMS405 Coated Carbide Ball Nose Long Length End Mill for Titanium & Heat-Resistant Alloy Machining
ZCC-CTÕs new TM range of high performance milling cutters for heat resistant super-alloys feature a revolutionary proprietary KMS405 coating for exceptional thermal stability and wear resistance.
£30.74 excl. VAT
£36.89 incl. VAT
£26.13excl. VAT
£31.36incl. VAT

ZCC-CT TM-5BP Series 5 Flute KMS405 Coated Carbide Ball Nose Reduced Neck End Mill for Titanium & Heat-Resistant Alloy Machining
ZCC-CTÕs new TM range of high performance milling cutters for heat resistant super-alloys feature a revolutionary proprietary KMS405 coating for exceptional thermal stability and wear resistance.
£34.01 excl. VAT
£40.81 incl. VAT
£28.91excl. VAT
£34.69incl. VAT
Frequently Asked Questions
A ball nose milling cutter (also called a ball end mill) is a solid carbide or HSS milling cutter with a hemispherical cutting tip.
The radius of the ball is exactly half the cutter's nominal diameter so a 10mm ball nose has a 5mm tip radius.
This rounded geometry allows the tool to machine curved surfaces, 3D contours, fillets, radii and complex profiles that flat-bottom end mills cannot produce.
Ball nose cutters are essential for 3D profiling, die & mould work plus any application requiring smooth, contoured surfaces.
Flat end mill / square end mill - has a flat bottom cutting face with sharp corners and is used for slotting, pocketing and machining flat floors and true 90° shoulders
Ball nose end mill - has a hemispherical tip and cannot produce a flat floor but excels at 3D surface machining, radii, fillets and scalloped profiling passes
For most 3D milling and contouring work, a ball nose is the correct choice.
For pocketing and flat-floor operations, a flat end mill or corner-radius end mill is more appropriate.
A corner radius end mill (sometimes called a bull nose or toroidal cutter) has a flat cutting face with a small radius blended into the corner and not a full hemisphere.
It combines the flat-floor capability of a square end mill with improved edge strength and a gentle radius.
A full ball nose produces the maximum possible radius equal to half the tool diameter.
Use a ball nose for 3D profiling and use a corner radius tool when you need flat floors with a small blended fillet or where edge strength on a flat-bottomed pocket is important.
2-flute ball nose - the most common ball nose option with the best chip evacuation, especially in pockets and deep cavities, most suitable for most materials & general-purpose profiling
3-flute ball nose - a good balance between chip clearance & rigidity, making them useful in materials where vibration or tool deflection is a concern
4-flute (and above) ball nose - improved rigidity and surface finish making them better suited to finishing passes where chip load per tooth is low. They have less chip clearance, so less suitable for slotting or deep pockets!
For most profiling and 3D surface finishing work, a 2-flute cutter is the standard starting point. Where surface quality is the priority on the finishing pass, 4-flute tools can improve results.
Our solid carbide ball nose range covers all common engineering materials:
Steel and alloy steel - general machining grades with AlTiN or TiAlN coatings
Stainless steel - requires sharp, positive-rake geometry and appropriate coatings to avoid work hardening
Aluminium and non-ferrous alloys - polished flutes, high helix geometry and ZrN or uncoated grades for clean chip evacuation and bright finish
Hardened steels (up to ~70 HRC) - specialist ultra-fine grain carbide with hard coatings for die and mould finishing
Titanium and HRSA - specific grades with high edge toughness and suitable coatings
Plastics, composites, and wood - sharp geometry, polished flutes and reduced coating for clean cutting without burr
Check the individual product listing for material suitability, coating type and recommended cutting data.
Coatings extend tool life which in turn allows higher cutting speeds and improves cutting performance in specific materials:
TiAlN / AlTiN - the most common general-purpose coating which offer high hardness, excellent heat resistance. Suitable for steel, stainless & cast iron
TiSiN / nACo / AlCrN - advanced coatings for hardened steels, high-speed dry machining & very hard materials
ZrN / TiN - lower hardness but excellent for non-ferrous metals (aluminium, copper, brass) where built-up edge is a concern
DLC (Diamond-Like Carbon) - extremely slippery coating for aluminium & soft non-ferrous which prevents sticking
Uncoated (bright) - occasionally used for very fine finishing in aluminium or where coating adhesion could affect surface quality
Flute length (cutting length) - determines the maximum depth of profile cut. You should select a flute length just sufficient for the required depth as excessive flute length beyond the cutting zone reduces tool rigidity and increases the risk of chatter and deflection
Overall length (OAL) - the total length of the cutter from tip to shank end. Longer tools reach deeper into pockets and cavities but are more prone to deflection. Always minimise the gauge length (stick-out from the collet) to maximise rigidity
Neck clearance - many long-reach ball nose cutters feature a reduced-diameter neck behind the cutting head, allowing deep cavity access while maintaining a full-diameter shank for rigidity in the collet.
The step-over determines the cusp height (scallop) left on the machined surface between adjacent tool passes.
The smaller the step-over relative to the tool radius, the finer the surface finish:
A step-over of 5–10% of tool diameter gives a very fine finish with minimal scallop height, this is used for high-quality die & mould surfaces
A step-over of 15–25% of tool diameter is typical for semi-finishing passes
A step-over of 30–50% is used for roughing or semi-roughing passes where finish quality is secondary
Calculate cusp height as: h = R − √(R² − (ae/2)²), where R is the ball radius and ae is the step-over.
At the very tip of a ball nose cutter, the cutting edge passes through the centreline of the tool (the point at which peripheral speed drops to zero).
This "dead zone" at the centre produces rubbing rather than cutting, which generates heat and can cause poor surface quality, especially at low tilt angles.
To avoid this you should:
Tilt the tool 10–15° in the CAM program so the effective cutting zone is slightly off-centre
Use a higher spindle speed to maintain adequate surface footage
Avoid plunging directly on the ball tip - use helical ramping or a roughing tool to pre-clear material before ball nose finishing
These refer to the ratio of overall length to diameter:
Short (stub) reach - maximum rigidity and is used where access allows. Best for high-speed finishing where deflection must be minimised
Standard reach - the most versatile option and is suitable for the majority of profiling & pocketing operations
Long reach - for deep cavities, pockets & moulds where standard length cannot reach the work
Extra-long / extended neck - specialist tools for very deep cavities with reduced neck diameter behind the cutting head allows deep access while retaining a full shank in the holder
Always use the shortest tool that reaches the feature as every extra mm of overhang reduces rigidity and increases the risk of chatter!
Technically yes, but it is not ideal!
The hemispherical geometry produces a rounded slot floor rather than a flat one and chip evacuation in a full-width slot can be challenging.
For full-width slotting a flat-bottom end mill is preferable. Ball nose cutters can be used for profiling slots with curved floors (e.g. in cams and guides) or where the rounded floor geometry is acceptable.