Threading Tools
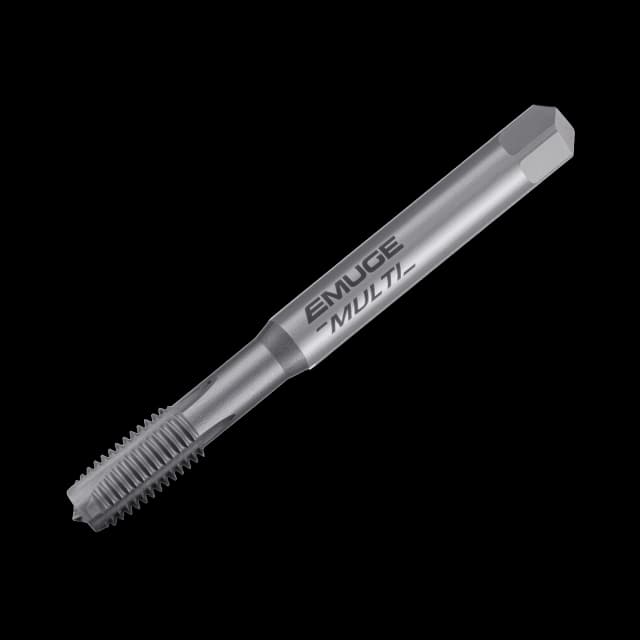
Emuge Metric Coarse Spiral Point Multi Tap NT2 Coated Stainless Steel
The EMUGE Multi-tap is the original all purpose tapping solution for nearly all materials.
- NT2 is oxidised to stop cold welding
- Multi purpose tap to machine steels,stainless steel,cast iron, aluminium and non-ferrous materials
- Attractive price-performance ratio
max. 3 x d1
£17.20 excl. VAT
£20.64 incl. VAT
£14.85excl. VAT
£17.82incl. VAT
Emuge Metric Coarse Spiral Flute Multi Tap NE2 Coated
The EMUGE Multi-tap is the original all purpose tapping solution for nearly all materials.
- NE2 is oxidised to stop cold welding
- Multi purpose tap to machine steels,stainless steel,cast iron, aluminium and non-ferrous materials
- Attractive price-performance ratio
max. 2.5 x d1
£17.00 excl. VAT
£20.40 incl. VAT
£15.30excl. VAT
£18.36incl. VAT
Metric Coarse Machine Taps Spiral Flute
- Bright Finish
- General Purpose Tap For A Wide Range Of Materials
- HSSE
- Metric Coarse
- Spiral Flute
NEUWERK Metric Coarse Machine Taps Spiral Flute HSSE H40TM Series for General Purpose
The H40TM series machine tap from NEUWERK is our 1st choice tap for general purpose high performance threading of steel, cast iron, aluminium and copper. It has a Titanium Nitride coating providing long tool life.
NEUWERK are a leading European manufacturer of high quality machine taps providing high performance and reliability
£14.40 excl. VAT
£17.28 incl. VAT
£8.47excl. VAT
£10.16incl. VAT
Emuge Metric Coarse Spiral Point Multi Tap GLT-1 Coated Stainless Steel
The EMUGE Multi-tap is the original all purpose tapping solution for nearly all materials.
- GLT1 is a Multi layered coating which has a hard smooth surface
- Tremendous increase in tool life and superior swarf evacuation
- High performance tap to machine steels, stainless steel, duplex,cast iron, aluminium and non-ferrous materials
- Attractive price-performance ratio
max. 3 x d1
£21.80 excl. VAT
£26.16 incl. VAT
£18.90excl. VAT
£22.68incl. VAT
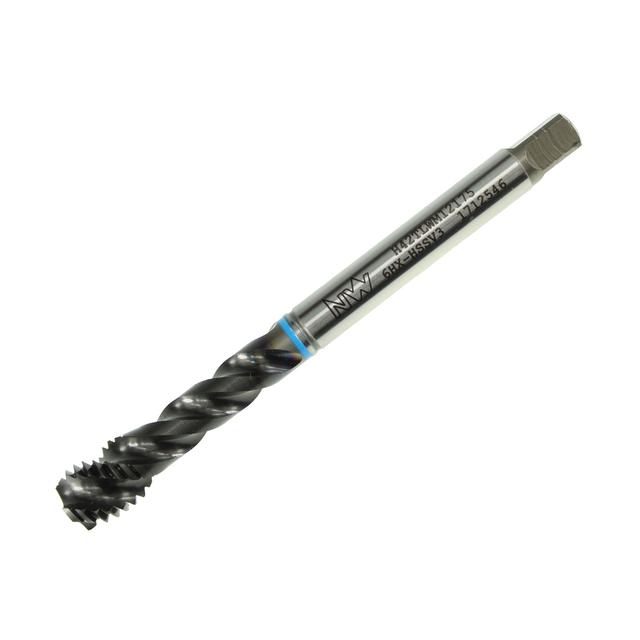
NEUWERK Metric Coarse Machine Tap Spiral Flute HSSV3 H42TLWM Series for Stainless Steel
The H42TLWM series machine tap from NEUWERK is our 1st choice tap for high performance threading of stainless steel, carbon steel and tempered steel. It is made from Vanadium Cobalt Substrate with a TiN Alox coating which provides long tool life.
NEUWERK are a leading European manufacturer of high quality machine taps providing high performance and reliability
£18.46 excl. VAT
£22.15 incl. VAT
£9.96excl. VAT
£11.95incl. VAT
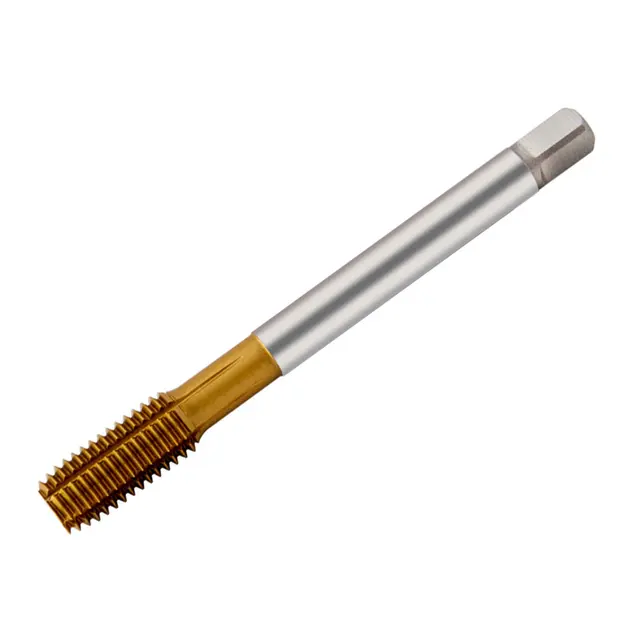
Osborn Metric Coarse Roll Taps
- Tin Coated
- General Purpose Tap For A Wide Range Of Materials
- HSSE
- Metric Coarse
- With Oil Grooves
£12.79 excl. VAT
£15.35 incl. VAT
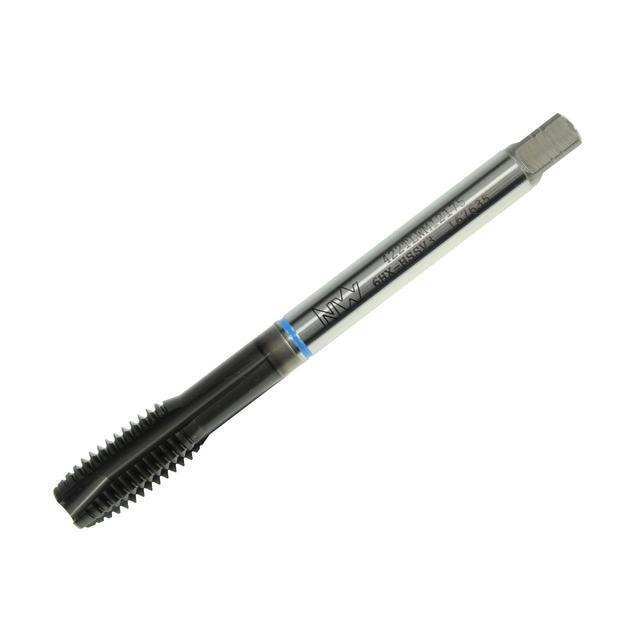
NEUWERK Metric Coarse Machine Tap Spiral Point HSSV3 422TLWM Series for Stainless Steel
The 422TLWM series machine tap from NEUWERK is our 1st choice tap for high performance threading of stainless steel, carbon steel and tempered steel. It is made from Vanadium Cobalt Substrate with a TiN Alox coating providing long tool life.
NEUWERK are a leading European manufacturer of high quality machine taps providing high performance and reliability
£18.46 excl. VAT
£22.15 incl. VAT
£17.23excl. VAT
£20.68incl. VAT
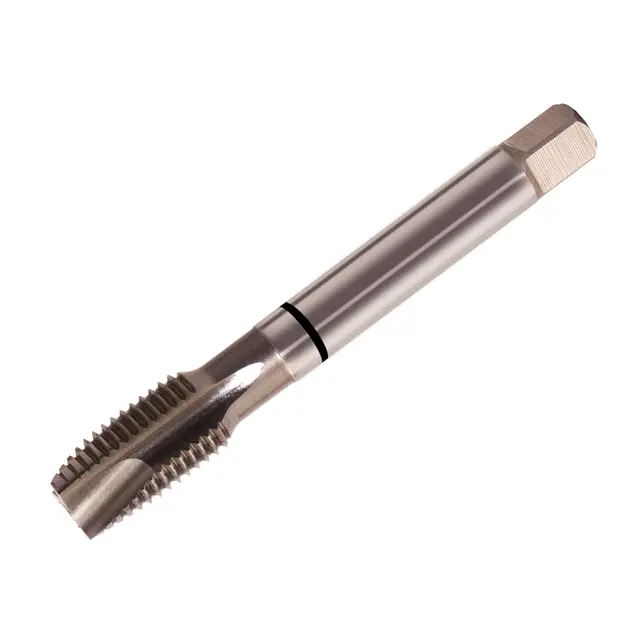
Metric Coarse Machine Taps Spiral Point
- Bright Finish
- General Purpose Tap For A Wide Range Of Materials
- HSSE
- Metric Coarse
- Spiral Point
Emuge Whitworth Spiral Flute Multi Tap NE2 Coated
The EMUGE Multi-tap is the original all purpose tapping solution for nearly all materials.
- NE2 is oxidised to stop cold welding
- Multi purpose tap to machine steels,stainless steel,cast iron, aluminium and non-ferrous materials
- Attractive price-performance ratio
max. 2.5 x d1
£38.20 excl. VAT
£45.84 incl. VAT
£33.03excl. VAT
£39.64incl. VAT
NEUWERK Metric Coarse Machine Tap Spiral Point HSSE 420TM Series for General Purpose
The 420TM series machine tap from NEUWERK is our 1st choice tap for general purpose high performance threading of steel, cast iron, aluminium and copper. It has a Titanium Nitride coating providing long tool life.
NEUWERK are a leading European manufacturer of high quality machine taps providing high performance and reliability
£14.40 excl. VAT
£17.28 incl. VAT
£9.01excl. VAT
£10.81incl. VAT
£51.04 excl. VAT
£61.25 incl. VAT
Emuge Unified Coarse Thread Spiral Flute Multi Tap NE2 Coated
The EMUGE Multi-tap is the original all purpose tapping solution for nearly all materials.
- NE2 is oxidised to stop cold welding
- Multi purpose tap to machine steels,stainless steel,cast iron, aluminium and non-ferrous materials
- Attractive price-performance ratio
max. 2.5 x d1
£22.30 excl. VAT
£26.76 incl. VAT
£19.26excl. VAT
£23.11incl. VAT
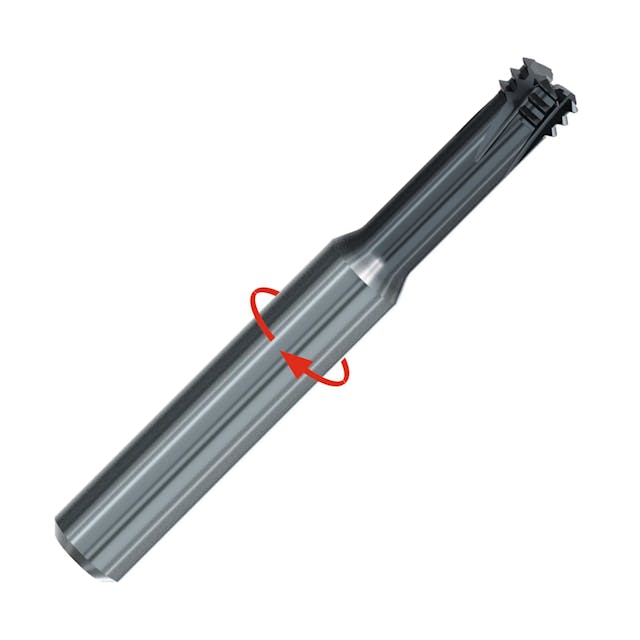
Emuge Franken Metric Drill Thread Mill 2xD
Emuge Franken solid carbide circular drill thread mill
- Drill, thread mill and chamfer with 1 tool
- Speed up cycle times and reduce tooling cost with 1 tool
- Suitable for steel, stainless steel, cast iron, heat resistant super alloys and non-ferrous materials
- 2xD
- Metric thread
Emuge Franken UNC Drill Thread Mill 2xD
Emuge Franken solid carbide circular drill thread mill
- Drill, thread mill and chamfer with 1 tool
- Speed up cycle times and reduce tooling cost with 1 tool
- Suitable for steel, stainless steel, cast iron, heat resistant super alloys and non-ferrous materials
- 2xD
- UNC thread
Emuge Franken UNF Drill Thread Mill 2xD
Emuge Franken solid carbide circular drill thread mill
- Drill, thread mill and chamfer with 1 tool
- Speed up cycle times and reduce tooling cost with 1 tool
- Suitable for steel, stainless steel, cast iron, heat resistant super alloys and non-ferrous materials
- 2xD
- UNF thread
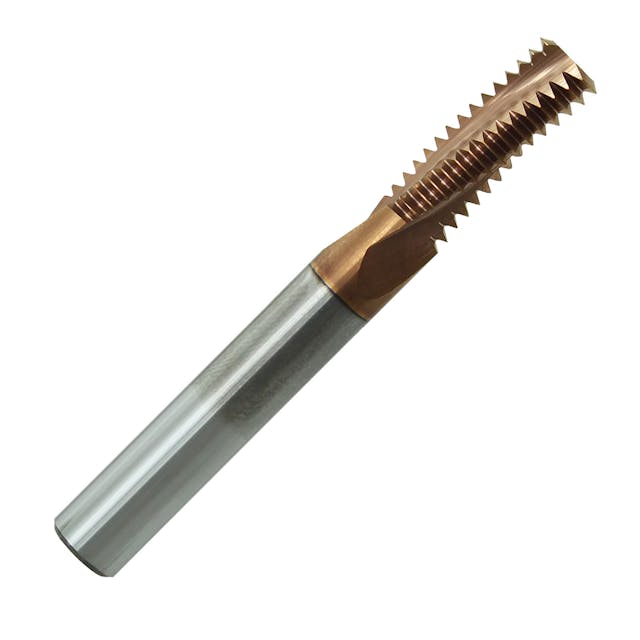
Coated Carbide Metric Coarse Internal Thread Mills BY STARKE
- Solid carbide
- TISIN coated to machine up to 60 HRC
- 2XD minimum flute length
- Standard metric coarse
- Sizes available: M3 to M16
£55.47 excl. VAT
£66.56 incl. VAT
£38.42excl. VAT
£46.10incl. VAT
Emuge Metric Coarse Thread Multi Circular Thread Mill
Solid carbide circular thread mill
- For machining of internal threads
- 2XD
- From thread size M1
- Pre-drilled taphole necessary
- Tool for several dimensions with corrected thread profile
- Partly independant of pitch
£117.08 excl. VAT
£140.50 incl. VAT
Emuge Unified Coarse Thread Spiral Point Multi Tap NT2 Coated
The EMUGE Multi-tap is the original all purpose tapping solution for nearly all materials.
- NT2 is oxidised to stop cold welding
- Multi purpose tap to machine steels,stainless steel,cast iron, aluminium and non-ferrous materials
- Attractive price-performance ratio
max. 3 x d1
£21.70 excl. VAT
£26.04 incl. VAT
£18.81excl. VAT
£22.57incl. VAT
Emuge Metric Coarse Spiral Point Multi Tap NT2 Coated
The EMUGE Multi-tap is the original all purpose tapping solution for nearly all materials.
- NT2 is oxidised to stop cold welding
- Multi purpose tap to machine steels,stainless steel,cast iron, aluminium and non-ferrous materials
- Attractive price-performance ratio
max 2 x d1
£15.20 excl. VAT
£18.24 incl. VAT
£13.14excl. VAT
£15.77incl. VAT
Emuge Metric Coarse Spiral Point Multi Cold Forming Tap GLT-1 Coated
The EMUGE Multi-tap is the original all purpose tapping solution for nearly all materials.
- GLT1 is a Multi layered coating which has a hard smooth surface
- Tremendous increase in tool life and superior swarf evacuation
- High performance tap to machine steels, stainless steel, duplex,cast iron, aluminium and non-ferrous materials
- Attractive price-performance ratio
max. 3 x d1
£25.80 excl. VAT
£30.96 incl. VAT
£22.32excl. VAT
£26.78incl. VAT
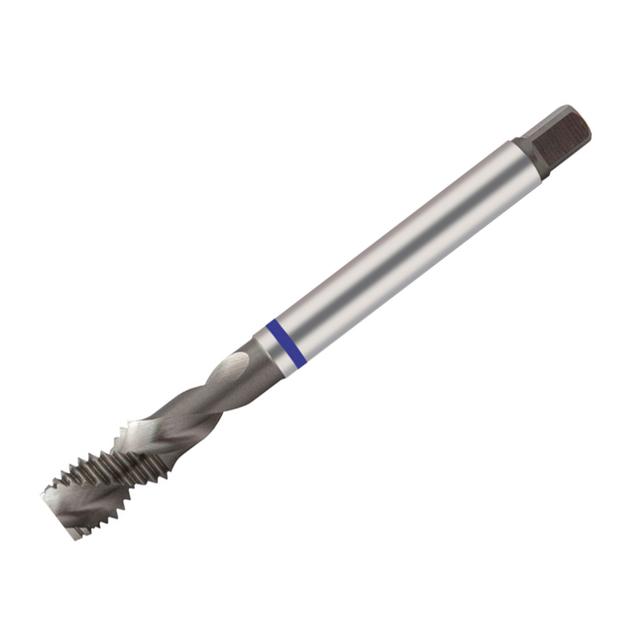
Metric Coarse HSSE Spiral Flute Machine Tap for Aluminium - Osborn
- The Blue Ring HSSE machine tap is our first choice for aluminium and aluminium alloys
- The 45° helix angle ensures excellent chip evacuation
- Metric Coarse (MC) thread form
- Spiral Flute
- Sizes available M2 to M20
£7.27 excl. VAT
£8.72 incl. VAT
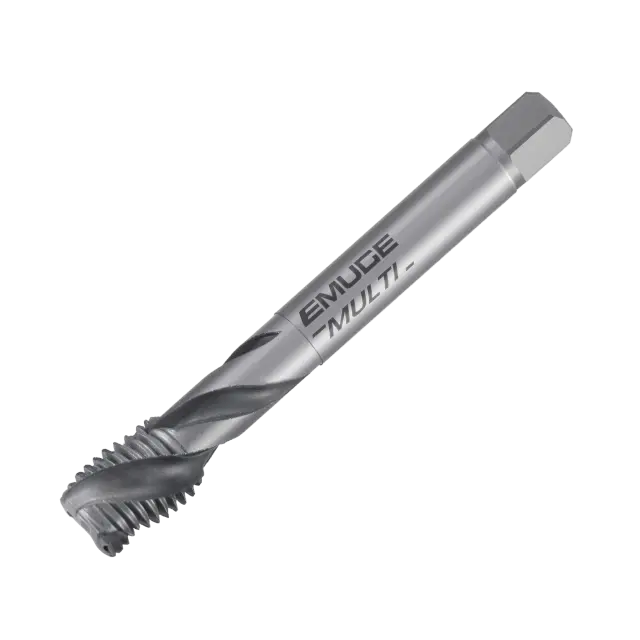
Emuge Metric Fine Spiral Flute Multi Tap NE2 Coated
The EMUGE Multi-tap is the original all purpose tapping solution for nearly all materials.
- NE2 is oxidised to stop cold welding
- Multi purpose tap to machine steels,stainless steel,cast iron, aluminium and non-ferrous materials
- Attractive price-performance ratio
max. 2.5 x d1
£30.60 excl. VAT
£36.72 incl. VAT
£26.46excl. VAT
£31.75incl. VAT
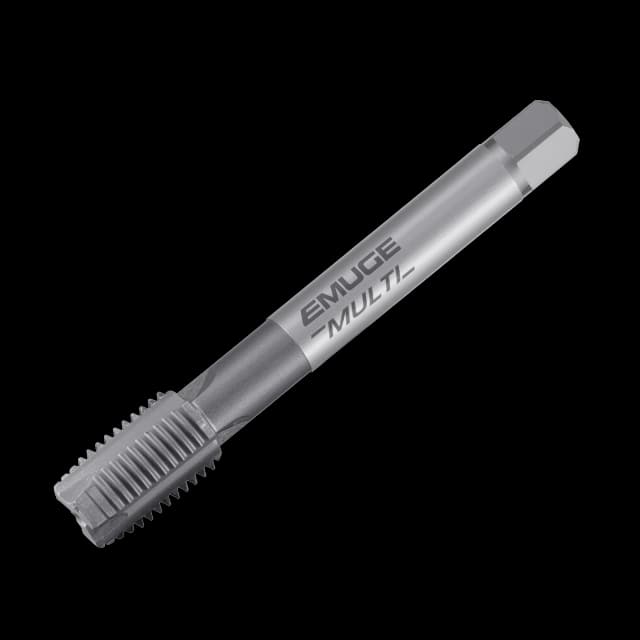
Emuge Whitworth Spiral Point Multi Tap NT2 Coated Stainless Steel
The EMUGE Multi-tap is the original all purpose tapping solution for nearly all materials.
- NT2 is oxidised to stop cold welding
- Multi purpose tap to machine steels,stainless steel,cast iron, aluminium and non-ferrous materials
- Attractive price-performance ratio
max. 3 x d1
£36.80 excl. VAT
£44.16 incl. VAT
£31.86excl. VAT
£38.23incl. VAT
Frequently Asked Questions
The Threading section covers five product groups:
Machine Taps: for CNC and production tapping operations
Hand Taps: for manual and bench work
Thread Mills: for CNC helical interpolation threading
Threading Inserts: for lathe turning of external and internal threads
Threading Holders: toolholders required to present threading inserts correctly to the workpiece.
The range covers all commonly used thread standards in UK engineering:
Metric Coarse (MC / ISO): the standard for the majority of modern engineering work in the UK and Europe. The most widely stocked form across all product types.
Metric Fine (MF): a finer pitch than coarse for the same nominal diameter. Used where higher clamping loads are needed for a given thread diameter, in thin-walled components and in precision adjustments where a finer pitch provides better resolution. Available in both taps and threading inserts.
Unified Coarse (UNC) & Unified Fine (UNF): the standard for American-designed equipment and parts manufactured to ANSI/ASME specifications. Covered in machine taps, thread mills and threading inserts.
Whitworth (G / BSW / BSP): the British Standard Whitworth and parallel pipe thread forms. Still widely used for hydraulic and pneumatic fittings and legacy machinery. Available in taps and threading inserts.
BSPT: British Standard Pipe Taper, the UK tapered pipe thread used in plumbing and fluid power connections. Covered in threading inserts.
ACME & Stub ACME: trapezoidal thread forms used for lead screws, power transmission and valve stems. Threading inserts only.
Trapezoidal: the metric equivalent of ACME commonly used in European lead screws and linear actuators. Threading inserts only.
NPT — American tapered pipe thread. Thread mill and threading inserts available.
Tap diameters range from M2 through to M30 in metric and from No. 4 through to 1" in UNC/UNF.
The distinction comes down to how chip evacuation is managed during the tapping cycle.
Hand Taps are the traditional three-tap sets used for manual threading taper (first cut), second cut (plug/intermediate) and plug (bottom/finishing). The taper tap starts the thread with a gradual entry over 8 to 10 threads and the second and plug taps progressively deepen the thread. When tapping manually the user periodically reverses the tap to break and clear chips, a technique that works well but is too slow and inconsistent for production use. The hand taps in the range are Osborn metric coarse bottoming lead taps.
Machine Taps are designed to cut or form threads in a single-pass operation under power in CNC machining centres and lathes, tapping heads and rigid-cycle drilling machines. They are engineered to handle chip evacuation continuously rather than relying on reversal.
Machine taps are differentiated primarily by their geometry which determines how they deal with chips:
Spiral Point (Gun) Taps: push chips forward ahead of the tap into the hole below the thread. This geometry is only suitable for through holes as the chips must have somewhere to go. It is the most common geometry for CNC through-hole tapping because chip control is positive and reliable.
Spiral Flute Taps: have helical flutes that pull chips upward and out of the hole behind the tap and away from the cutting zone. This geometry is for blind holes where the bottom of the hole stops the chips from passing through. The spiral flute action is critical in blind-hole tapping as without it chips pack at the bottom of the hole and either break the tap or strip the newly cut thread.
Roll Taps (Cold Forming): do not cut at all! They plastically deform and flow the workpiece material to form the thread profile without producing chips. This requires a ductile workpiece (steel, stainless steel, aluminium, brass) and a slightly different (larger) pre-drill hole diameter than for cut tapping. The advantages are no chips to evacuate, very strong thread (the material is work-hardened and fibres run with the thread rather than being cut across) and longer tool life.
Four machine tap sub-categories are stocked:
General Purpose Machine Taps: cover the everyday requirement for tapping steel, cast iron, aluminium and non-ferrous metals in standard production environments. Both Osborn and Neuwerk brands are available. The finish on most taps in this category is steam tempered (a blue-black iron oxide finish that reduces friction slightly and resists built-up edge on the tap flanks).
High Performance Universal Machine Taps: (from Emuge-Franken) are the premium tier, designed to run at higher cutting speeds and in more demanding applications. These taps use the GLT-1 coating, a multi-layer PVD coating (Gold Layer Technology) that significantly reduces friction, increases surface hardness and maintains a stable cutting edge at elevated temperatures. GLT-1 coated taps are substantially more durable in tough materials and in high-volume production compared to steam-tempered taps.
Machine Taps for Stainless Steel: are specifically geometrised and coated for austenitic and duplex stainless steels which work-harden rapidly. Standard tap geometry in stainless steel quickly generates heat and causes the material to harden ahead of the cutting edge, seizing the tap. Stainless-specific taps use a sharper cutting edge geometry, specific helix angles to reduce torque, and coatings optimised for low-friction cutting in sticky materials.
Machine Taps for Aluminium: use a high helix angle and polished flutes to prevent aluminium from adhering to the tap as aluminium welding (cold pressure welding) to the tap face is the most common cause of tap breakage in aluminium. The specific geometry also minimises the tendency of aluminium to tear rather than cut cleanly.
A thread mill is a multi-tooth solid carbide rotary tool that machines a thread by moving in a helical path around the inside (or outside) of a hole using CNC circular interpolation. Unlike a tap which is committed to a specific thread pitch and diameter as soon as it enters the hole, a thread mill can produce any thread diameter within its reach by adjusting the programmed circular interpolation radius and one thread mill can produce multiple different diameters of the same pitch.
Thread mills are the preferred choice when:
The workpiece is hardened or very hard. Thread mills in the range are rated for steel, stainless steel, cast iron and heat-resistant super alloys as these are materials where tap breakage risk is high. A broken tap in a hardened workpiece is almost always scrap, a broken thread mill can often be extracted without destroying the part.
The thread is large. For threads M10 and above a thread mill and a standard solid carbide drill of the correct pre-drill diameter is more economical than a large tap, particularly if thread depth is less than 2xD.
A blind hole needs a thread that runs to the very bottom. A tap requires a certain amount of lead-in length and cannot always thread right to the bottom of a blind hole. A thread mill programmed correctly can produce a full thread very close to the bottom.
A single tool needs to serve multiple diameters. By adjusting the CNC interpolation radius one thread mill covers a range of diameters for the same pitch.
When to stick with a tap over a thread mill: for high-volume production of small threads (M2–M6) in softer materials, tapping is faster and lower-cost per hole. Thread milling has a longer cycle time than tapping because of the interpolation path required.