

2 Flute Milling Cutters / 2 Flute Slot Drills
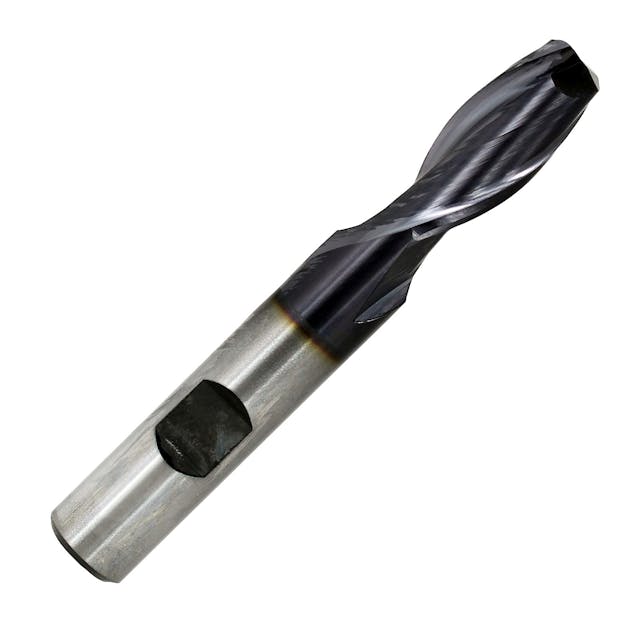
HSC Series 2 Flute Tialn Coated HSS Milling Cutters
- 2 flute HSSE slot drill
- HSS 8% Cobalt gives improved tool life and performance in comparison to conventional HSS
- 1st choice for economical machining
- TIALN coated for increased tool life
£10.01 excl. VAT
£12.01 incl. VAT
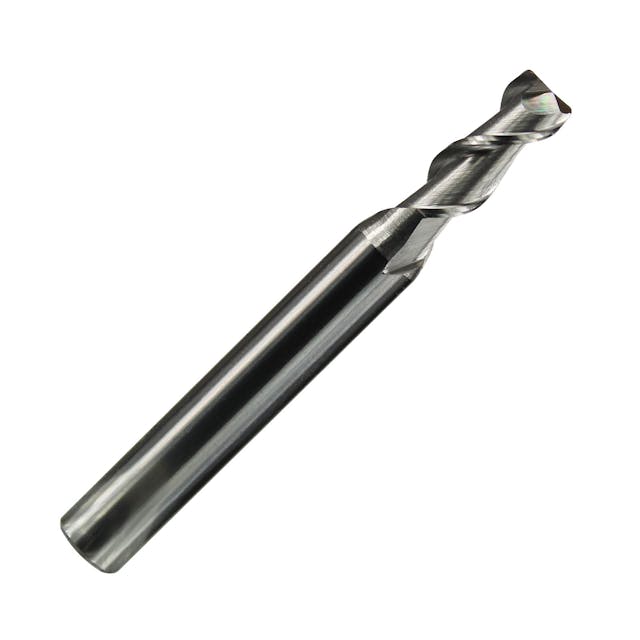
Ali-Mill 2 Flute 45 Degree Carbide Slot Drills for Aluminium
ALI-MILL Solid Carbide 2 Flute 45 Degree Slot Drill from STÄRKE is 1st choice for machining aluminium and non ferrous material.
Polished flutes for superior surface finish.
The special Hi-Helix geometry enables better chip removal.
Micrograin carbide
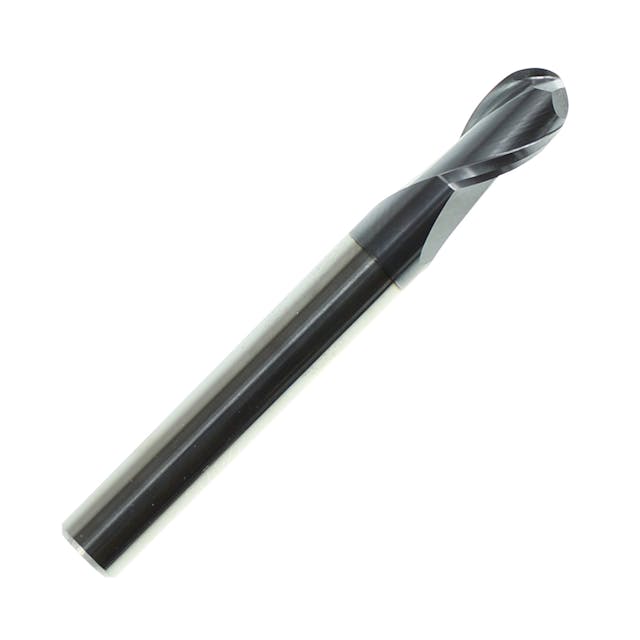
Eco-Mill 2 Flute Coated Carbide Ball Nose Slot Drills
ECO-MILL coated carbide 2 flute ball nosed slot drill from STÄRKE, a TiALN coated general purpose cutter.
- Suitable for cutting steel, stainless steel, cast iron and non-ferrous materials including aluminium alloys and copper.
- Cut up to 45 HRC
- Can be used wet or dry to increase tool life.
- Micrograin carbide
- Available diameter sizes between 1mm and 20mm


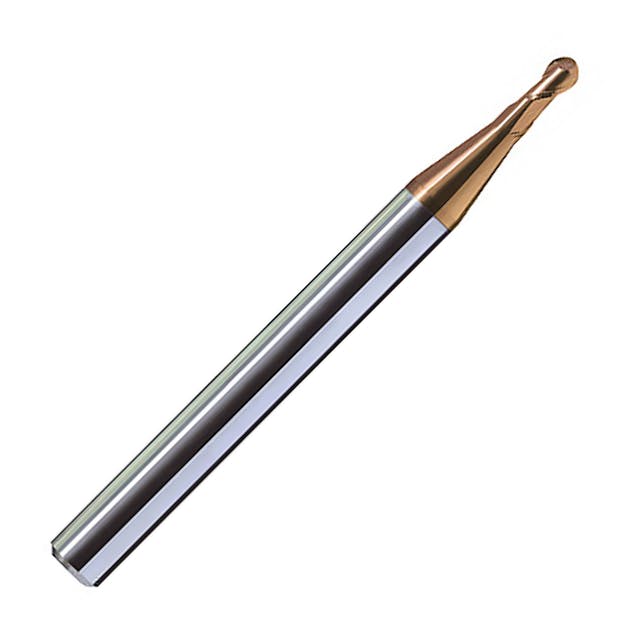
ZCC-CT HM Series 2 Flute Ball Nose Rib Processing Hardened Steel Milling Cutters
ZCC-CT HM-2BP 2 Flute Ball Nose Rib Processing Slot Drill
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
£21.79 excl. VAT
£26.15 incl. VAT
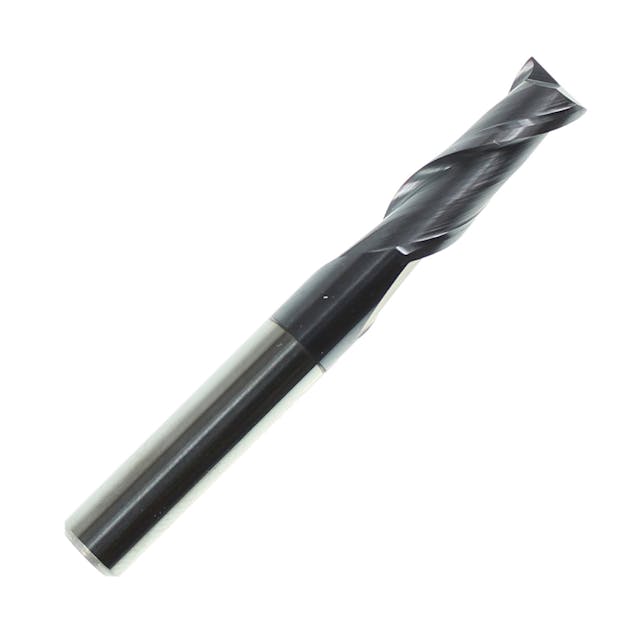
Eco-Mill 2 Flute Coated Solid Carbide Slot Drill
ECO-MILL Coated Carbide 2 Flute End Mill from STÄRKE is a TiALN coated general purpose cutter.
- Suitable for cutting steel, stainless steel, cast iron and non-ferrous material including cast aluminium and copper.
- Cut up to 45 HRC
- Can be used wet or dry to increase tool life.
- Micrograin carbide
- Centre cutting
- Available diameter sizes between 1mm to 20mm
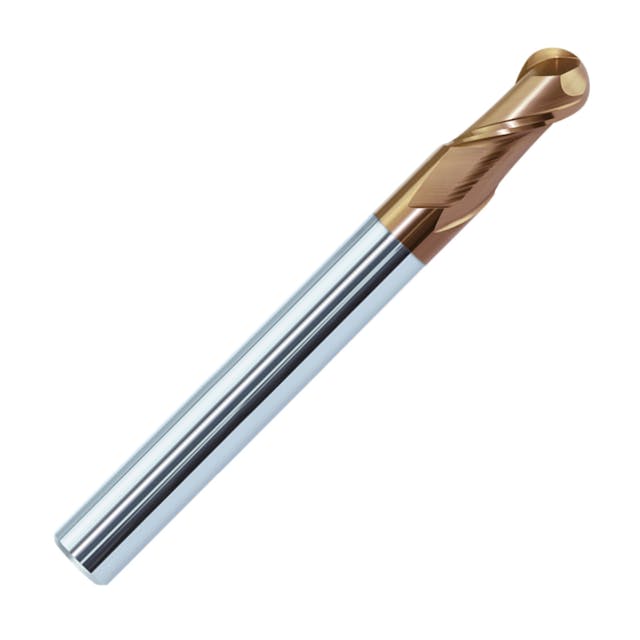
ZCC-CT HM-2BL Series 2 Flute Long Length Ball Nose Slot Drill for Hardened Steel Machining
ZCC-CT 2 Flute Long Length Ball Nose Slot Drill
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
£38.11 excl. VAT
£45.73 incl. VAT
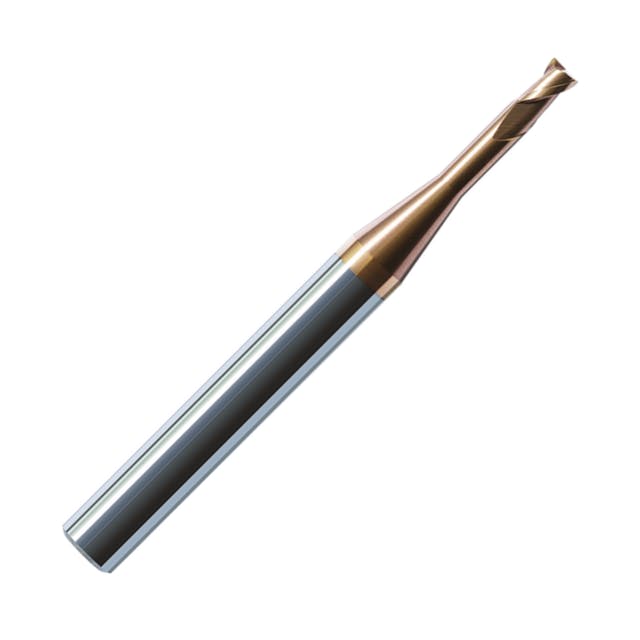
ZCC-CT HM-2EP 2 Flute Slot End Mill with Short Cutting Edge and Long Neck for Hardened Steel
ZCC-CT HM-2EP 2 Flute Slot End Mill with Short Cutting Edge and Long Neck
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
£19.74 excl. VAT
£23.69 incl. VAT
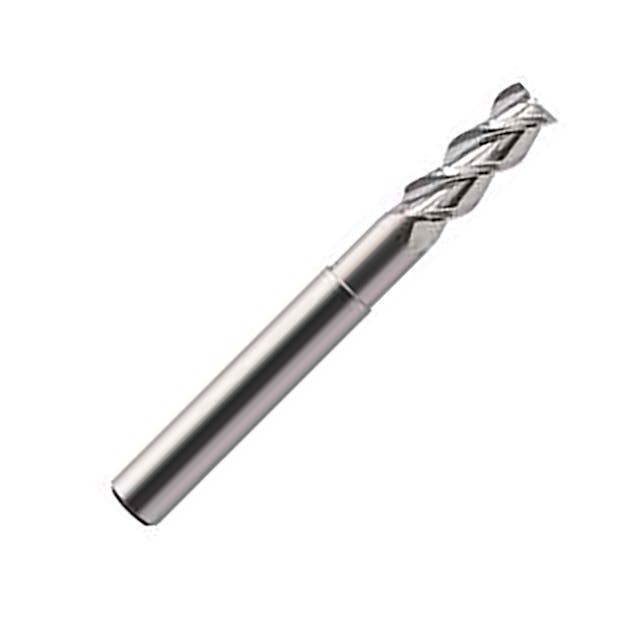
2 Flute Carbide Reduced Neck End Mill for Aluminium
- Excellent surface finishes.
- Superior chip removal
- Micrograin solid carbide substrate
- Mirror polished Flutes
- Suitable for high speed machining of aluminium and other non-ferrous materials
- Corner protected.
- Long series
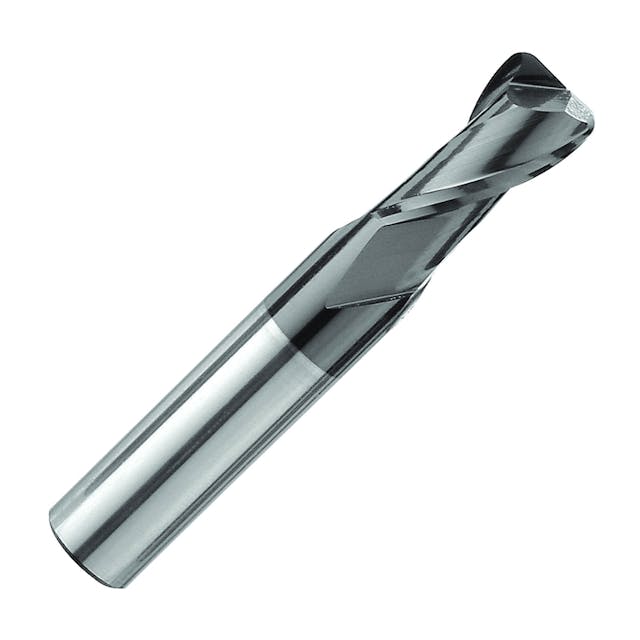
NANO-MILL Max-Mill JNR Series Coated Carbide 2 Flute Corner Radius End Mill
Max-Mill Coated Carbide 2 Flute Corner Radius End Mill from Nano-Mill is a general purpose cutter, ideal for cutting carbon steel, high speed steel, stainless steel, alloy, inconel and titanium. MAX-MILL cutters cut up to 55 HRC, and can be used wet or dry to increase tool life.
£9.94 excl. VAT
£11.93 incl. VAT
£12.33excl. VAT
£14.80incl. VAT
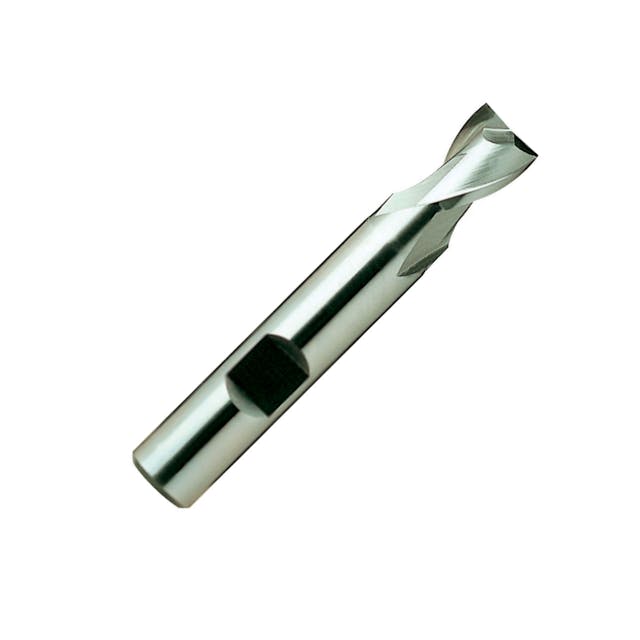
Clarkson 2 Flute HSS Co8 Weldon Shank Short Length Slot Drill
Clarkson 2 Flute HSS Co8 Weldon Shank Short Length Slot Drill
- HSS 8% cobalt
- Uncoated
- Weldon shank
- Suitable for a wide range of materials
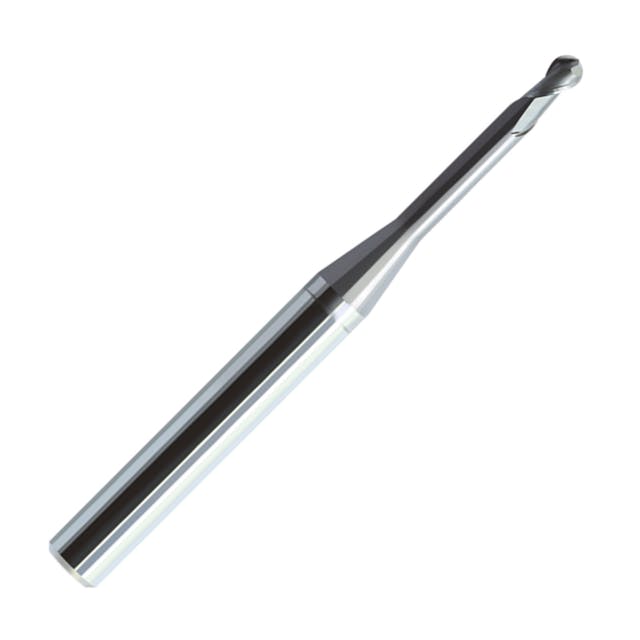
2 Flute CrN Coated Aluminium Ball Nose Rib Processing Micro Slot Drill
2 Flute CrN Coated Aluminium Ball Nose Rib Processing Micro Slot Drill
- For machining of Aluminiums, Copper, Brass and Bronze
- Excellent sharpness of cutting edge for very good surface quality
- CrN coating for improved tool life
- Sizes from 0.5mm-5mm
£20.11 excl. VAT
£24.13 incl. VAT
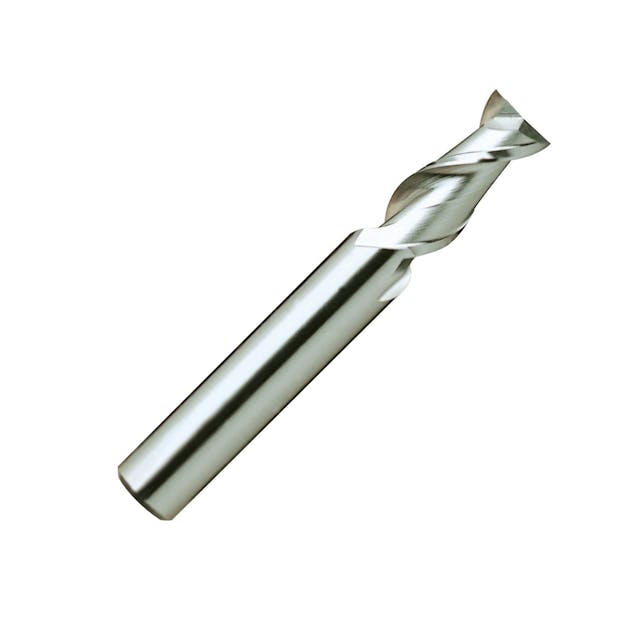
Alu-XP 2 Flute Carbide Slot Drill for Aluminium
Alu-XP 2 Flute Carbide Slot Drill for Aluminium
- Excellent surface finishes.
- Superior chip removal
- Micrograin solid carbide substrate
- Mirror polished Flutes
- Suitable for high speed machining of aluminium and other non-ferrous materials
- Corner protected.
£12.50 excl. VAT
£15.00 incl. VAT
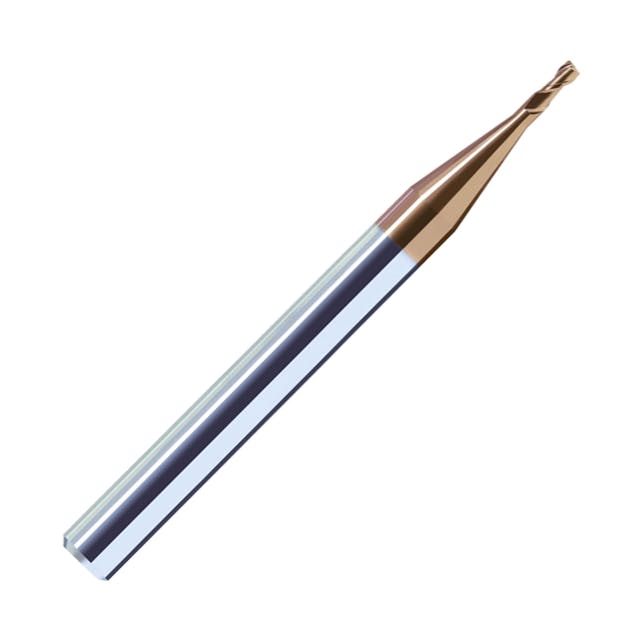
ZCC-CT HM-2ES Series 2 Flute Micro Diameter End Mill with Straight Shank for Hardened Steel Machining
ZCC-CT HM-2ES 2 Flute Micro Diameter End Mill with Straight Shank
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
- Starting at 0.3mm diameter
£12.31 excl. VAT
£14.77 incl. VAT
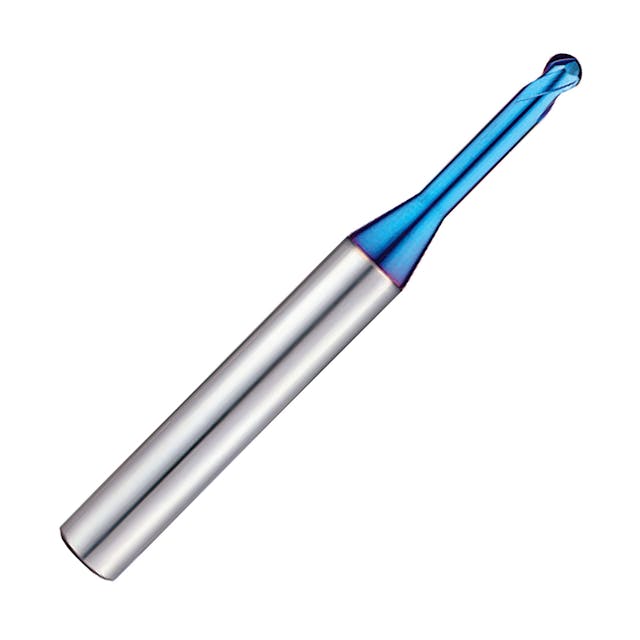
Pulsar Blue 2 Flute Rib Processing Ball Nose Slot Drill for Hardened Steel
Pulsar Blue 2 Flute Rib Processing Ball Nose Slot Drill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
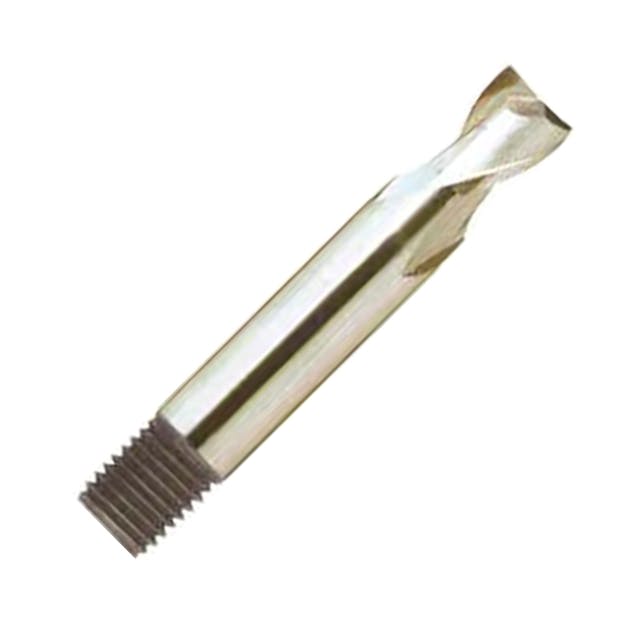
CLARKSON HSS Co8 2 Flute Threaded Shank Slot Drill
CLARKSON HSS Co8 2 Flute Threaded Shank Slot Drill
- HSS 8% cobalt
- Uncoated
- Threaded shank
- Suitable for a wide range of materials
£7.11 excl. VAT
£8.53 incl. VAT
£6.84excl. VAT
£8.21incl. VAT
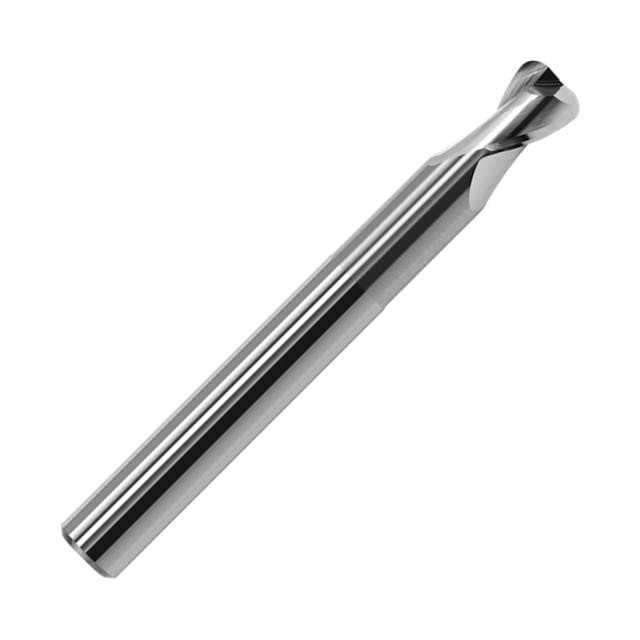
2 Flute Corner Radius Long Length End Mill for Aluminium
2 Flute Corner Radius Long Length End Mill for Aluminium
- Newly developed geometry
- New KMD401 diamond like coating for significantly improved tool life
- Wide range of radii available on larger diameters
£45.15 excl. VAT
£54.18 incl. VAT
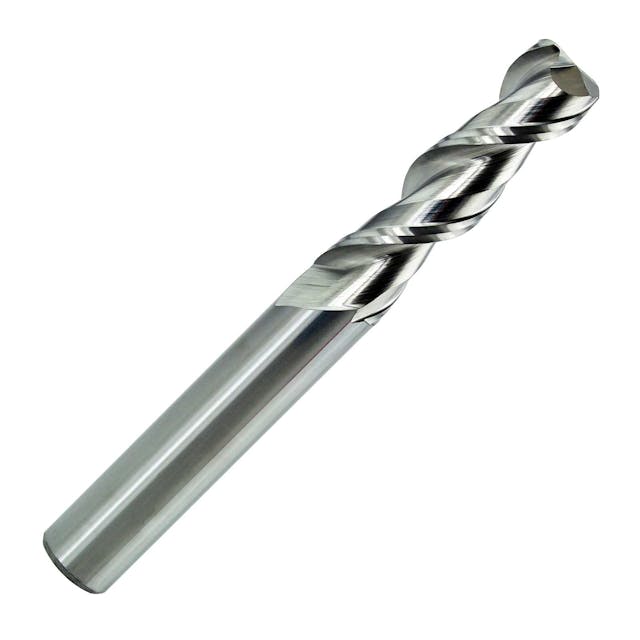
2 Flute Long Series carbide Slot Drill for Aluminium (STARKE Ali-Mill)
- Suitable for machining of aluminium and other non-ferrous materials.
- Mirror polished fl utes
- Excellent surface finishes, superior chip removal.
- Micrograin carbide
- Hi-helix geometry
- Sizes available: 3mm, 4mm, 6mm, 8mm, 10mm, 12mm, 16mm, 20mm
£9.81 excl. VAT
£11.77 incl. VAT
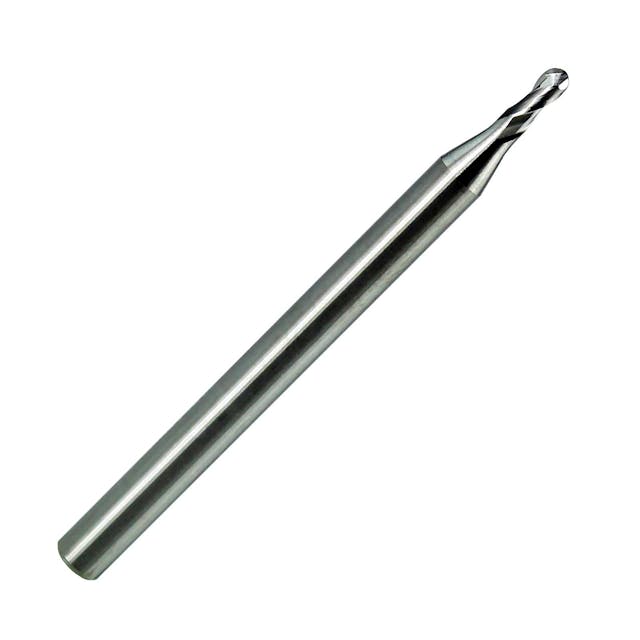
Ali-Mill 2 Flute Ball Nosed Solid Carbide for Aluminium
- Solid micrograin carbide
- 38 degree helix geometry enable better chip removal
- Polished flutes for superior surface finish
- 2 flutes
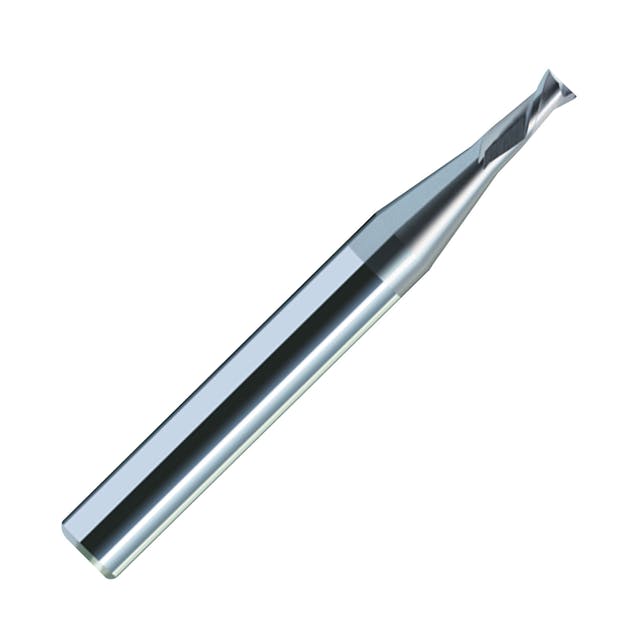
2 Flute Coated Aluminium Rib Processing Micro Slot Drill
2 Flute Coated Aluminium Rib Processing Micro Slot Drill
- For machining of Aluminiums, Copper, Brass and Bronze
- Excellent sharpness of cutting edge for very good surface quality
- CrN coating for improved tool life
- Sizes from 0.5mm-5mm
£17.68 excl. VAT
£21.22 incl. VAT
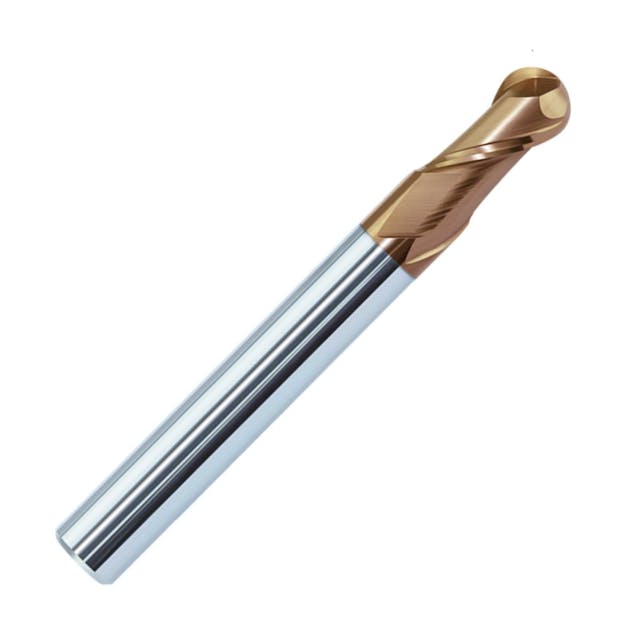
ZCC-CT HM-2B Series 2 Flute Ball Nose End Mill with Straight Shank for Hardened Steel Machining
ZCC-CT HM-2B 2 Flute Ball Nose End Mill with Straight Shank
- Excellent tool design covers large chip pocket, good stability and machining efficiency
- Optimized cutting geometry (Rake angle) assures edge stabitlity and sharpness
- Ultra fine grain carbide
- KMG555 Nano-ALTiN coating base for hard machining at high temperatures
- For machining upto 68HRC
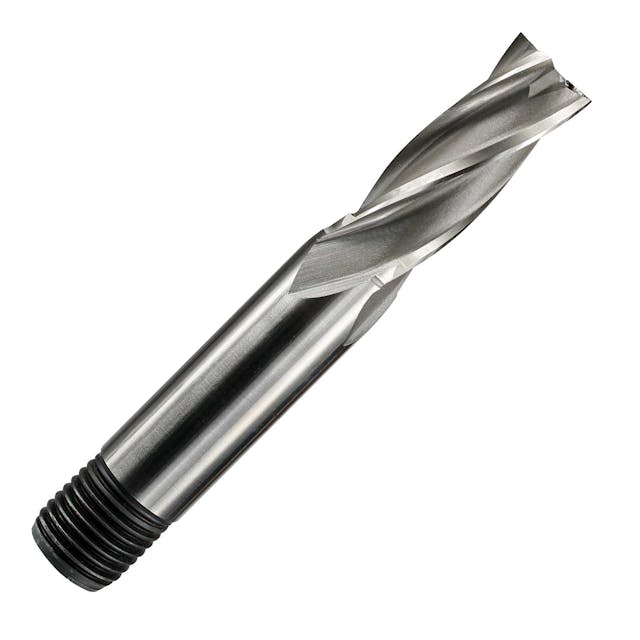
CLARKSON HSS Co8 Threaded Shank End Mill
CLARKSON HSS Co8 Threaded Shank End Mill
- HSS 8% cobalt
- Uncoated
- Threaded shank
- Suitable for a wide range of materials
£7.11 excl. VAT
£8.53 incl. VAT
£9.04excl. VAT
£10.85incl. VAT
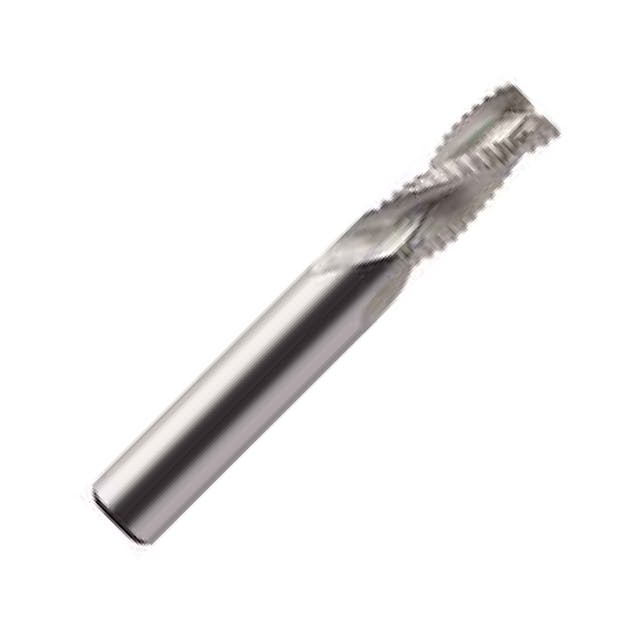
Alu-XP 3 Flute Long Length Weldon Shank Ripper
Alu-XP 3 Flute Long Length Weldon Shank Ripper
- Excellent surface finishes.
- Superior chip removal.
- Flatted shank.
- Micrograin solid carbide substrate.
- Corner protected.
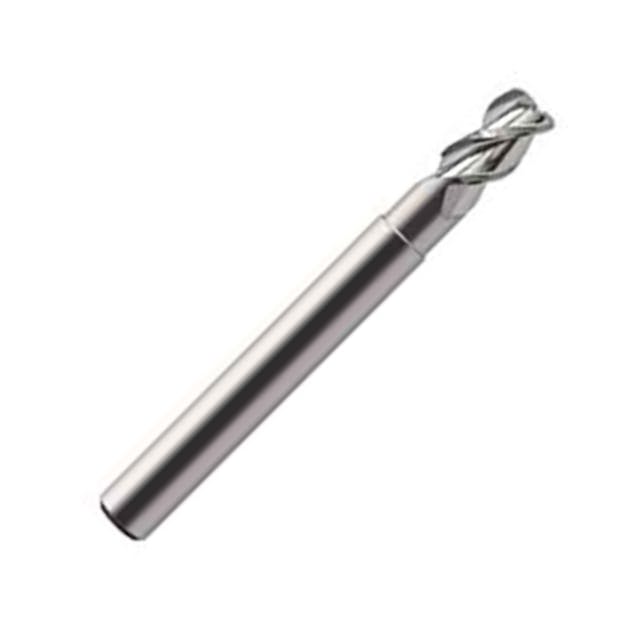
Alu-XP 156303 Series 2 Flute Carbide Corner Radius Reduced Neck End Mill for Aluminium & Non-Ferrous Machining
Alu-XP tools with Òmirror polishedÓ flutes allow for smooth chip evacuation, giving better surface finish and wear resistance. Cutting edges are optimised to minimise vibration, and 3-flute tools have a tight diameter tolerance giving excellent process reliability.
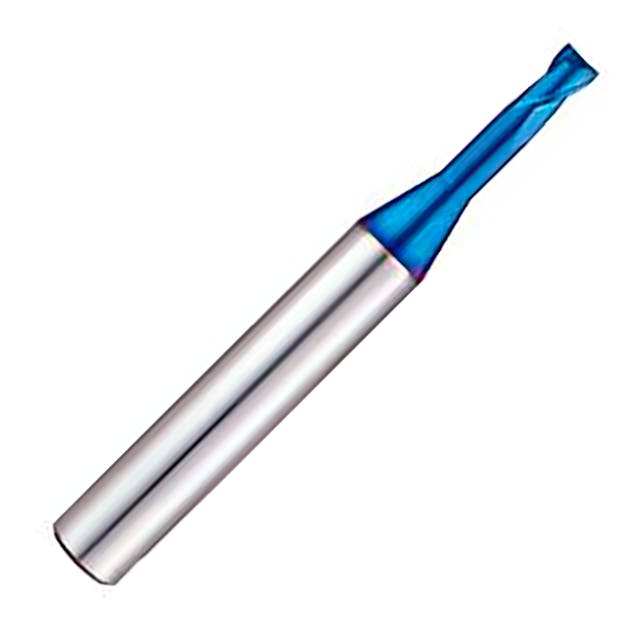
Pulsar Blue 2 Flute Rib Processing Slot Drill for Hardened Steel
Pulsar Blue 2 Flute Rib Processing Slot Drill for Hardened Steel
- Premium nanograin carbide
- Suitable for dry cutting
- Suitable for machining upto 70HRC
- High speed cutting
- 30 degree helix
- Excellent workpiece finish
Frequently Asked Questions
A 2-flute slot drill (end mill) is a solid carbide or HSS end mill with two cutting edges (flutes).
The 2-flute design is characterised by:
Larger chip gullets: two flutes leave more space between them than 3 flute or 4 flute tools and this larger chip clearance volume is the defining functional advantage of the 2-flute geometry
Centre-cutting capability : the majority of 2-flute slot drills are centre-cutting where one flute passes through or very close to the centre of the tool, allowing the cutter to plunge directly into solid material (like a drill) without a pre-drilled entry hole
Lower cutting forces per flute: with only two edges engaged, the radial force on the workpiece and spindle is lower per flute compared to a 3 flute cutter or 4 flute cutter.
Primary applications include:
Slot milling: cutting full-width slots from solid which is the defining application. The 2-flute geometry is the traditional and correct choice for full-slot cutting
Pocketing: ramping, helical interpolation or plunging into solid material and milling out a pocket - the centre-cutting geometry allows this without a pilot hole
Aluminium and non-ferrous materials: the large chip gullets are essential when milling soft, ductile materials that produce large, stringy chips. A 4 flute tool will pack chips in aluminium; a 2-flute tool will not!
Plastics, composites& soft materials: same chip clearance reasoning as aluminium.
Three end profiles are available, each suited to different machined feature types:
Square (Flat End)
Flat cutting face with sharp 90° corners - the most common profile
Produces square-bottomed slots, pockets, shoulders & steps
Use for any feature requiring a flat floor and sharp internal corners
Ball Nose
Hemispherical tip; creates a curved profile in the cut
The 2-flute ball nose is the standard choice for 3D work in softer materials and for micro-detail features
Use for 3D contouring and surfacing of sculptured surfaces, corner radii in pockets, profiling complex geometry, die/mould work or ramp entry into materials
Corner Radius (Bull Nose)
Flat end face with a small radius ground on the corner (rather than a sharp 90° edge)
Available in a range of corner radii, check the product listing for the specific radius options within each series
Use for: profiling where a defined radius is required at the base of a wall, strengthening the tool corner compared to a square end (the radius distributes stress and increases corner life), semi-finishing passes or reducing stress concentration in machined features
Shank diameters available across the range include 4mm, 5mm, 6mm, 8mm, 10mm, 12mm, 14mm, 15mm, 16mm, 18mm, 20mm & 25mm.
For standard-diameter cutters (≥6mm) the shank diameter typically equals the cutter diameter, for example a 10mm cutter has a 10mm shank.
For reduced neck cutters and sub-6mm cutters a larger shank (4mm or 6mm) carries a smaller cutter diameter providing rigidity and ease of holding in a standard collet without requiring ultra-small collets for the smallest diameters.
Toolholding note: For 4mm and 6mm shank cutters an ER16 or ER25 collet chuck is the standard holder. For 10–20mm shank cutters use an ER32 or ER40 collet chuck or an end mill holder if Weldon-flat shanks are present.
Yes they can provided the tool is centre-cutting. A centre-cutting 2-flute slot drill has one flute that passes through or very close to the centre of the tool face, enabling it to cut material at the very centre of the tool and plunge directly into solid stock like a drill.
Most 2-flute slot drills in this range are centre-cutting, however:
Ball nose cutters with a true hemispherical profile cut to the centre of the ball. They can plunge, but more effectively ramp or helically interpolate (more aggressive chip formation at the centre of a ball nose at zero surface speed)
Plunge rate should be limited as even a centre-cutting end mill is not as efficient at plunging as a dedicated drill - use a moderate feed rate and ensure adequate chip clearance.
Best practice for pocketing: Rather than straight plunging, use a helical interpolation entry (circular path with gradual Z-descent) or a ramp entry (straight inclined path). Both strategies produce better chip control and reduce axial load on the cutter compared to straight plunge.