

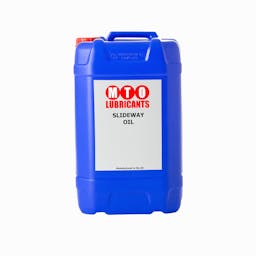
MTO Slideway 150 Oils
Series: SW0150£92.00 excl. VAT
£110.40 incl. VAT
MTO Slideway Oil is high quality machine tool lubricants available in various viscosities.
Application
Use as received for the lubrication of slideways at the manufacturers recommended viscosity. Also suitable for use where machines have a combined hydraulic and tableway system, for carriages, guides and headstocks, and as a gearbox oil where the tackiness additives may offer improved oil film strength.
Benefits
- Enhanced anti-wear and anti-corrosion properties
- Excellent slideway lubricity for smooth, stick free operation
| SKU | Size / Size | Price (Ex VAT) |
|---|---|---|
| SW0150-205L | 205 ltr | £929.33 |
| SW0150-20L | 20 ltr | £92.00 |
Frequently Asked Questions
A slideway is the precision-ground bearing surface on which a machine tool's moving elements (the table, saddle, cross-slide, quill or column) travel. The quality of the lubrication on these surfaces directly determines positioning accuracy, surface finish of the workpiece and the long-term condition of the machine.
Slideways operate under a lubrication regime that is fundamentally different from most other lubricated surfaces in a machine. The surfaces are broad, flat and relatively slow-moving (conditions that make maintaining a consistent hydrodynamic oil film difficult). Under light loads at low speeds, there is a tendency for the moving element to periodically break away and re-stick as it traverses, a behaviour known as stick-slip. Stick-slip produces non-linear motion so instead of a smooth, continuous traverse, the table advances in small, irregular jerks. This directly translates to chatter marks, dimensional variation and poor surface finish on the workpiece.
A dedicated slideway oil prevents stick-slip through a specific formulation that general-purpose metal working lubricants and hydraulic oils do not replicate. It contains friction modifiers, additives that alter the friction coefficient between the surfaces in a specific way. Unlike most anti-wear additives which aim to minimise friction uniformly, slideway friction modifiers are designed to produce a higher coefficient of friction when the surface is stationary (static friction) than when it is moving (kinetic friction). This inverted relationship (more resistance to initial movement than to continued movement) is what eliminates the stick-slip cycle. It is sometimes described as "anti-stick-slip" additive chemistry, and it is the defining requirement that separates a true slideway oil from any other lubricant.
A general hydraulic oil or engine oil used in place of slideway oil will not provide this friction characteristic, will allow stick-slip to develop, and will produce inferior surface finish on the workpiece.
ISO VG stands for ISO Viscosity Grade, the international standard (ISO 3448) that classifies lubricating oils by their kinematic viscosity at 40°C. The grade number is the midpoint of a viscosity range in centistokes (cSt). ISO VG 32 has a midpoint viscosity of 32 cSt at 40°C (range approximately 28.8-35.2 cSt). ISO VG 68 has a midpoint of 68 cSt (range approximately 61.2-74.8 cSt). ISO VG 150 has a midpoint of 150 cSt (range approximately 135–165 cSt).
Three viscosity grades are available in this category:
ISO VG 32 (SW0032): the thinnest oil in our range. Suitable for high-speed, lightly-loaded slideways or for machines where the machine manufacturer specifies a low-viscosity slideway oil.
ISO VG 68 (SW0068): the most common grade for general-purpose machine tool slideways. The majority of manual and CNC lathes, milling machines and machining centres specify ISO VG 68 for their tableway lubrication systems.
ISO VG 150 (SW0150): the heaviest grade, for slow-moving or heavily-loaded slideways, or for larger machines where the manufacturer specifies a higher-viscosity way oil.
Always check the machine manufacturer's specification before selecting a grade. The machine handbook or lubrication chart will state the required ISO VG or equivalent specification.
Stick-slip is a cyclical motion phenomenon that occurs on lubricated flat surfaces under light loads at low traverse speeds. The mechanics are as follows: when the slideway is stationary a boundary layer of oil separates the two surfaces, but the static friction force between them is relatively high. When the machine attempts to move the table, the driving mechanism (leadscrew or ballscrew) builds up elastic force against the static friction. Eventually, the static friction is overcome and the table breaks free suddenly (it "slips."). The table then moves a small distance, the driving force drops below the kinetic friction level, the table stops again and re-sticks and the cycle repeats. The frequency and amplitude of the stick-slip cycle depends on the slideway geometry, the lubricant, the load and the traverse speed.
The effects on machining are immediate and measurable as surface finish on the workpiece degrades, producing regular chatter marks or waviness corresponding to the stick-slip frequency. Dimensional accuracy deteriorates, since the table is not traversing linearly. Positioning repeatability worsens which is particularly damaging for CNC operations relying on accurate axis positioning.
Over time if the slideway is run without adequate lubrication or with the wrong lubricant type, the consequences are more serious. The repeated micro-welds and break-free events of stick-slip produce accelerated wear on the slideway surfaces. Precision-scraped or ground slideways that should last the life of the machine can be worn to the point of requiring regrinding or replacement within a few years of inadequate lubrication. Regrinding or replacing a worn slideway on a precision machine tool is a major, expensive engineering operation.
Millway is Millers Oils' dedicated slideway oil range. Millers Oils is a UK-based lubricant manufacturer with a long-established reputation in motorsport and industrial lubrication. The Millway range adds several additional formulation features beyond the standard MTO slideway specification:
The most distinctive is a tacky adhesive additive - a polymer additive that gives the oil a slightly stringy, adhesive character. When you withdraw a finger or probe from a container of Millway, the oil forms threads rather than breaking cleanly. This tackiness is not simply a sensory property: it means the oil clings to surfaces more tenaciously than a non-tacky oil. On vertical slideway surfaces — the type found on the vertical column and quill of a milling machine, or the vertical slideways of a jig borer whereas a non-tacky oil will drain away under gravity between lubrication cycles. A tacky oil resists this draining and maintains a continuous film for longer between applications. Millway is described specifically as "highly suitable for the lubrication of vertical surfaces" as a result of this property.
Yes you can! Both the MTO Slideway range and Millway are explicitly described as suitable for machines with a combined hydraulic and tableway system. These are machines (common in older manual lathes and knee mills) where a single oil reservoir and pump circuit provides oil both to the hydraulic control system (if fitted) and to the slideway lubrication passages. In these designs, a single grade of oil must satisfy both the hydraulic system's requirements (viscosity stability, anti-wear properties, compatibility with seals) and the slideway requirements (friction modification, tackiness, anti-corrosion).
For machines with combined systems, the ISO VG 68 grade is the most common specification because it sits within the hydraulic system's required viscosity range while also providing adequate film thickness for slideway lubrication. Always verify against the machine manufacturer's specification: some older machines specify ISO VG 32 for a combined hydraulic/slideway circuit; some larger machines may specify ISO VG 68 for ways and a separate hydraulic oil for the hydraulic system.
On machines with a separate way lube system and a separate hydraulic system, do not mix oil types or fill the wrong reservoir with the wrong product. Slideway oil in a pure hydraulic system (without slideway lubrication requirements) will still function as a hydraulic fluid but the friction modifier additives are unnecessary whereas hydraulic oil in a dedicated slideway circuit will cause stick-slip.
Both MTO Slideway and Millway can be used as a gearbox oil where the tackiness additives may offer improved oil film strength. This means slideway oils can be used in enclosed gearboxes (typically the feed gearbox on a lathe or the knee elevation gearbox on a milling machine) where the manufacturer specifies a compatible viscosity grade and where the tackiness additives will not cause foaming or seal incompatibility.
This dual-use capability is practically useful on older manual machine tools (particularly manual lathes) where the gearbox, headstock and way lubrication may all share a single type of oil and where the machine handbook calls for a "way oil" or "machine oil" throughout. Using a single product for multiple applications on these machines simplifies the consumables inventory.
This does not mean slideway oil is a general-purpose gear oil: it is not formulated with the extreme pressure (EP) additives required for automotive gearboxes, worm gears or hypoid gears. It is appropriate only where the machine manufacturer's specification aligns with a non-EP machine tool oil of the correct viscosity.
With slideway oils, replenishment intervals depend heavily on the machine type, the lubrication system design and the intensity of use.
Machines with automatic centralised lubrication systems (common on CNC machining centres and larger manual machines) oil the slideways on a timed cycle (often every few minutes during operation). These systems have an oil reservoir that requires topping up periodically (the machine's operation manual will state the reservoir capacity and recommend a check frequency). A reservoir that drops below its minimum level will reduce oiling frequency and lead to dry-running. On machines with centralised systems, checking the reservoir at the start of each shift and topping up as required is standard practice.
Machines with manual oiling (where the operator applies oil by hand to the slideway oiling points using an oil can) should be oiled at the start of each working period and on heavy-use days, at each break. The oiling points are typically marked on the machine and direct oil to the slideway surfaces via internal passages.
The signs of inadequate slideway lubrication are:
Stick-slip: the table or slide movement becomes jerky or irregular, particularly at slow feeds. (This is the earliest and most obvious symptom)
Increased resistance to manual table traverse (on machines with handwheels): the table feels stiff or notchy rather than smooth
Unusual noise from the slideway: squeaking or scraping sounds during traverse
Deteriorating surface finish on the workpiece: regular feed marks or waviness that was not previously present.
If any of these symptoms appear, lubrication should be checked and restored before continuing machining. Continuing to run a machine with inadequate slideway lubrication causes accelerating wear and will require progressively more expensive remediation.
This is an important practical concern in workshop environments. Cutting fluid contamination of slideway oil is a common occurrence, particularly on manual machines where coolant splashes onto the slideway surfaces or enters through poorly-sealed oiling passages.
Water-based cutting fluid (the most common type in use) will contaminate slideway oil in two ways:
It dilutes the oil's viscosity and lubricating properties
It introduces water that promotes corrosion of the slideway surfaces.
The anti-corrosion additives in both the MTO Slideway and Millway products provide some protection against incidental water contact, but they are not designed to handle sustained emulsification with water-based coolant.
If cutting fluid contamination is suspected the slideway oiling system should be drained, flushed with a small quantity of fresh oil and refilled. Continuing to use a contaminated oil means reduced lubrication effectiveness and accelerated surface corrosion.
To minimise contamination risk: maintain slideway wipers in good condition (the rubber or felt wiper elements at the leading and trailing edges of the table that sweep the slideway clean before the bearing surfaces engage), keep coolant flow directed at the cutting zone rather than at the machine table and avoid flooding the table with coolant when it is not necessary.
Millway's tacky adhesive additive offers a secondary benefit here. On machines where coolant contact with the slideways is unavoidable the more tenacious film left by a tacky oil is harder to displace than a non-tacky oil, providing marginally better protection against coolant wash-off between oiling cycles.
Customers Also Viewed
ex VAT
ex VAT
ex VAT
ex VAT
ex VAT
ex VAT
Service & Delivery Information
If the order is placed online, we offer free shipping to mainland UK on orders over £25 ex VAT.
This offer excludes certain items due to weight restrictions. These items will be highlighted in the shopping cart.
Delivery to Ireland, Northern Ireland, Scottish Highlands etc may incur additional charges.
Please see our delivery information page for a full breakdown.
You are able to cancel or return the goods of items that we stock. Goods which are ordered in from suppliers specifically for your order will be subject to a restocking fee.
We are able to offer businesses trade accounts subject to a soft credit check.
Please contact us if you would like to set up a trade account.
Tracking details will be emailed for all orders sent tracked once the goods have been shipped. This will include a link to the relevant courier's website.
Alternatively, you can also contact us who can track the order for you.
Please contact us if you have any questions regarding this product or any other product or service.
You can contact us by:
- Phone: 01274 872822
- Email: sales@milotools.co.uk
- Online chat