

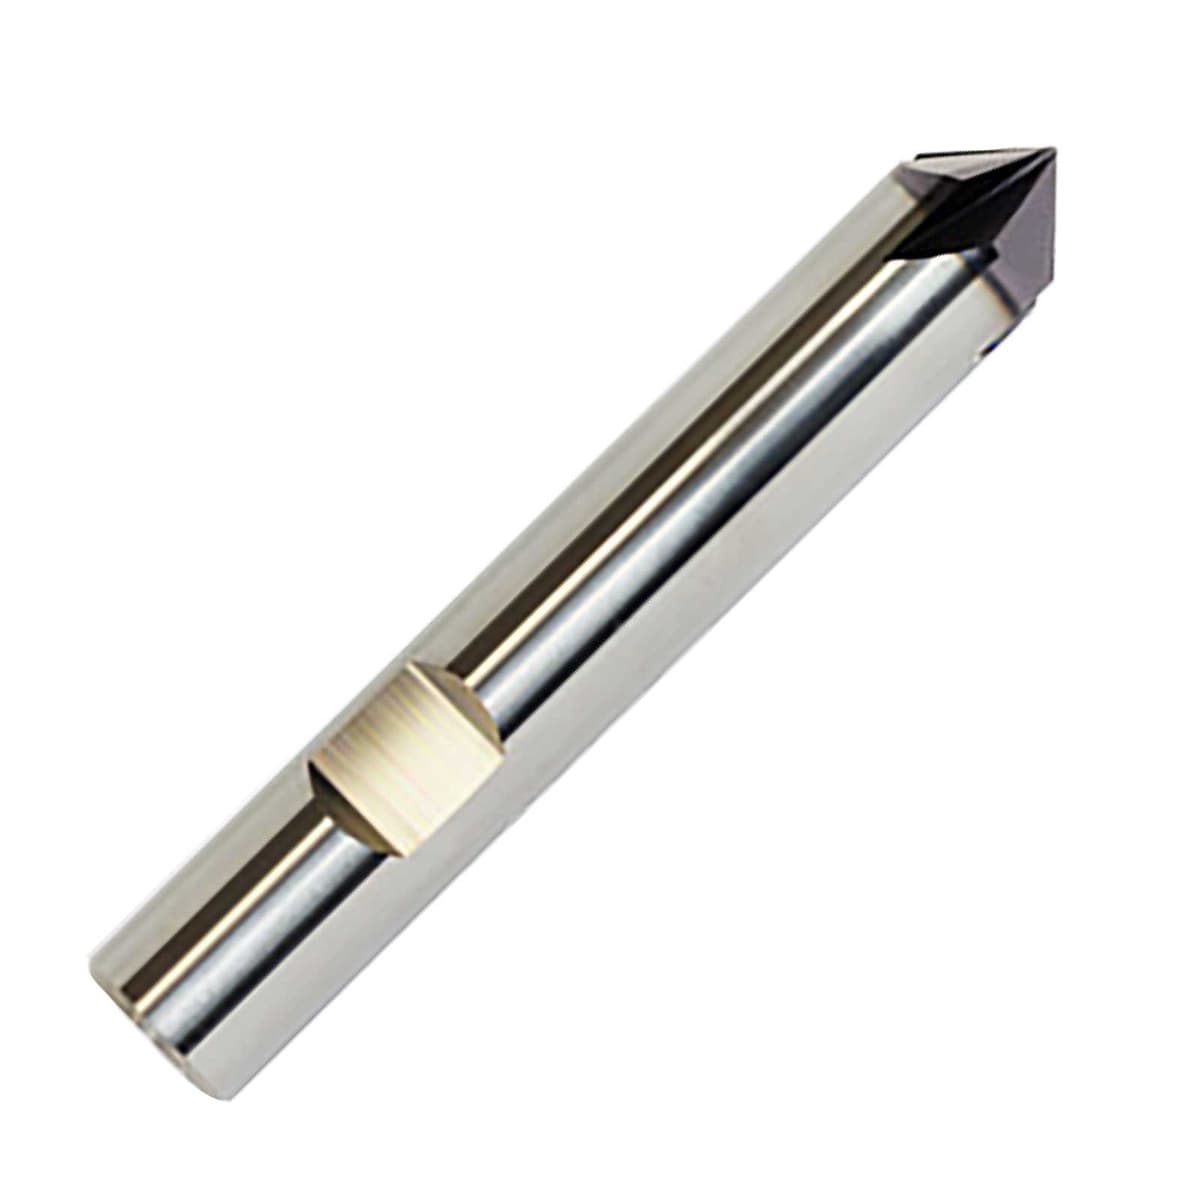


ZCC-CT 5501/5601 90 Degree Solid Carbide Deburring Cutter
Series: 5501/5601-R90£12.92 excl. VAT
£15.50 incl. VAT
Features:
- Micro grain carbide substrate.
- TiAlN Coated for longer tool life.
- Point angle: 90 degree
- Weldon shank.
For machining steels, stainless steel and cast iron.
| SKU | Diameter / D1 | Shank Diameter / D2 | Overall Length / L2 | No Flutes | Price (Ex VAT) |
|---|---|---|---|---|---|
| 5501R603FM0300KMG303 | 3mm | 3mm | 48mm | 3 | £12.92 |
| 5501R604FM0400KMG303 | 4mm | 4mm | 48mm | 4 | £13.86 |
| 5601R904FM0600KMG303 | 6mm | 6mm | 55mm | 4 | £17.30 |
| 5601R904FM0800KMG303 | 8mm | 8mm | 58mm | 4 | £25.54 |
| 5601R904FM1000KMG303 | 10mm | 10mm | 65mm | 4 | £31.44 |
| 5601R904FM1200KMG303 | 12mm | 12mm | 75mm | 4 | £43.36 |
| 5601R904FM1600KMG303 | 16mm | 16mm | 85mm | 4 | £103.60 |
Frequently Asked Questions
The Hole Making Tools section covers nine distinct product groups:
Solid Carbide Twist Drills: CNC-grade carbide drills in multiple material-specific series with sizes ranging from 0.9mm to 20mm+
HSS & HSSE Twist Drills: High-speed steel and cobalt steel drills for general workshop use
HSS & HSSE Twist Drill Sets: Boxed sets for workshop stocking
Spot Drills & Centre Drills: For accurate hole location and lathe centre work
Reamers: HSS, HSSE and solid carbide for achieving precision hole sizes and finishes
Countersinks: HSSE 90° countersinks for cap screw seating and chamfering
Indexable Drilling: Insert-based drill bodies for high-productivity large-diameter drilling
Spade Drills: Insert-based flat-blade drills for large diameters and deep holes
Hole Saws: For cutting large-diameter holes in sheet and plate
HSS (High Speed Steel)
Ground from M2 high-speed steel - the traditional workshop drill
Suitable for steel, stainless, aluminium, plastics and most general-purpose work
Lower cost per drill as it can be resharpened many times
Maximum hardness typically ~64 HRC (tool hardness) so not suitable for hardened workpieces
Best for: manual drilling, drill press work, job shop use with varied materials
HSSE / HSS-Co8 (8% Cobalt High Speed Steel)
M35 or M42 grade cobalt high-speed steel which retains hardness at higher cutting temperatures
Superior to HSS for stainless steel, titanium, nickel alloys and other difficult materials
Better heat resistance allows higher cutting speeds than standard HSS
Best for: manual and semi-CNC drilling in tough materials - a significant upgrade over HSS for stainless steel work
Solid Carbide
Ground from tungsten carbide and 3-4 times harder than HSS. Cannot flex or deflect!
Runs at 3-5 times the cutting speed of HSS in equivalent materials
Requires a rigid machine (CNC machining centre or rigid drill press with minimal runout) because carbide is brittle and will break if the drill deflects or vibrates excessively
Suitable for virtually all materials with the correct series selection
Best for: CNC machining centres with through-spindle coolant, high-volume production, difficult materials or applications where hole quality and positional accuracy are critical
General rule: for manual drilling and drill presses on standard steel, HSS or HSSE is the correct and cost-effective choice. Solid carbide in a drill press or manual machine is wasteful and risks breakage. For CNC drilling operations solid carbide is almost always the better option for productivity and hole quality.
Through-coolant (TC) drills have one or two internal helical coolant channels running from the shank to the drill tip. When used on a machine with through-spindle coolant (TSC) cutting fluid is pumped under pressure through these channels and exits as a high-pressure jet directly at the cutting zone.
Benefits of through-coolant drilling:
Chip evacuation: the coolant jet actively flushes chips out of the hole which critical in deep holes where chips would otherwise pack and cause drill breakage
Lubrication at the cutting edge: reduces built-up edge, particularly in stainless steel and titanium
Cooling at the tip: the most critical thermal zone! External flood coolant does not effectively reach the tip in holes deeper than ~2xD
Higher feed rates: with reliable chip clearance, feed per revolution can be increased significantly
Without through-spindle coolant: through-coolant drills can still be used with external flood coolant, the internal channels simply remain dry. In this case the through-coolant holes do not provide active benefit but the drill geometry and substrate are otherwise identical to non-TC versions.
Indexable drills (also called spade insert drills or insert drills) use a steel drill body (holder) with two indexable carbide inserts, one for the outer cutting zone and one for the inner zone screwed into pockets near the tip. When an insert wears it is rotated to a fresh cutting edge (indexed) or replaced. The steel body is reused indefinitely.
Key advantages over solid carbide for larger diameters:
A solid carbide drill at 20mm diameter costs many multiples of an insert drill body with two inserts & the economics flip completely above approximately 12–15mm
Inserts are replaced individually so no regrinding cost or replacement of the full drill body
Both ZCC-CT and Europa Tool are stocked
Diameter range: 12mm to 50mm in 1mm increments
Hole depth options: 2xD, 3xD, 4xD, 5xD - same depth designations as solid carbide drills
Material coverage: steel, stainless steel, cast iron, HRSA, hardened steel - all chipbreaker grades available (LM, EM, XM for medium cutting)
Through coolant: all indexable drill holders in the range support through-coolant as the body has internal coolant channels feeding the tip
What indexable drills cannot do (vs. solid carbide):
Below 12mm diameter a solid carbide is the only option as insert pockets cannot be machined into a body smaller than approximately 12mm
Hole position accuracy is typically slightly less precise than solid carbide so for close-tolerance hole positions, solid carbide stub drills are preferred
Customers Also Viewed
ex VAT
ex VAT
ex VAT
ex VAT
ex VAT
ex VAT
Service & Delivery Information
If the order is placed online, we offer free shipping to mainland UK on orders over £25 ex VAT.
This offer excludes certain items due to weight restrictions. These items will be highlighted in the shopping cart.
Delivery to Ireland, Northern Ireland, Scottish Highlands etc may incur additional charges.
Please see our delivery information page for a full breakdown.
You are able to cancel or return the goods of items that we stock. Goods which are ordered in from suppliers specifically for your order will be subject to a restocking fee.
We are able to offer businesses trade accounts subject to a soft credit check.
Please contact us if you would like to set up a trade account.
Tracking details will be emailed for all orders sent tracked once the goods have been shipped. This will include a link to the relevant courier's website.
Alternatively, you can also contact us who can track the order for you.
Please contact us if you have any questions regarding this product or any other product or service.
You can contact us by:
- Phone: 01274 872822
- Email: sales@milotools.co.uk
- Online chat