


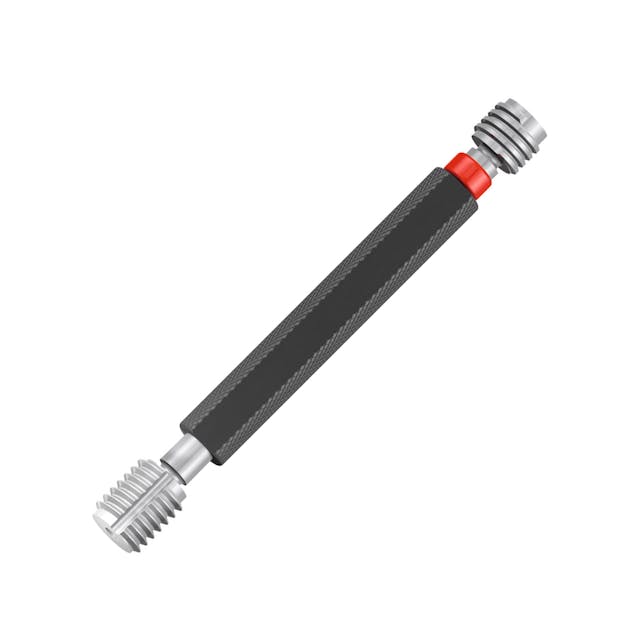
EMUGE BSP(G) Go/No-Go Thread Plug Gauge
EMUGE Unified Fine Go/No-Go Thread Plug Gauge
EMUGE Metric Coarse Go/No-Go Thread Plug Gauge
EMUGE Unified Coarse Go/No-Go Thread Plug Gauge
EMUGE Metric Coarse Go/No-Go Thread Plug Gauge
Go/No-Go thread gauges are precision inspection tools used to verify whether a threaded workpiece has been manufactured within its specified tolerance limits.
The "Go" end checks the maximum material condition, it must thread fully into or onto the workpiece to confirm the thread is not too large (on an internal thread) or too small (on an external thread).
The "No-Go" end checks the minimum material condition, it must not thread in beyond a specified number of turns, confirming the thread is not too small (internal) or too large (external).
Together, the two ends provide a pass/fail assessment of thread acceptability.
The Go end is manufactured to the maximum material limit of the thread being inspected. For an external (male) thread, the Go ring gauge should screw on smoothly and fully by hand. For an internal (female) thread, the Go plug gauge should screw in fully.
The No-Go end is manufactured to the minimum material limit, it should not enter or screw on beyond a specified number of turns (typically two) when the thread is within tolerance.
If the Go end does not engage fully, the thread is oversize; if the No-Go end enters too far, the thread is undersize.
This category includes Go/No-Go thread gauges for five thread forms:
Metric threads follow ISO standards and are the most common in UK and European engineering.
Unified threads (UNC/UNF) are used for American-standard inch-based threads.
Whitworth (G) threads are the British Standard pipe thread form used for parallel pipe connections.
Each thread form has its own pitch and diameter combinations, so it is essential to specify the correct form when ordering.
Metric Coarse (MC) threads have the standard pitch for each nominal diameter, for example, M10 x 1.5. They are the most widely used metric thread form, offering good strength, ease of assembly and resistance to stripping.
Metric Fine (MF) threads have a smaller pitch for the same diameter, for example, M10 x 1.25 or M10 x 1.0. Fine threads offer greater tensile strength, better resistance to loosening from vibration, finer adjustment capability and thinner wall thickness requirements. They are commonly used in automotive, aerospace and precision engineering applications where these properties are advantageous.
UNC (Unified National Coarse) and UNF (Unified National Fine) are inch-based thread standards used primarily in North America but widely adopted in international engineering, particularly in aerospace. UNC is the coarse-pitch series, offering fast assembly and good resistance to stripping.
UNF is the fine-pitch series, providing greater tensile stress area, better locking characteristics and finer adjustment. The gauges in this category cover standard UNC and UNF sizes from small instrument threads through to larger diameters used in structural and mechanical applications.
Whitworth G-series threads (BSPP — British Standard Pipe Parallel) are used for parallel pipe connections where a pressure-tight joint is achieved via a sealing washer, gasket or O-ring rather than the thread itself. They are commonly found in hydraulic, pneumatic and fluid-handling systems. The Go/No-Go gauges for G threads verify that the parallel thread form and pitch diameter are within tolerance, ensuring proper engagement with the mating fitting and correct alignment of the sealing surfaces.
The sense of rotation indicates whether the thread is right-hand or left-hand.
Right-hand threads tighten when turned clockwise and are the standard for the vast majority of engineering applications.
Left-hand threads tighten when turned counter-clockwise and are used in specialised applications where a right-hand thread might loosen due to rotational forces, such as on the left side of some vehicle axles, gas fittings or specific safety-critical assemblies.
All of our Go/No-Go Thread Plug Gauges are right-hand, which covers the standard thread forms and sizes stocked.
DIN 2280 is the German standard that specifies the dimensional and tolerance requirements for Go/No-Go thread limit gauges. It defines the gauge design, handling features, marking and tolerance grades for both plug gauges (internal thread inspection) and ring gauges (external thread inspection).
All gauges in this category are manufactured to DIN 2280, ensuring consistent quality, accuracy and interchangeability with other gauges produced to the same standard.
There are three dimension standards represented in our Go/No-Go category:
DIN ISO 1502: The international standard for metric (ISO) thread gauging, covering Metric Coarse and Metric Fine threads. This is the most widely used standard in European and UK engineering
DIN EN ISO 228-2: The standard for parallel pipe threads (Whitworth G-series), specifying gauge limits for BSPP thread verification
ANSI/ASME B1.2: The American standard for gauging unified (UNC/UNF) inch threads, used in North American and aerospace applications.
The correct standard is determined by the thread form being inspected as each thread form has its own governing gauging standard.
Our category covers an extensive range of nominal diameters, from as small as 1 mm up to large sizes above 33 mm.
This includes all standard Metric Coarse and Metric Fine sizes (M1 through M33+), common UNC and UNF sizes (from #0 through to 1¼ inch and above) and standard Whitworth G pipe thread sizes (from 1/16 through to 1+ inch).
Half-millimetre and intermediate diameters are also available to cover fine-pitch and specialised thread specifications.
This category includes both plug gauges (for checking internal/female threads) and ring gauges (for checking external/male threads). Plug gauges are precision-machined cylindrical threaded members that are inserted into the threaded hole or nut.
Ring gauges are internally threaded rings that are screwed onto the threaded stud or bolt. Both types feature Go and No-Go ends either as a double-ended gauge (Go on one end, No-Go on the other) or as separate single-end gauges, depending on the size and configuration.
The gauge should be applied by hand, without the use of wrenches or excessive force.
For a Go check, the Go end should thread smoothly and fully into or onto the workpiece under light finger pressure.
For a No-Go check, the No-Go end should not enter or screw on beyond the permitted number of turns (typically two full turns is the acceptance limit under most standards).
The workpiece should be clean and free of burrs, swarf or cutting fluid before gauging. If the gauge feels tight, remove it and inspect the thread rather than forcing it, as forcing a gauge can damage both the gauge and the workpiece.
Thread gauges are precision instruments and should be treated accordingly.
After use, clean the gauge with a lint-free cloth and apply a light coating of rust-preventive oil before returning it to its case. Store gauges in their dedicated cases in a dry, temperature-controlled environment away from other tools that could cause damage.
Never drop a gauge or use it as a makeshift tool. Periodically inspect gauges for signs of wear, nicks or corrosion and have them recalibrated or replaced if any damage is detected.
With proper care, quality gauges will provide many years of reliable service.
Gauges manufactured to DIN 2280 are produced to tightly controlled tolerances and are marked with their thread specification, tolerance class and gauge identification.
For applications requiring documented traceability (such as aerospace, automotive or ISO 9001 quality management systems) calibration certificates can typically be provided. I
f you require a calibration certificate or need gauges for a specific quality management system, please contact our engineering team to confirm availability and ensure your requirements are met before ordering.
Yes. Our team includes time-served engineers who can help you identify the correct thread form, pitch, tolerance class and gauge type for your inspection requirements.
Whether you need to verify a specific thread specification, interpret a drawing callout or determine which standard applies to your application, you can reach us by phone, online chat or email and we will be happy to assist.